Coal ash material pneumatic conveying systems are essential equipment in industrial processes, particularly for handling and transporting coal ash efficiently. This article will explore the working principle and key features of such systems, providing a comprehensive understanding for professionals in the field.
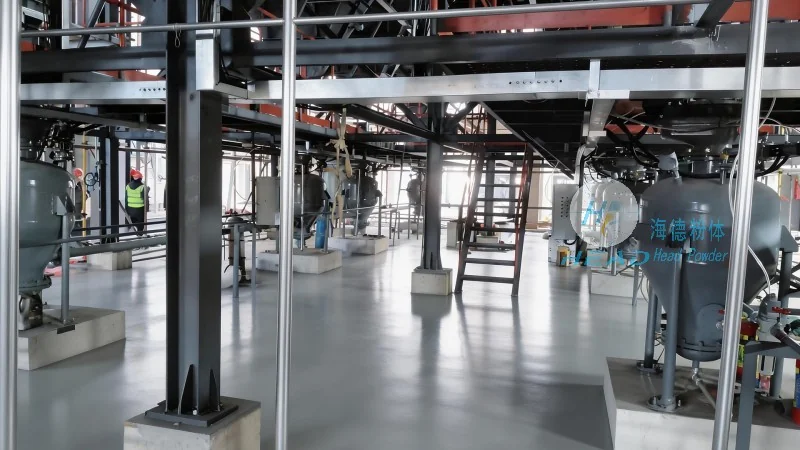
The core mechanism of a coal ash pneumatic conveying system involves the use of compressed air or gas to transport solid materials, in this case, coal ash, through a pipeline. The process typically begins with the material being fed into a hopper or feeder, where it is then introduced into the conveying line. Compressed air is then introduced at one end of the pipeline, creating a pressure differential that propels the coal ash particles forward. The system utilizes various components, including a blower, filter, and control valves, to ensure smooth and controlled transportation. The blower generates the necessary air pressure, while the filter removes any dust or particles from the air stream, maintaining system efficiency and safety. Control valves regulate the air flow and material discharge, allowing for precise control over the conveying process. This pneumatic method offers a continuous and automated way to move coal ash from the source to the destination, minimizing manual handling and associated risks.
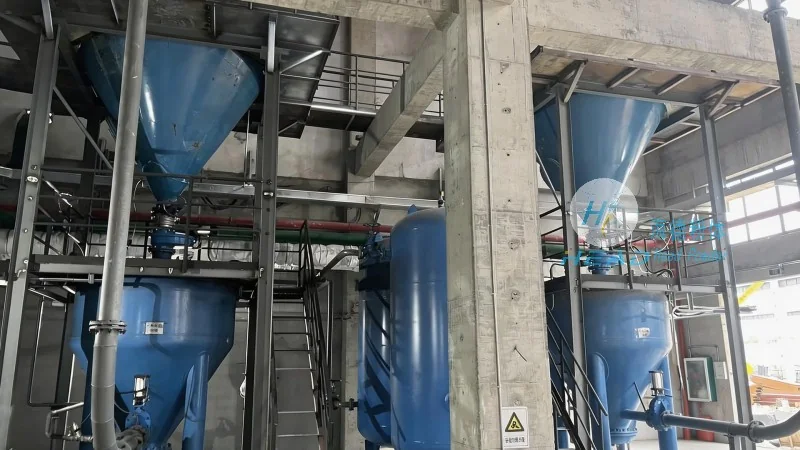
Coal ash pneumatic conveying systems offer several advantages that make them a preferred choice for industrial applications. One of the primary features is their high efficiency in material transport. By using compressed air, these systems can move large volumes of coal ash over long distances with minimal energy consumption compared to traditional methods like belt conveyors or trucks. This efficiency translates into cost savings and increased productivity for industrial operations. Another significant feature is the environmental benefits. Pneumatic conveying systems are generally more environmentally friendly as they reduce dust emissions and minimize the need for water or other cleaning agents, which are often used in other handling methods. The enclosed pipeline design also helps in controlling dust and preventing contamination, ensuring compliance with environmental regulations. Additionally, these systems provide flexibility in layout and installation. They can be easily integrated into existing industrial setups and can be adapted to various distances and heights, making them suitable for different plant configurations. The automated nature of the system also enhances safety by reducing the need for manual handling of heavy or potentially hazardous materials like coal ash. This reduces the risk of accidents and improves workplace safety standards.
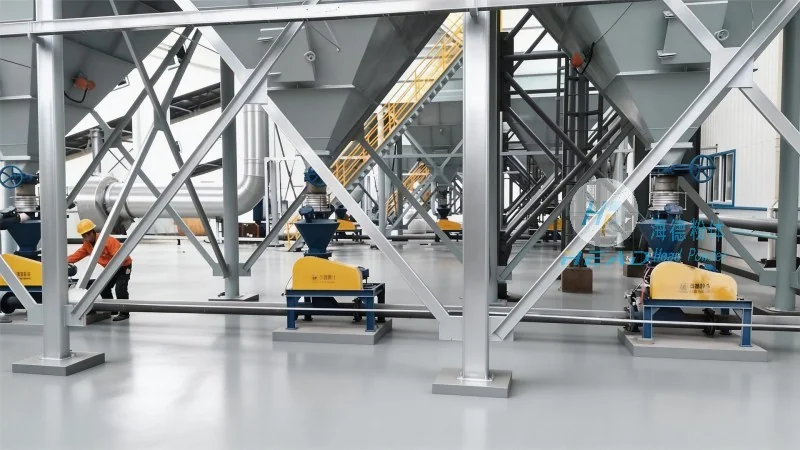
Coal ash pneumatic conveying systems are widely used in various industrial sectors, including power plants, cement factories, and waste management facilities. In power plants, for example, these systems are crucial for transporting coal ash from the boiler to storage or disposal sites. The efficiency and reliability of the system ensure that the ash is handled without interruption, maintaining the smooth operation of the power generation process. In cement factories, coal ash is often used as a supplementary cementitious material, and pneumatic conveying systems facilitate its transport from storage to the production line. This ensures a consistent supply of raw material, which is vital for maintaining production quality and output. The benefits of these systems extend beyond material transport efficiency. They also contribute to overall operational efficiency by reducing downtime caused by material handling issues. The automated control systems allow for real-time monitoring and adjustment, ensuring that the conveying process operates at optimal levels. This leads to improved productivity and reduced maintenance costs over time. Furthermore, the environmental advantages of pneumatic conveying systems align with the growing emphasis on sustainable industrial practices. By minimizing waste and emissions, these systems help industries meet regulatory requirements and enhance their corporate social responsibility.
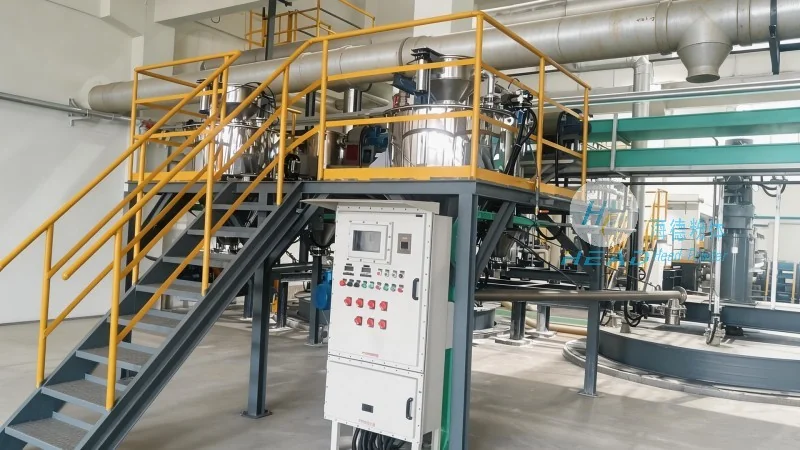
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer and supplier of industrial conveying systems, including coal ash pneumatic conveying solutions. With a strong presence in China, the company specializes in designing, manufacturing, and installing customized pneumatic conveying systems tailored to the specific needs of clients. The company's expertise lies in understanding the unique challenges of handling coal ash and other similar materials, and developing solutions that address these challenges effectively. By leveraging advanced technology and engineering expertise, headpowder provides high-quality, reliable systems that meet international standards and client expectations. The company's commitment to quality and customer satisfaction has earned it a reputation as a trusted partner in the industrial conveying industry. With a focus on innovation and continuous improvement, headpowder remains at the forefront of developing cutting-edge pneumatic conveying systems that enhance operational efficiency and environmental sustainability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top