HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of efficient pneumatic conveying systems for handling bulk materials. This article explores the fundamental working principles and key features of powder bin material pneumatic conveying lines, providing a comprehensive overview for industry professionals seeking reliable solutions for material transport.
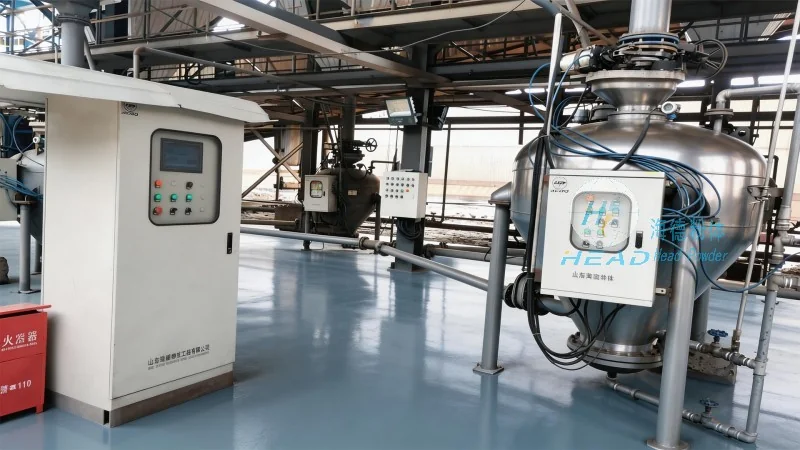
The core mechanism of a powder bin material pneumatic conveying system involves the use of compressed air to transport dry bulk materials from a storage bin to a processing or storage location. The process typically begins with the material being drawn from the powder bin by the pressure differential created by the air flow. As compressed air is introduced into the conveying line, it creates a low-pressure zone that pulls the material particles along with the air stream. The system utilizes either positive pressure (where air is blown into the line) or negative pressure (where air is drawn out), depending on the specific application and material characteristics. The air velocity within the pipeline is carefully controlled to ensure that the material is transported without causing excessive wear or degradation. The conveying line may include components such as a feeder, a filter, and a receiver, all of which work in tandem to maintain system efficiency and material integrity.
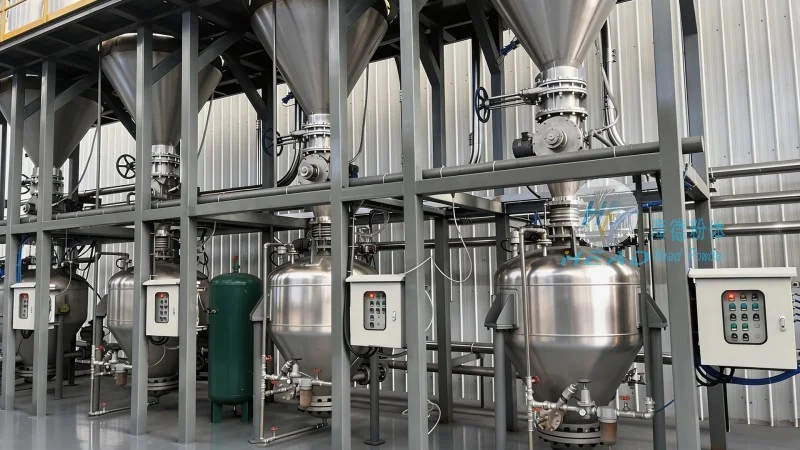
HeadPowder's pneumatic conveying systems for powder bins are distinguished by several critical features that enhance performance and reliability. Firstly, the systems are designed for high efficiency in material transport, minimizing downtime and operational costs. The use of advanced control technology allows for precise regulation of air pressure and flow, ensuring consistent material delivery. Secondly, the equipment is constructed with durable materials to withstand the abrasive nature of bulk materials, extending the service life of the system. Additionally, the systems are equipped with filtration and cleaning mechanisms to prevent material buildup and maintain air quality. Another notable feature is the modular design, which enables easy integration with existing production lines and facilitates maintenance. The systems also offer flexibility in terms of conveying distance and material types, making them suitable for a wide range of industrial applications.
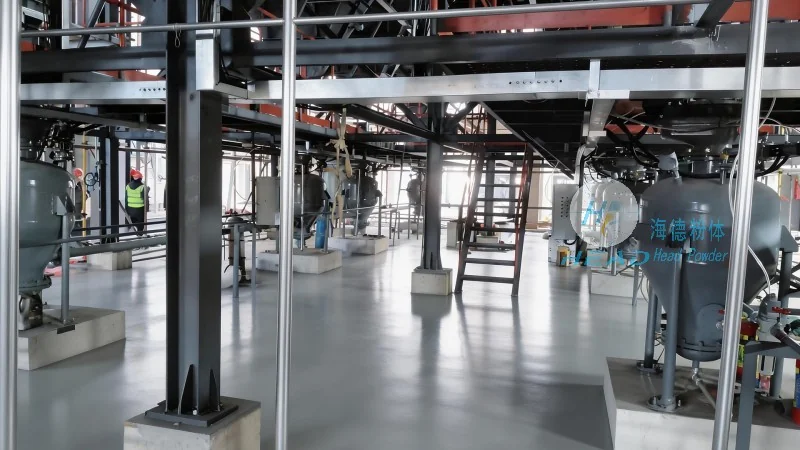
Adopting a powder bin material pneumatic conveying system from HeadPowder offers numerous advantages for industrial operations. The primary benefit is the reduction in labor costs associated with manual material handling, as the system automates the transport process. Additionally, the systems enhance safety by eliminating the need for workers to handle heavy or hazardous materials. The consistent and controlled delivery of materials improves the quality of downstream processes, such as mixing or packaging. Furthermore, the energy efficiency of pneumatic conveying systems reduces operational expenses compared to traditional methods like belt conveyors or bucket elevators. The compact design of the systems also saves valuable floor space in production facilities, making them ideal for facilities with limited space.
Powder bin material pneumatic conveying systems are widely used in various industries, including pharmaceuticals, food processing, chemical manufacturing, and mining. The systems are particularly effective for handling fine powders, granules, and other dry bulk materials that are prone to dust and clogging. For example, in the pharmaceutical industry, the systems ensure that active ingredients are transported without contamination, maintaining product purity. In the food industry, the systems comply with hygiene standards, preventing cross-contamination and ensuring food safety. The systems are also suitable for transporting materials with varying particle sizes and moisture content, as the air flow can be adjusted to accommodate different material characteristics. HeadPowder's expertise in material compatibility ensures that the systems are tailored to meet the specific needs of each application.
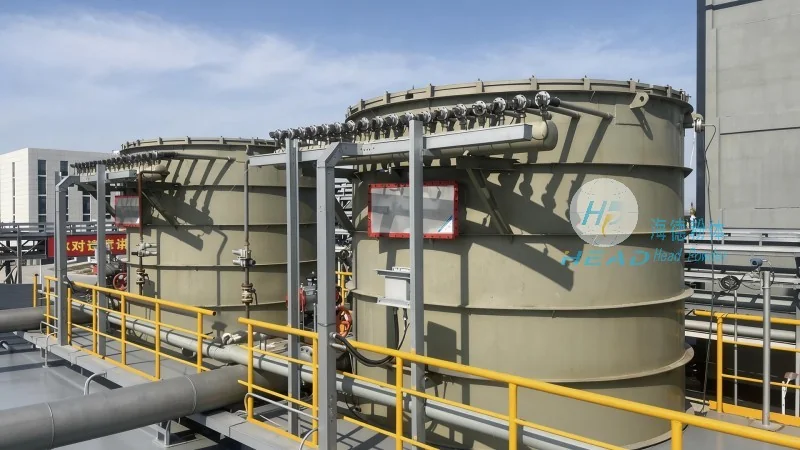
Proper maintenance is crucial to ensure the long-term performance and reliability of pneumatic conveying systems. Regular inspection of the conveying line, filters, and air compressors is essential to prevent system failures. The use of high-quality filters helps to maintain air purity and prevent material buildup in the system. Additionally, the air compressor should be maintained to ensure consistent pressure and flow. HeadPowder provides comprehensive maintenance services and technical support to assist customers in optimizing system performance. The systems are designed with user-friendly controls, allowing operators to monitor and adjust parameters as needed. Regular cleaning of the powder bin and conveying line is also recommended to prevent material accumulation and maintain system efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top