HeadPowder, a leading provider in the field of powder handling technology, specializes in the design, manufacturing, and implementation of advanced conveying systems for various industrial applications. This article delves into the operational workflow and underlying principles of a Lysine powder conveying system, highlighting the key components, control mechanisms, and efficiency measures that ensure reliable and safe material transport.
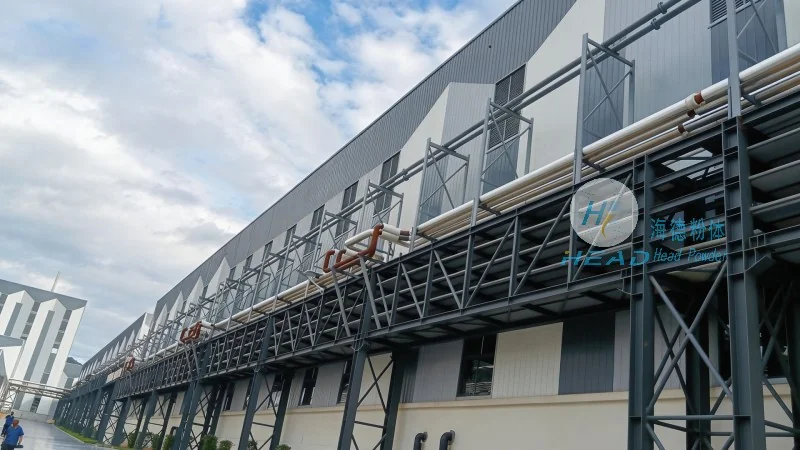
Lysine is a critical amino acid widely used in animal feed and pharmaceutical industries. The efficient and safe handling of Lysine powder is essential to maintain product quality and operational safety. A well-designed conveying system not only optimizes the flow of material but also minimizes dust generation, ensures consistent product integrity, and adheres to stringent industry standards. HeadPowder Engineering Co., Ltd., based in Shandong, China, has extensive expertise in developing customized solutions tailored to the unique requirements of Lysine powder handling processes.
The Lysine powder conveying system typically consists of several interconnected components that work in tandem to achieve seamless material transport. These components include a hopper for material storage, a feeder to control the flow rate, a conveying device (such as a screw conveyor or pneumatic system), a control panel for monitoring and adjustment, and a discharge mechanism for delivering the material to the next stage of processing. Each component is carefully selected and integrated to ensure compatibility with Lysine powder's physical properties, such as its fine particle size and hygroscopic nature.
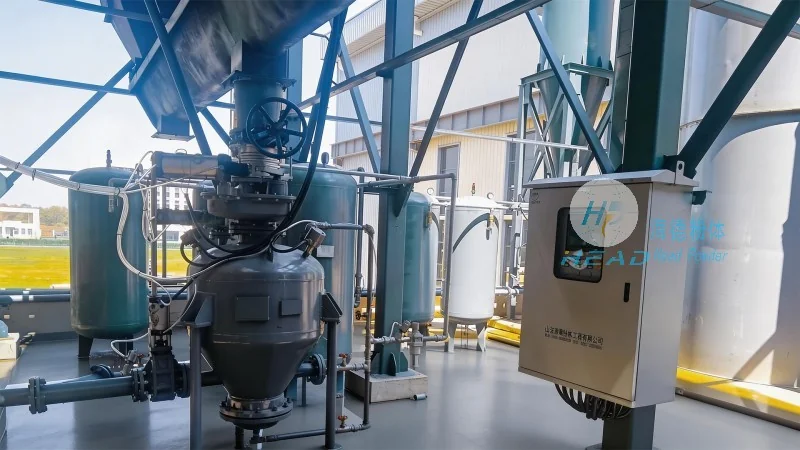
The operation of the Lysine powder conveying system begins with the loading of Lysine powder into the storage hopper. The hopper is designed with a sloped bottom to facilitate material flow and prevent clogging. A feeder, often a rotary valve or a vibratory feeder, regulates the amount of powder released into the conveying line. The feeder's speed is controlled by the system's control panel, which adjusts based on real-time demand and process parameters. The conveyed powder then travels through the conveying device, which may use mechanical force (e.g., screw rotation) or pneumatic pressure to move the material. The system is equipped with sensors and alarms to detect any blockages or abnormal conditions, ensuring immediate intervention to prevent material loss or equipment damage.
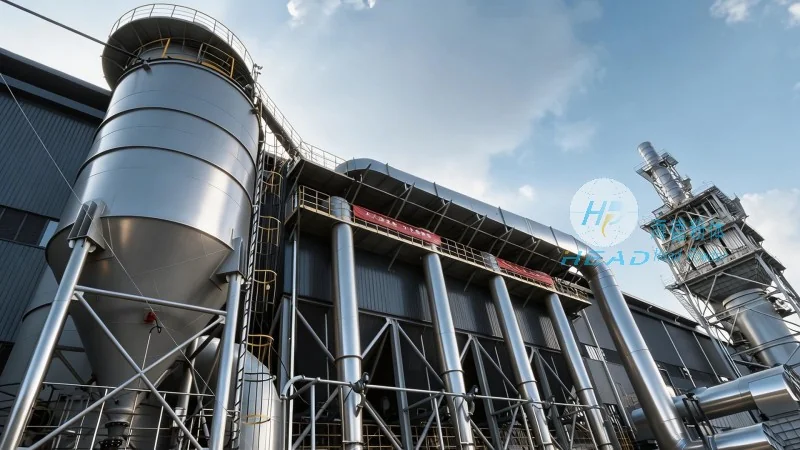
The core working principle of the Lysine powder conveying system revolves around the controlled movement of material from the source to the destination. For mechanical conveying systems, the screw conveyor operates by rotating a helical screw inside a tube, which pushes the powder forward. The speed and pitch of the screw are optimized to maintain a consistent flow rate without causing excessive pressure or particle degradation. In pneumatic conveying systems, compressed air is used to create a flow of air and powder mixture, where the powder is suspended and transported through pipes. The system's control logic ensures that the air pressure and flow rate are precisely managed to prevent dust accumulation and maintain material integrity. Additionally, the system incorporates dust collection and filtration systems to comply with environmental regulations and maintain a clean working environment.
Advanced control systems are integral to the efficient operation of the Lysine powder conveying system. The control panel, typically equipped with a human-machine interface (HMI), allows operators to monitor key parameters such as flow rate, pressure, and temperature in real time. Sensors, including level detectors, pressure transducers, and flow meters, provide continuous feedback to the control system, enabling automatic adjustments to maintain optimal performance. The system may also include programmable logic controllers (PLCs) that execute pre-set sequences for start-up, shutdown, and emergency stop procedures. This automation ensures consistent operation, reduces human error, and enhances overall system reliability.
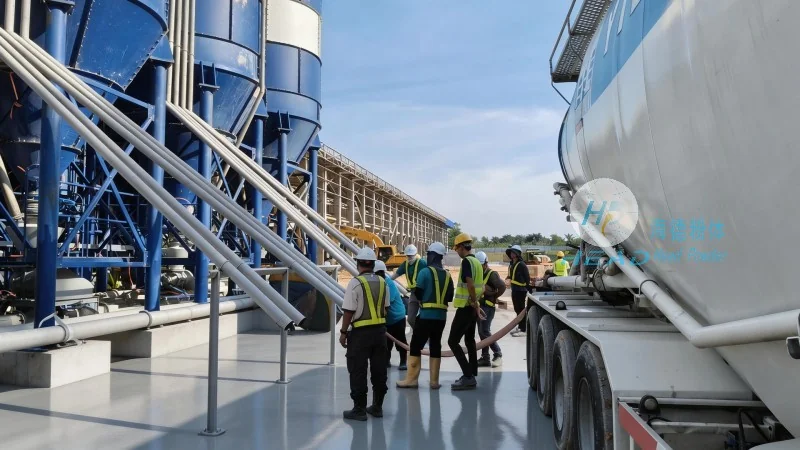
Given the nature of Lysine powder, which can be hygroscopic and potentially cause dust explosions under certain conditions, safety is a paramount concern in the design and operation of the conveying system. The system incorporates various safety features, including explosion-proof components, dust suppression systems, and emergency shutdown mechanisms. Regular maintenance is essential to ensure the longevity and performance of the equipment. This includes cleaning of hoppers and conveying lines to prevent material buildup, lubrication of moving parts, and inspection of sensors and control systems. HeadPowder Engineering Co., Ltd. provides comprehensive maintenance services and technical support to ensure that the system operates at peak efficiency and meets all regulatory requirements.
The Lysine powder conveying system developed by HeadPowder Engineering Co., Ltd. exemplifies the integration of advanced technology and industrial expertise in powder handling. By understanding the operating process and working principles of such systems, users can optimize their material transport operations, enhance product quality, and ensure compliance with industry standards. With its headquarters in Shandong, China, HeadPowder continues to innovate and provide tailored solutions that meet the evolving needs of the Lysine powder industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top