HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems for various powder materials, including poultry powders. This article provides a detailed overview of the structure and operational principles of such equipment, highlighting its key components and how they work together to ensure efficient and reliable powder transportation.
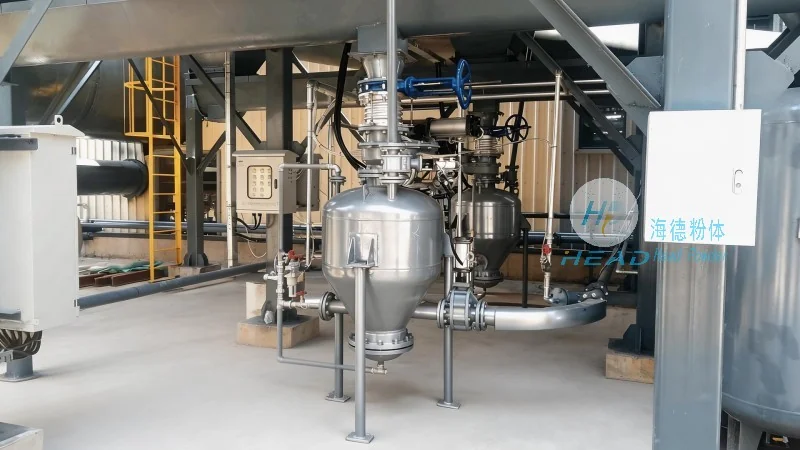
Pneumatic conveying equipment is a critical technology in the food processing industry, particularly for handling fine powders like poultry powders. These systems use compressed air or other gases to transport bulk materials through a closed pipeline system. The primary advantage of pneumatic conveying is its ability to handle delicate, hygienic, and potentially dusty powders without the need for mechanical components that could cause contamination or product degradation.
The pneumatic conveying system for poultry powders typically consists of several interconnected components, each playing a vital role in the overall operation. The main components include the feed hopper, the air compressor or blower, the conveying pipeline, the gas-solid separator, and the product collection tank. Each component is designed to work in harmony to ensure efficient material transfer while maintaining product quality and system reliability.
The feed hopper is the initial component where the poultry powder is stored and prepared for transport. It is usually equipped with a rotary valve or a star feeder to control the flow rate of the material into the conveying line. The hopper is designed to be hygienic and easy to clean, ensuring compliance with food safety regulations. The material preparation stage also involves ensuring that the powder is free from clumps or oversized particles, as these can affect the efficiency of the conveying process.
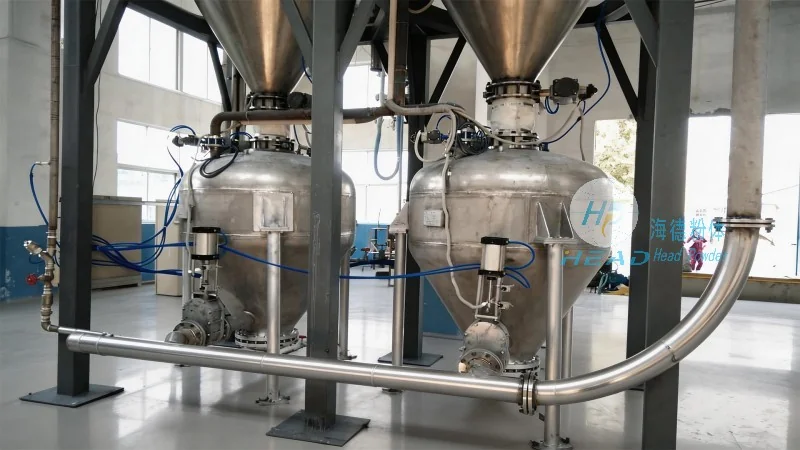
The air compressor or blower is the heart of the pneumatic conveying system, responsible for generating the necessary pressure and airflow to move the powder through the pipeline. There are two main types of air movers used in such systems: positive displacement blowers and centrifugal compressors. Positive displacement blowers, such as rotary lobe or roots blowers, are commonly used for low to medium pressure applications, while centrifugal compressors are suitable for high-pressure systems. The choice of air mover depends on the specific requirements of the application, including the material's characteristics, the conveying distance, and the desired flow rate.
The conveying pipeline is a closed system made of materials like stainless steel or food-grade plastic, designed to withstand the pressure and temperature of the conveying process. The pipeline is typically arranged in a loop or a straight line, depending on the layout of the facility. The flow path includes various components such as elbows, tees, and straight sections, which are strategically placed to guide the powder and air mixture through the system. The design of the pipeline is crucial to minimize pressure losses and ensure consistent material flow.
The gas-solid separator is the final component of the pneumatic conveying system, responsible for separating the powder from the air and collecting the product in a clean and hygienic manner. The separator typically consists of a cyclone or a bag filter, which uses centrifugal force or filtration to separate the powder from the air stream. The separated powder is then collected in a product tank or a silo, while the clean air is discharged back into the system or vented to the atmosphere. The design of the separator is critical to ensure high efficiency in powder recovery and to maintain air quality in the facility.
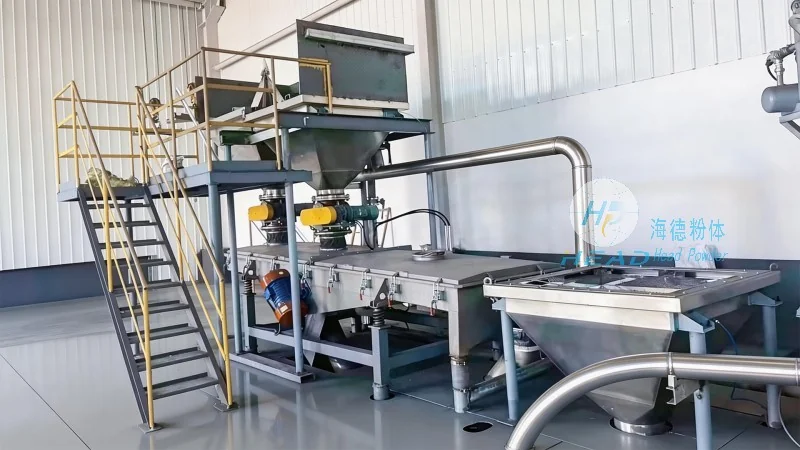
The operational principle of a pneumatic conveying system is based on the interaction between the air and the powder particles. The compressed air creates a pressure differential that lifts the powder particles and carries them through the pipeline. The flow rate and pressure are carefully controlled to ensure that the powder particles are suspended in the air stream without settling or clogging the pipeline. Several factors affect the efficiency of the system, including the particle size and density of the powder, the air velocity, the conveying distance, and the system design. Proper maintenance and regular cleaning of the components are also essential to maintain the system's performance and prevent downtime.
Pneumatic conveying equipment is widely used in the poultry powder processing industry for various applications, such as transporting raw materials, moving finished products, and handling waste materials. The benefits of using pneumatic conveying systems include improved product quality, reduced contamination risk, increased operational efficiency, and lower labor costs. Additionally, these systems are easy to integrate into existing production lines and can be customized to meet the specific needs of different applications.
HeadPowder Engineering Co., Ltd. provides high-quality pneumatic conveying equipment designed to meet the demanding requirements of the poultry powder industry. By understanding the structure and operational principles of these systems, users can make informed decisions about the most suitable equipment for their applications. The company's commitment to quality and innovation ensures that its products are reliable, efficient, and compliant with industry standards, helping customers achieve their production goals while maintaining product integrity and safety.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top