HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced paddy grain pneumatic conveying systems. These systems are engineered to efficiently transport paddy grains from storage areas to processing facilities, ensuring minimal loss and optimal grain quality. The following sections detail the operational process and underlying principles of such equipment, highlighting the key components and their functions.
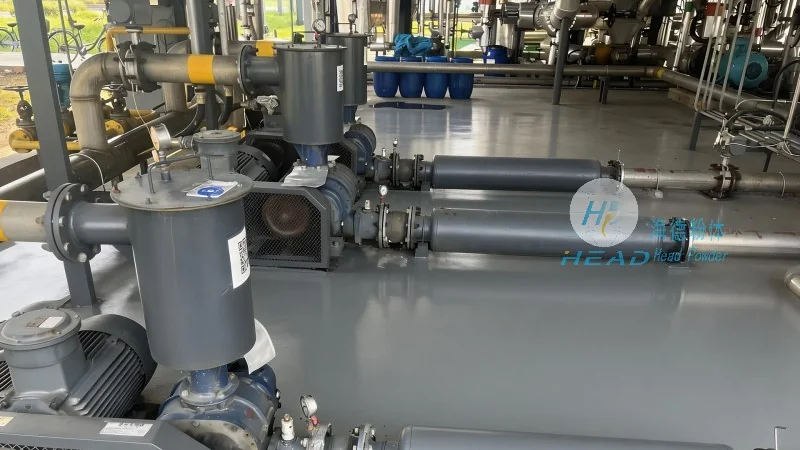
The paddy grain pneumatic conveying system typically consists of several critical components that work in tandem to achieve efficient material transport. The primary components include the hopper, air compressor, conveying pipeline, rotary valve, and dust collector. Each component plays a vital role in the overall system performance.
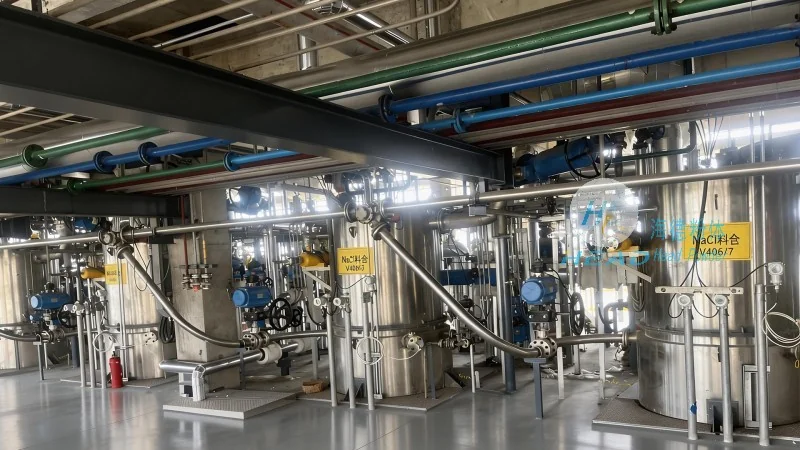
The hopper is the initial storage and feeding unit where paddy grains are loaded. It is designed with a sloped bottom to facilitate smooth material flow into the conveying pipeline. The air compressor, often a positive displacement type, generates the necessary air pressure to move the grains through the system. The conveying pipeline, usually made of stainless steel or other corrosion-resistant materials, ensures the grains are transported under controlled air pressure. The rotary valve acts as a control valve at the discharge end, regulating the flow of grains out of the system. Finally, the dust collector is integrated to capture and filter any airborne particles, maintaining a clean and safe working environment.
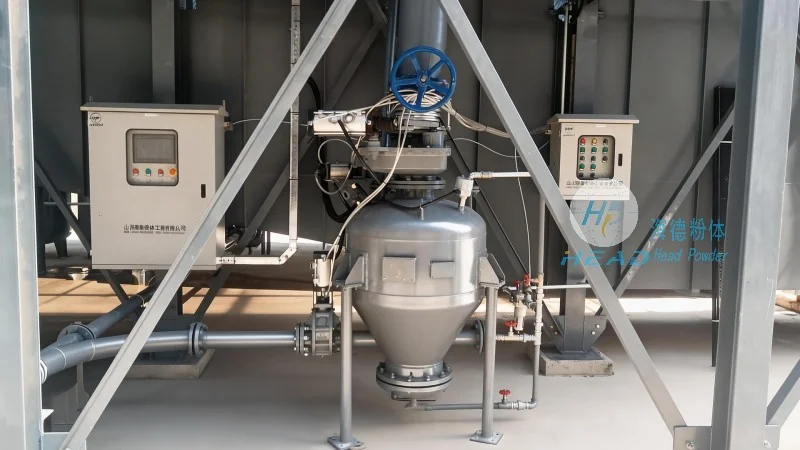
The operation of the paddy grain pneumatic conveying system is based on the principle of pneumatic transport, where grains are suspended and carried by a stream of air. The process begins with the grains being fed from the hopper into the conveying pipeline. The air compressor then supplies compressed air, which creates a pressure differential within the pipeline. This pressure differential propels the grains forward through the pipeline. As the grains move, they are kept in suspension by the air flow, reducing friction and minimizing grain damage. The system maintains a consistent air pressure and flow rate to ensure reliable and continuous transport of paddy grains.
The operational process of the paddy grain pneumatic conveying system involves several sequential steps. First, the paddy grains are loaded into the hopper. The rotary valve at the inlet of the hopper controls the flow rate of grains into the conveying pipeline. Simultaneously, the air compressor starts and generates compressed air. The compressed air is introduced into the pipeline, creating a positive pressure that moves the grains forward. The grains travel through the pipeline, passing through any necessary processing units such as cleaning or sorting equipment. At the discharge end, the rotary valve regulates the release of grains into the receiving container. The dust collector continuously operates to capture any airborne dust or particles, ensuring compliance with environmental standards and maintaining worker safety.
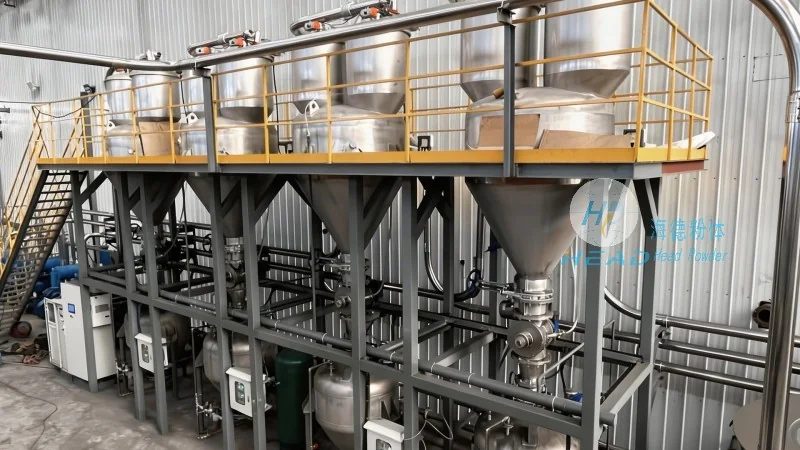
Implementing a paddy grain pneumatic conveying system offers several advantages over traditional mechanical conveying methods. Firstly, it reduces the risk of grain breakage and damage, which is crucial for maintaining grain quality. The system’s enclosed design minimizes exposure to contaminants and moisture, preserving the integrity of the paddy grains. Additionally, the pneumatic transport method is highly efficient, allowing for continuous and automated operation, which improves productivity and reduces labor costs. The system also provides better control over the flow rate and pressure, enabling precise management of grain movement. Furthermore, the enclosed pipeline reduces dust emissions, contributing to a cleaner and safer working environment.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top