HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced air-pneumatic conveying systems tailored for handling moisture-containing sodium nitrate. This article explores the fundamental principles behind such equipment, its operational characteristics, and the specific scenarios where it excels in material transport. By understanding these aspects, industries dealing with sodium nitrate can optimize their material handling processes, ensuring efficiency, safety, and reliability.
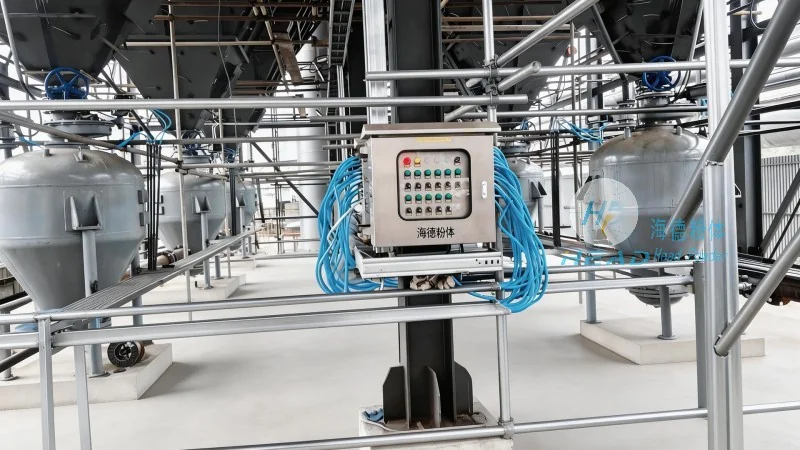
The core principle of air-pneumatic conveying involves the use of compressed air to transport bulk materials through a pipeline system. In the case of moisture-containing sodium nitrate, the equipment must be engineered to handle the unique challenges posed by the material's hygroscopic nature and potential for dust generation. The system typically consists of a hopper, a rotary valve, a conveying line, and a receiver. Compressed air is introduced into the conveying line, creating a low-pressure zone that draws the sodium nitrate particles into the flow. The velocity of the air ensures that the particles remain suspended and are transported to the destination. Key components like the air lock and the filter system are critical for maintaining material integrity and preventing air leakage, which is essential for both efficiency and safety. The system operates on the principle of creating a vacuum or pressure differential that moves the material along the pipeline, with the air flow rate being carefully controlled to match the material's flow characteristics. This control is vital to prevent material degradation and ensure consistent transport.
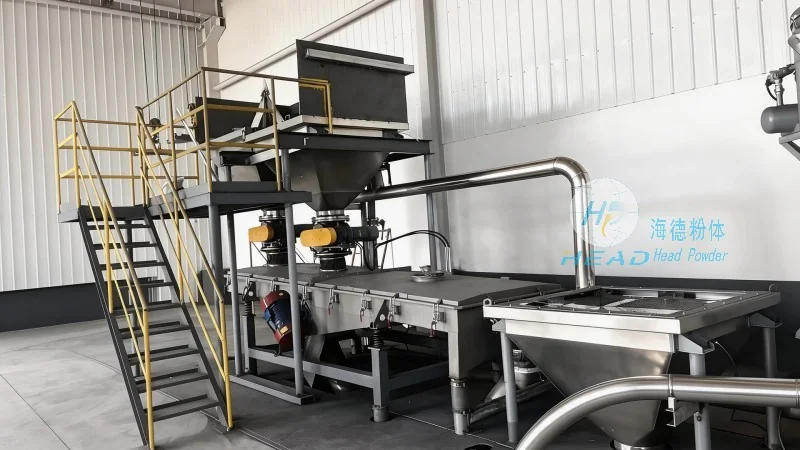
The air-pneumatic conveying equipment for moisture-containing sodium nitrate is particularly suited for industrial environments where precise and dust-free material handling is required. Common applications include chemical plants, fertilizer production facilities, and food processing industries. In these settings, the equipment operates in scenarios such as:
When compared to traditional methods like belt conveyors or bucket elevators, air-pneumatic conveying offers several advantages for moisture-containing sodium nitrate. Firstly, it eliminates the risk of material degradation due to contact with metal surfaces or excessive friction. The enclosed system prevents exposure to ambient air, reducing the risk of caking or clumping. Secondly, the system is highly flexible, allowing for vertical and horizontal transport in a single line, which simplifies the layout of industrial facilities. This flexibility is particularly beneficial in retrofitting existing plants or designing new facilities where space is limited. Additionally, the equipment is less prone to blockages and can handle materials with a wide range of particle sizes, making it suitable for various processing needs. The ability to transport fine powders without segregation is another key advantage, as it maintains the material's uniformity throughout the process.
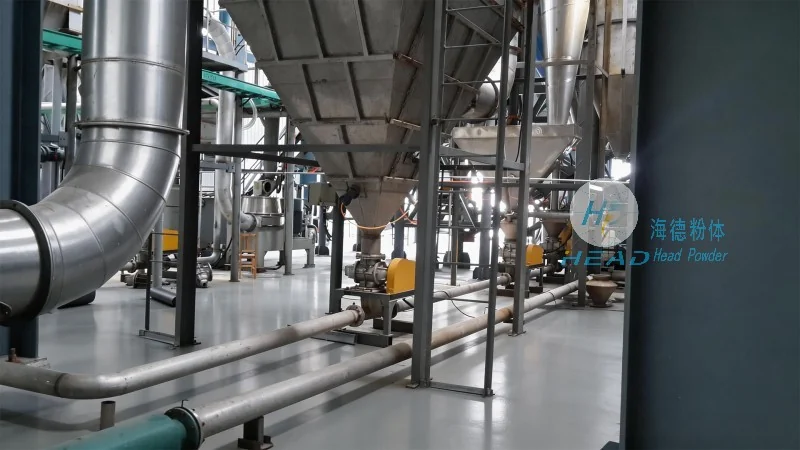
Operating air-pneumatic conveying systems for sodium nitrate requires careful consideration of several factors to ensure optimal performance and safety. Temperature control is a critical aspect, as high temperatures can affect the material's properties and the system's performance. The system must be equipped with temperature sensors and appropriate cooling mechanisms if necessary. For example, in hot climates or during high-temperature processing, the conveying line may need to be insulated to prevent heat transfer that could alter the sodium nitrate's moisture content. Additionally, the equipment must be designed to handle the material's hygroscopic nature, which means regular maintenance of the air filter and moisture traps is essential to prevent clogging. The air filter, typically made of high-efficiency particulate air (HEPA) or similar materials, removes dust and moisture from the air, ensuring that the material remains dry and free-flowing. Safety features such as pressure relief valves and emergency shut-off systems are standard to protect against over-pressurization and other hazards. These features are critical in preventing accidents and ensuring the safety of personnel working in the vicinity of the equipment. Regular inspection and maintenance of these safety components are recommended to maintain compliance with industrial safety standards.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top