Wheat flour bulk material handling is a critical process in the food processing industry, focusing on the efficient and safe transportation of wheat flour from storage facilities to production lines or packaging areas. This process involves various equipment and systems designed to handle the unique properties of wheat flour, such as its fine particle size, low bulk density, and tendency to create dust. The design of wheat flour bulk material handling systems must consider multiple factors, including material characteristics, operational requirements, and safety standards, to ensure optimal performance and minimal product loss.
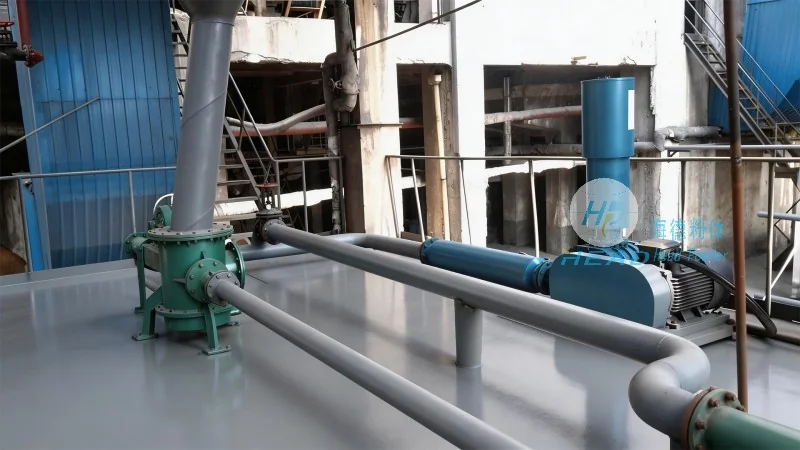
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and integration of advanced wheat flour bulk material handling systems. With years of experience in the industry, HeadPowder has developed a comprehensive approach to addressing the challenges of wheat flour transportation, combining technical expertise with practical solutions tailored to client needs. The company’s headquarters is located in Shandong, China, where it leverages local resources and industry knowledge to deliver high-quality, reliable equipment for the global food processing market.
Wheat flour bulk material handling systems are designed to move large quantities of wheat flour in a continuous or intermittent manner. The core components of such systems typically include storage silos, conveyors (like screw conveyors, belt conveyors, or pneumatic conveyors), transfer points, and control systems. Each component plays a crucial role in the overall efficiency of the process. For example, storage silos are used to hold large volumes of wheat flour, while conveyors transport the material to the next stage of processing. Transfer points ensure smooth transitions between different equipment, minimizing material spillage and maintaining product integrity.
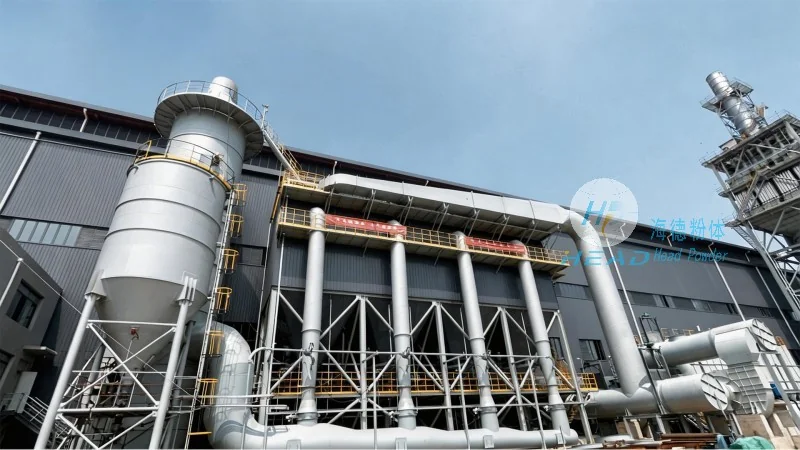
The design of wheat flour bulk material handling systems is guided by several fundamental principles that ensure safety, efficiency, and product quality. First, the system must be designed to handle the specific physical properties of wheat flour, including its particle size distribution, moisture content, and flow characteristics. Wheat flour is a fine powder with a relatively low bulk density, which can lead to issues like bridging (where material forms a solid plug in the hopper) or segregation (where different particle sizes separate during transport). To address these issues, designers often incorporate features such as agitators, vibrators, or air knives into the system to maintain consistent flow.
Second, energy efficiency is a critical design consideration. Wheat flour bulk material handling systems often operate continuously, and minimizing energy consumption reduces operational costs and environmental impact. This is achieved through the selection of appropriate conveyor types, such as screw conveyors, which are energy-efficient for short to medium distances, or pneumatic conveyors, which can be optimized for long-distance transport with lower energy use compared to traditional belt conveyors. Additionally, the system layout is designed to minimize the number of transfer points and the length of conveyor runs, reducing friction and energy loss.
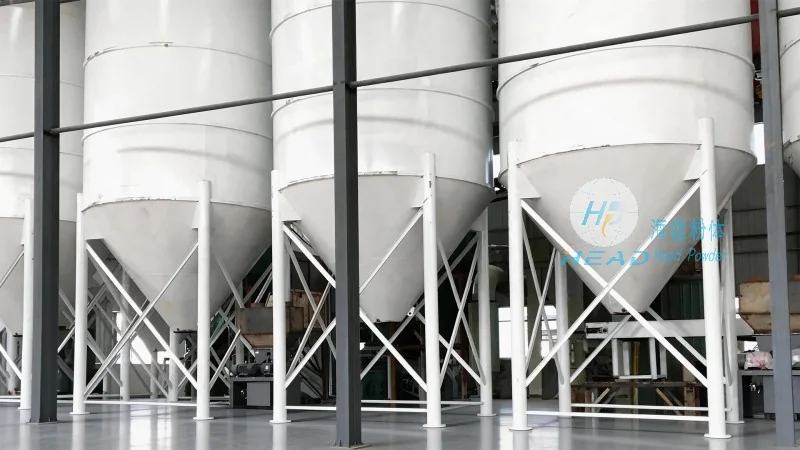
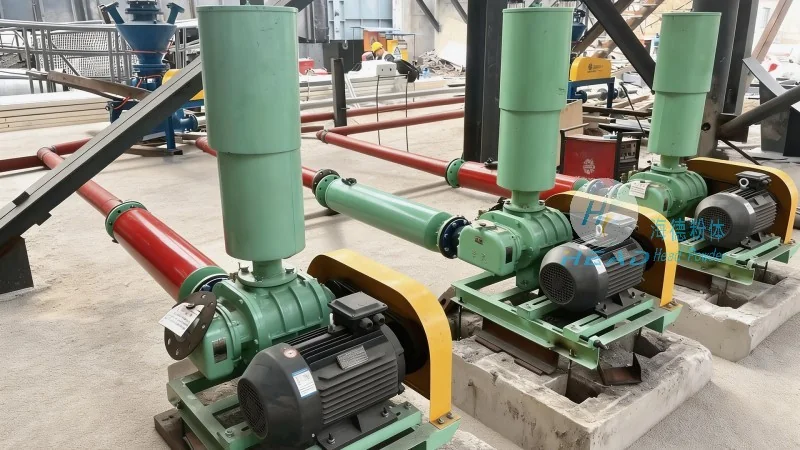
Choosing the right equipment for a wheat flour bulk material handling system is a key decision that impacts performance and cost. The primary equipment types used in such systems include:
When selecting equipment, designers consider factors such as the required capacity (in tons per hour), the distance between the source and destination, the available space, and the budget. The system is then integrated with control systems that monitor and regulate the flow of wheat flour, ensuring consistent performance and preventing overloading or underloading of the equipment.
Wheat flour bulk material handling systems must adhere to strict safety and hygiene standards to prevent contamination and ensure the quality of the final product. Key safety features include dust suppression systems, which use water or other agents to control dust emissions, and explosion-proof designs, which are essential in environments where dust can accumulate and pose a fire risk. Additionally, the equipment is designed to be easy to clean and maintain, with smooth surfaces and no crevices where flour can accumulate and become a breeding ground for bacteria.
Product integrity is also a top priority. The system is designed to minimize product degradation, such as oxidation or moisture absorption, which can affect the quality of the wheat flour. This is achieved through the use of airtight containers, temperature-controlled environments, and minimal exposure to air during transport. The design also considers the potential for cross-contamination, ensuring that different types of wheat flour or other materials are not mixed during the handling process.
Wheat flour bulk material handling is a complex process that requires careful consideration of material properties, operational requirements, and safety standards. HeadPowder, with its expertise and experience, provides comprehensive solutions that address these challenges effectively. By leveraging advanced design principles and high-quality equipment, HeadPowder ensures that wheat flour is transported efficiently, safely, and with minimal loss, meeting the needs of food processing facilities worldwide. Whether for small-scale or large-scale operations, HeadPowder's systems are tailored to deliver reliable performance and enhance productivity in the wheat flour handling process.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top