Efficient and reliable dust material conveying systems are essential in modern industrial operations, particularly for handling bulk materials that are fine, powdery, or have a tendency to generate dust during transport. The principles behind these systems are designed to address the unique challenges posed by such materials, ensuring safe, efficient, and cost-effective material movement from one point to another. This article explores the fundamental principles of dust material conveying lines and highlights the key characteristics of their working scenarios, with a focus on the expertise of Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in this field.
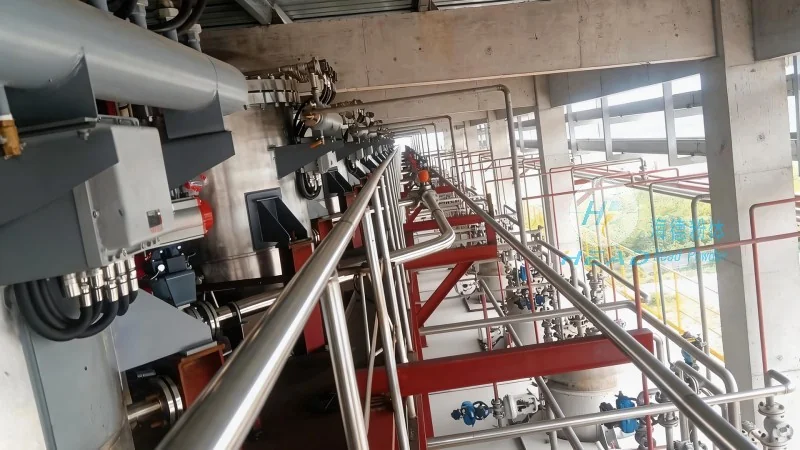
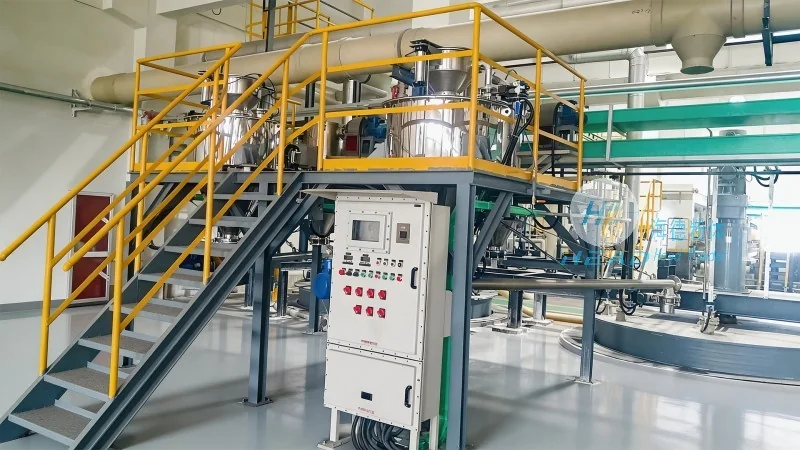
The primary principle of dust material conveying lines is to transport particulate materials, such as powders, granules, or fine particles, through a closed or semi-closed system. Unlike traditional open systems, these conveyors minimize dust dispersion, enhancing workplace safety and environmental compliance. The key components typically include a feeding mechanism, a conveying medium (like air or mechanical components), and a discharge system. The selection of the appropriate conveying method—such as pneumatic conveying, mechanical conveying, or a combination of both—depends on factors like material properties, particle size, moisture content, and the required transport distance. For example, pneumatic conveying systems use air pressure to move materials through pipes, while mechanical systems rely on belts, screws, or buckets to transport materials along a fixed path. The design of the system must also consider the material's flow characteristics, ensuring that it can be conveyed without clogging or degradation. Additionally, the system is equipped with dust collection and filtration components to capture and remove airborne particles, further improving safety and environmental performance.
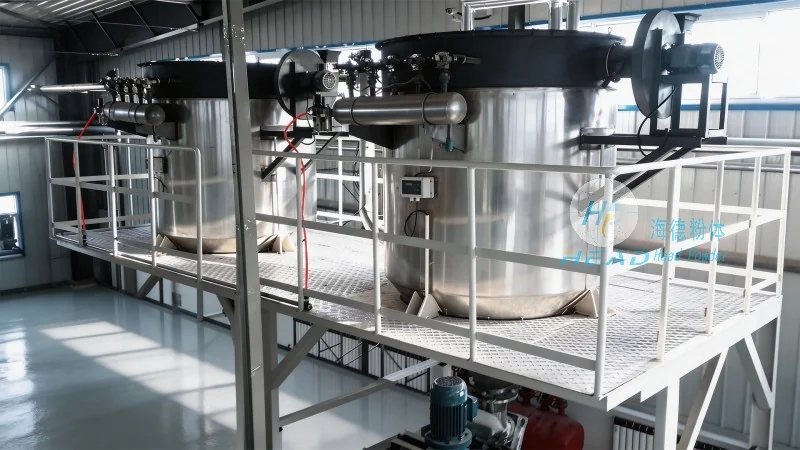
The working scenarios of dust material conveying lines vary widely across different industries, each with specific requirements that influence the system's design and operation. In the chemical industry, for instance, these systems are used to transport raw materials like powders or granules to reactors or storage tanks, where precise control over material flow is critical. The systems must be capable of handling materials with varying moisture levels and chemical properties, often requiring specialized materials for the conveyor components to prevent corrosion or contamination. In the food and pharmaceutical industries, the emphasis is on hygiene and contamination control. Dust material conveying lines here are designed with stainless steel components, sealed systems, and advanced filtration to meet stringent regulatory standards. The working environment is typically clean and controlled, with strict protocols for material handling to avoid cross-contamination. In the mining and mineral processing sector, these systems are used to transport raw ores, crushed materials, or fine powders from processing plants to storage or further processing facilities. The systems must be robust enough to handle abrasive materials and high volumes, often operating under harsh conditions with high temperatures or dust exposure. The working scene may involve large-scale operations with multiple conveying lines integrated into a complex production process, requiring efficient coordination and monitoring. In the construction and cement industry, dust material conveying lines are used to transport raw materials like limestone, clay, or cement powders to production lines or storage silos. The systems must be able to handle high volumes of material and operate continuously to meet production demands. The working environment may involve dust generation, requiring effective dust suppression and collection measures to maintain a safe working atmosphere. Overall, the working scene characteristics of dust material conveying lines are shaped by the specific needs of each industry, emphasizing efficiency, safety, and compliance with operational and environmental standards.
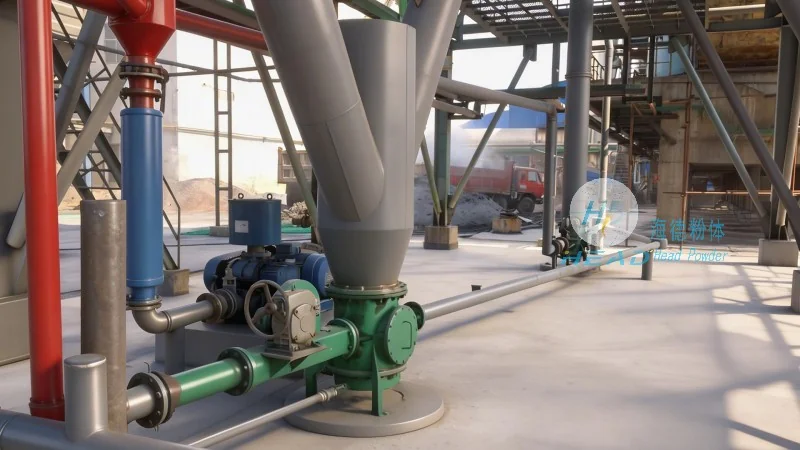
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a reputable manufacturer specializing in the design, development, and production of dust material conveying systems. With its headquarters located in Shandong, China, the company has established itself as a trusted partner for industries requiring reliable and efficient material handling solutions. HeadPowder's expertise lies in tailoring conveying systems to meet the unique demands of various applications, ensuring that clients receive customized solutions that enhance productivity and safety. The company's product range includes a variety of dust material conveying lines, such as pneumatic conveying systems, screw conveyors, and bucket elevators, each designed to handle different types of materials and operational conditions. The company adheres to strict quality control standards, using advanced manufacturing techniques and materials to ensure durability and performance. HeadPowder also provides comprehensive after-sales support, including installation, maintenance, and technical assistance, to ensure that clients can maximize the lifespan and efficiency of their conveying systems. By combining technical expertise with customer-centric service, Shandong HeadPowder Engineering Co., Ltd. continues to deliver high-quality dust material conveying solutions that meet the evolving needs of modern industries.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top