Sand and gravel material conveying lines are critical components in the construction and mining industries, designed to efficiently transport bulk materials such as sand, gravel, and crushed stone over long distances. These systems play a pivotal role in optimizing material handling processes, reducing operational costs, and enhancing overall productivity in various industrial applications. The principles underlying these conveying systems revolve around mechanical energy conversion, material flow control, and system integration to ensure reliable and continuous operation.
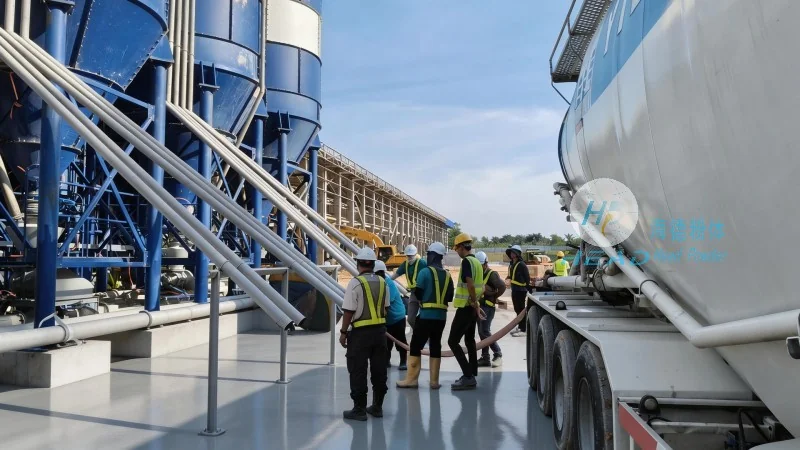
The fundamental principles of sand and gravel material conveying lines are centered on the efficient transfer of bulk materials using mechanical means. Key components include conveyor belts, rollers, idlers, and drive systems that work in tandem to move materials from the source to the destination. The design of these systems is tailored to handle the specific characteristics of sand and gravel, such as particle size, density, and abrasiveness, ensuring minimal wear and tear on equipment. Energy efficiency is a critical consideration, as these systems often operate continuously for extended periods, making the selection of appropriate drive mechanisms and material handling technologies essential for cost-effective operation.
Sand and gravel material conveying lines are deployed in diverse working environments, each with unique operational requirements. In construction sites, these systems are commonly used to transport raw materials to concrete mixing plants or to move finished aggregates to storage areas. The working scene characteristics include high throughput demands, variable material compositions, and the need for robust equipment capable of withstanding harsh conditions like dust, moisture, and temperature fluctuations. Mining operations also rely heavily on these conveying lines to transport extracted sand and gravel from open-pit or underground mines to processing facilities or loading docks. The working environment in mining sites often involves heavy machinery, limited space, and the need for systems that can operate in challenging terrains, such as steep inclines or uneven ground.
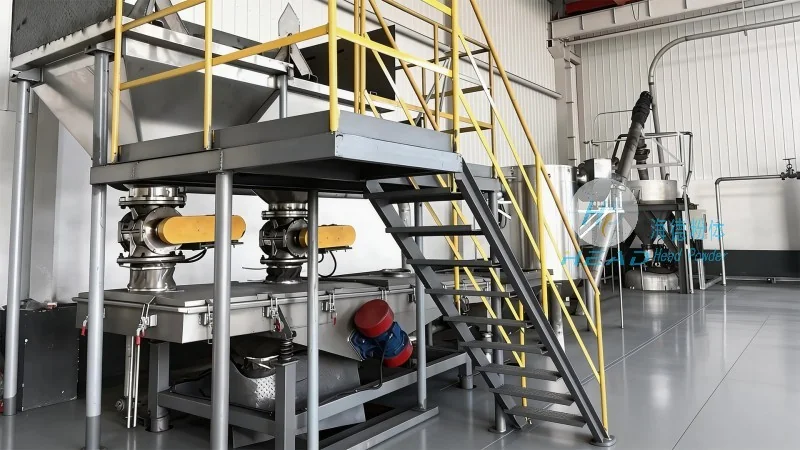
The application scenarios of sand and gravel material conveying lines span across multiple industries, including construction, mining, and aggregate processing. In construction, these systems are integral to the supply chain, enabling seamless material flow from quarries to building sites. The operational advantages include reduced labor costs, minimized material loss during transport, and improved safety by eliminating manual handling of heavy loads. Mining operations benefit from the ability to transport large volumes of material over long distances without the need for additional trucks or heavy machinery, thereby increasing overall efficiency and reducing environmental impact. Aggregate processing plants utilize these conveying lines to move materials between different processing stages, such as crushing, screening, and storage, ensuring a continuous production cycle.
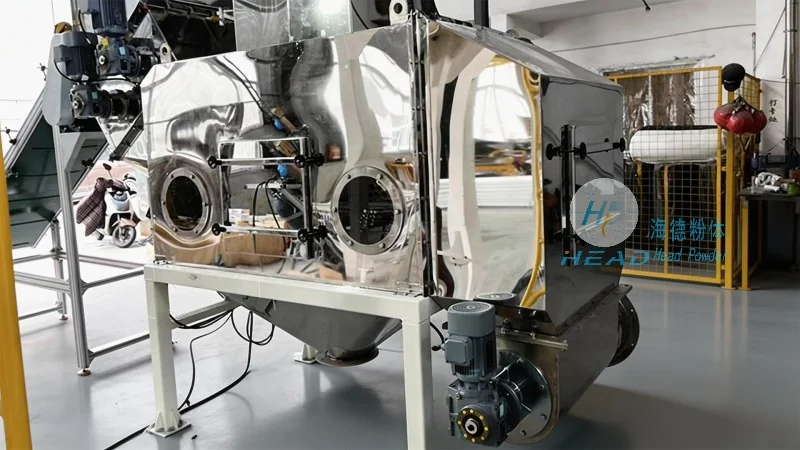
Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial material handling solutions, specializes in designing, manufacturing, and installing sand and gravel material conveying lines tailored to the specific needs of clients in the construction and mining sectors. With a focus on innovation and quality, the company leverages advanced engineering techniques to develop systems that meet the highest standards of performance and durability. HeadPowder's expertise in material flow dynamics and conveyor technology ensures that their solutions are optimized for efficiency, reliability, and cost-effectiveness. The company's operations are based in Shandong, China, where it serves a wide range of clients globally, delivering customized conveying systems that enhance operational productivity and reduce downtime.
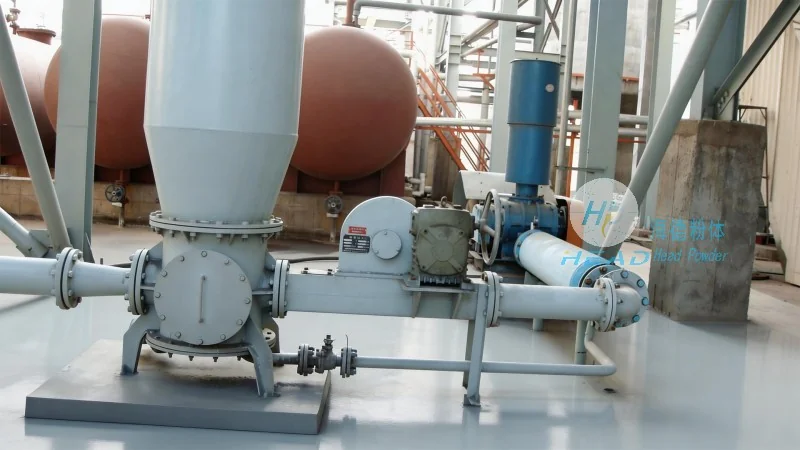
HeadPowder's sand and gravel material conveying lines are available in various configurations to suit different operational requirements. These systems can be customized in terms of conveyor length, width, and capacity to handle specific material volumes and particle sizes. The company offers a range of drive systems, including electric motors and gearboxes, to ensure optimal energy efficiency and performance. Additionally, the conveying lines are equipped with advanced control systems that allow for real-time monitoring and adjustment of material flow, enhancing operational flexibility. The materials used in the construction of these systems, such as high-strength steel and abrasion-resistant coatings, ensure long service life and minimal maintenance requirements. HeadPowder's commitment to quality and customer satisfaction is reflected in the detailed engineering and rigorous testing of each conveying line before deployment, ensuring that clients receive reliable and efficient solutions that meet their unique operational needs.
Sand and gravel material conveying lines are essential for modern industrial operations, providing efficient and reliable means of transporting bulk materials. The principles and working scene characteristics of these systems are designed to address the specific challenges of handling sand and gravel, ensuring optimal performance in diverse applications. Companies like Shandong HeadPowder Engineering Co., Ltd. play a crucial role in advancing material handling technology, offering customized solutions that enhance productivity and reduce operational costs. As the demand for efficient material transport continues to grow, the importance of well-designed conveying lines in industries such as construction and mining will only increase, driving further innovation and development in the field.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top