Compound fertilizer powder conveying systems are critical components in the modern agricultural and industrial sectors, designed to efficiently transport bulk powder materials such as fertilizers. These systems ensure reliable and safe material handling, which is essential for optimizing production processes and maintaining operational efficiency. The technology behind these systems combines advanced engineering principles with practical application, addressing the unique challenges of handling fine powders in various environments.
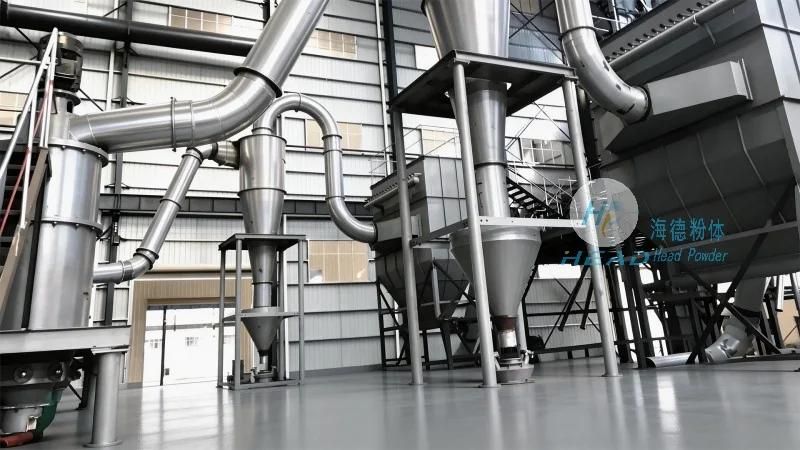
HeadPowder Engineering Co., Ltd., a leading provider in the field, specializes in the design, manufacturing, and implementation of high-performance powder conveying solutions. With a strong presence in Shandong, China, the company leverages decades of industry experience to deliver tailored systems that meet the specific needs of clients across different industries. The company's commitment to quality and innovation has established it as a trusted partner for businesses seeking reliable and efficient powder handling equipment.
The fundamental principle of compound fertilizer powder conveying systems revolves around the efficient movement of bulk powder materials from a source to a destination. These systems typically utilize a combination of mechanical and pneumatic technologies to achieve seamless and continuous material transport. Key components include hoppers, feeders, conveying pipes, and control systems, all working in harmony to ensure stable and controlled flow. The design focuses on minimizing material degradation, preventing blockages, and maintaining consistent pressure and flow rates, which are crucial for maintaining product quality and system reliability.
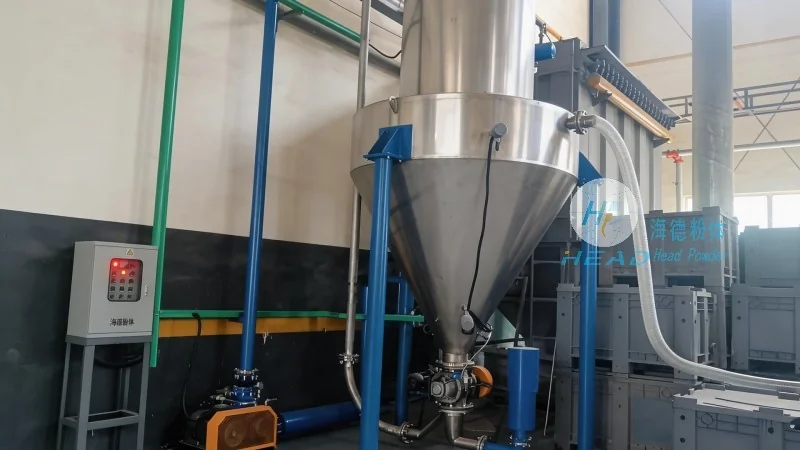
Compound fertilizer powder conveying systems are widely applied in diverse working environments, each with distinct characteristics that influence system design and operation. In agricultural settings, these systems are commonly used in fertilizer production facilities and storage yards, where they facilitate the transfer of raw materials and finished products to storage tanks or packaging lines. The systems are engineered to handle large volumes of fertilizer, ensuring that production lines operate at optimal capacity without interruptions. In industrial applications, such as chemical processing plants, the systems may be integrated into larger material handling networks, supporting the transport of various powders between processing stages. The adaptability of these systems allows them to be customized for different powder types, particle sizes, and operational conditions, making them suitable for a wide range of industrial processes.
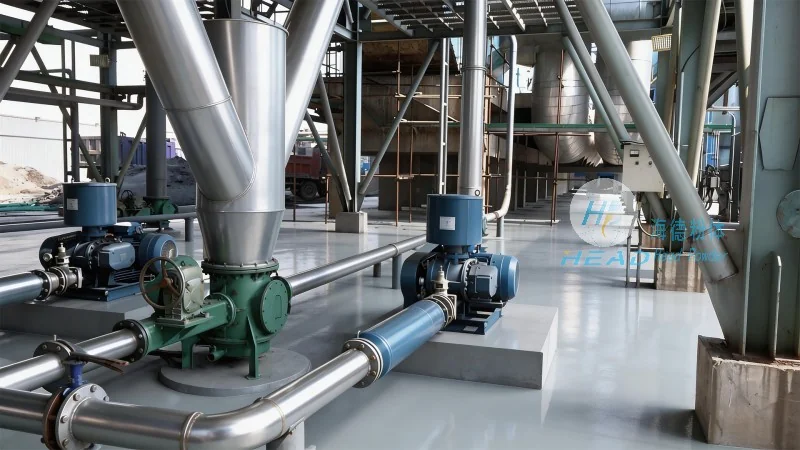
HeadPowder Engineering's compound fertilizer powder conveying systems are equipped with several key features that enhance performance and reliability. Advanced control systems enable precise regulation of flow rates and pressure, ensuring consistent material delivery. The use of durable materials, such as stainless steel and corrosion-resistant coatings, protects the system from the harsh conditions of fertilizer handling, extending its service life. Additionally, the systems are designed for easy maintenance and cleaning, reducing downtime and operational costs. The integration of safety features, including pressure relief valves and emergency stop mechanisms, ensures compliance with industry standards and protects personnel and equipment from potential hazards. These features collectively contribute to the overall efficiency and safety of the conveying process, making the systems ideal for both large-scale production and smaller-scale operations.
Compound fertilizer powder conveying systems, as exemplified by the solutions offered by HeadPowder Engineering Co., Ltd., represent a sophisticated blend of engineering and practical application. By understanding the core principles and working scene characteristics, businesses can select and implement systems that enhance operational efficiency, maintain product quality, and ensure safe material handling. The technology continues to evolve, with ongoing advancements in materials, control systems, and system integration, further improving the performance and reliability of powder conveying solutions. For companies in the fertilizer and related industries, investing in a well-designed and maintained powder conveying system is a strategic decision that supports long-term success and sustainability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top