Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, specializes in the design and manufacturing of advanced powder conveying systems tailored for industries such as brewing and feed production. With a focus on optimizing material handling efficiency, the company's solutions are engineered to meet the unique demands of handling barley malt and other fine powders. The company's headquarters is located in Shandong, China, where it leverages local industrial expertise and resources to develop cutting-edge technologies for powder processing.
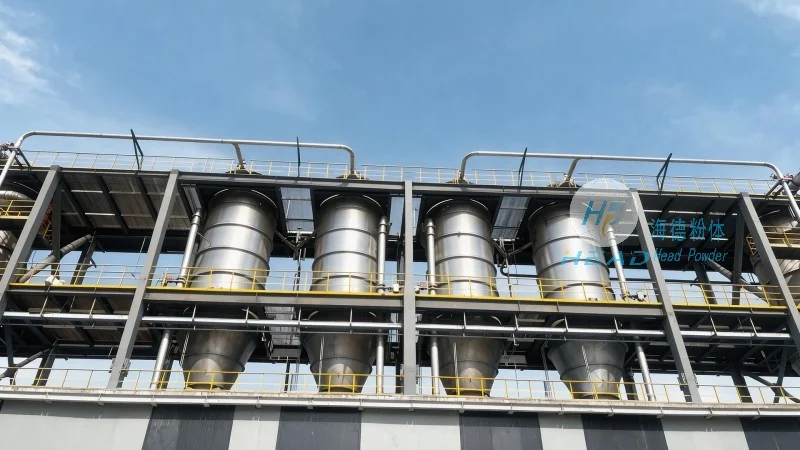
The core of the barley malt powder conveying system lies in its ability to transport fine powders like barley malt efficiently and reliably. These systems typically employ pneumatic or mechanical conveying technologies, each with distinct advantages depending on the application requirements. Pneumatic conveying, for instance, uses air pressure to move powders through pipelines, offering advantages in terms of speed and flexibility. This method is particularly effective for short to medium distance transport and can handle a wide range of powder characteristics. Mechanical conveying, on the other hand, relies on positive displacement or screw mechanisms to transport materials, which is often preferred for bulk handling and environments where air quality is a concern. The mechanical systems are generally more robust and can handle higher particle loads, making them suitable for heavy-duty industrial applications. The choice of technology is critical as it directly impacts the system's performance, energy consumption, and maintenance needs. Advanced systems may incorporate a combination of both pneumatic and mechanical components to achieve optimal results, such as using pneumatic transport for initial material movement and mechanical conveyors for final positioning.
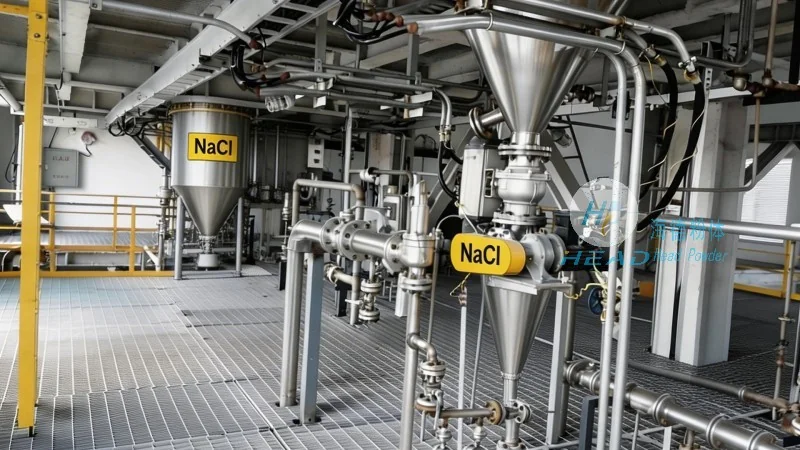
The working scene characteristics of barley malt powder conveying systems are shaped by the specific needs of industrial environments where they are deployed. In brewing facilities, for example, these systems are integral to the malt handling process, ensuring that raw materials are transported from storage silos to mashing tanks without degradation or contamination. The systems must be designed to handle the moisture content and particle size variations of barley malt, which can affect flowability and conveyance efficiency. In feed production plants, similar considerations apply, as the systems need to maintain hygiene standards and prevent cross-contamination between different product lines. Additionally, the systems are often integrated with other processing equipment, such as mixers and grinders, to form a seamless material handling workflow. The working scene characteristics also include considerations of space constraints, as many industrial facilities have limited room for large-scale equipment, requiring compact and modular designs. Environmental factors, such as temperature and humidity, are also critical, as they can influence the performance of the conveying components and the overall system reliability. For instance, in cold climates, the system may need to incorporate heating elements to prevent malt from clumping or freezing, while in humid environments, moisture-proof designs are essential to avoid material degradation. The systems are also designed to meet safety regulations, including explosion-proof features in areas where powders may be combustible, ensuring operational safety for personnel and equipment.
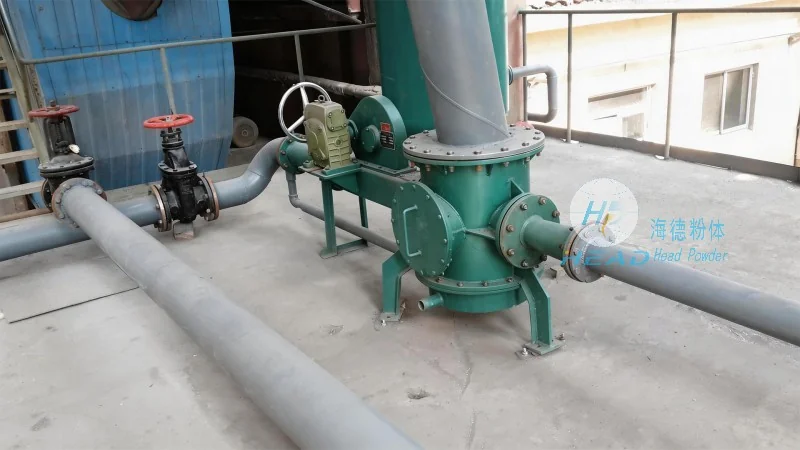
Headpowder's barley malt powder conveying systems are equipped with several key features that enhance their performance and reliability. One of the primary advantages is the use of high-quality materials for construction, such as stainless steel and corrosion-resistant alloys, which are essential for handling malt and other food-grade powders. These materials ensure durability and maintain hygiene standards, reducing the risk of contamination and extending the system's service life. The systems also incorporate advanced control systems, including programmable logic controllers (PLCs) and user-friendly interfaces, allowing for precise control over conveying speed, pressure, and material flow. This level of automation not only improves operational efficiency but also reduces the need for manual intervention, minimizing human error and labor costs. Additionally, the systems are designed for easy maintenance, with accessible components and modular designs that enable quick repairs and replacements. This reduces downtime and maintenance costs, making them a cost-effective solution for industrial applications. The company's expertise in customizing systems to specific customer requirements ensures that each installation is tailored to meet the unique operational needs of the facility, whether it is a small-scale brewery or a large-scale feed production plant.
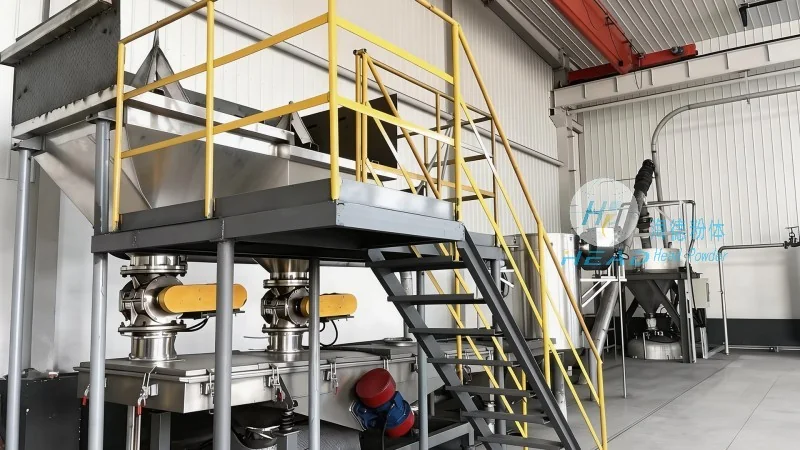
In summary, the barley malt powder conveying systems developed by Shandong HeadPowder Engineering Co., Ltd. represent a sophisticated solution for efficient and reliable material handling in the brewing and feed industries. By leveraging pneumatic and mechanical conveying technologies, advanced control systems, and robust construction materials, these systems address the specific challenges of handling barley malt and other fine powders. The working scene characteristics, including space constraints, environmental factors, and safety requirements, are carefully considered in the design process, ensuring that the systems are well-suited for a variety of industrial applications. As a result, headpowder's solutions contribute to improved operational efficiency, reduced maintenance costs, and enhanced product quality in the industries they serve.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top