When it comes to the efficient and reliable transportation of rice, various methods and systems are employed to ensure that this staple food reaches its destination in optimal condition. The process of rice transportation involves careful consideration of factors such as grain quality, moisture content, and the distance to be covered. Different methods are suited to different scenarios, from short-distance handling within a mill to long-distance shipping across regions or countries.
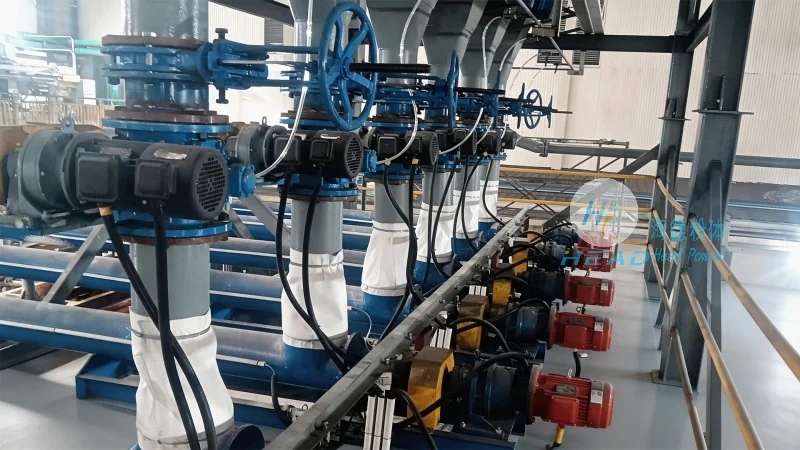
In the rice industry, several key methods are commonly used to move rice from the field to the consumer. These methods are designed to maintain the integrity of the grain while ensuring operational efficiency. The primary approaches include bulk handling systems, containerized transport, and specialized equipment tailored for rice characteristics.
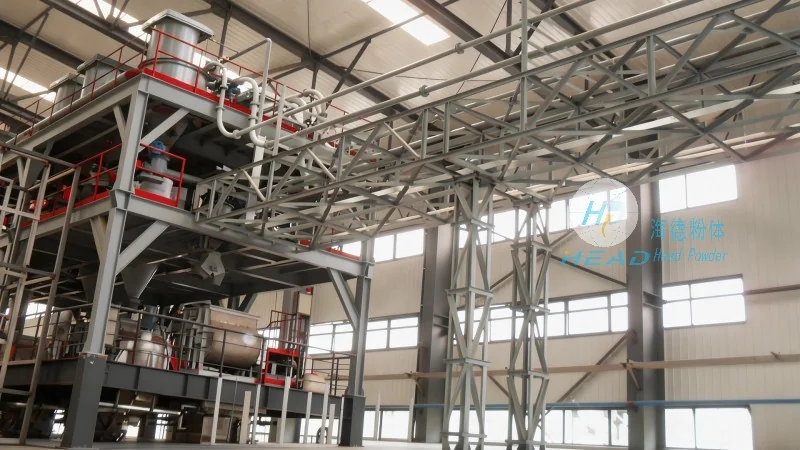
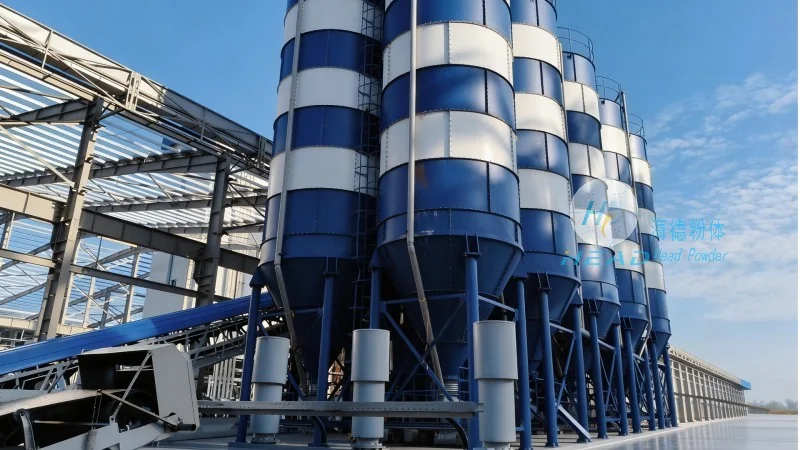
One of the most prevalent methods for rice transportation is through bulk handling systems. These systems are integral to modern rice mills and processing facilities, enabling the movement of large quantities of rice with minimal manual intervention. The process typically involves using conveyors, elevators, and pneumatic systems to transfer rice from storage silos or processing units to packaging or shipping areas. Bulk handling ensures that rice is moved in a continuous flow, reducing the risk of breakage and contamination. The equipment used in bulk handling, such as bucket elevators and belt conveyors, is specifically designed to handle the size and density of rice grains, ensuring smooth operation and minimal damage.
For long-distance transportation, especially in international trade, containerized transport has become the standard method for rice. This approach involves loading rice into standardized shipping containers, which are then transported via trucks, trains, or ships. Containerization provides several advantages, including protection from moisture, dust, and physical damage, as well as facilitating easier customs clearance and logistics coordination. The containers are often equipped with ventilation systems to maintain proper air circulation and prevent mold growth during transit. This method is particularly effective for exporting rice to global markets, as it allows for consistent quality control and compliance with international standards.
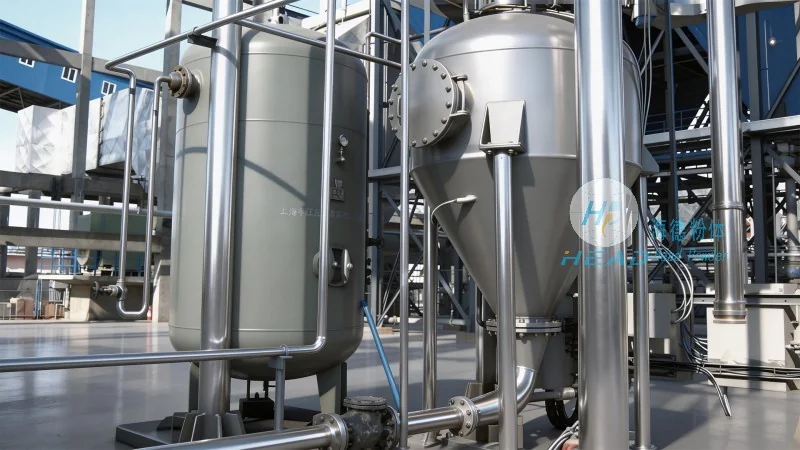
Given the unique properties of rice, such as its susceptibility to breakage and the need to maintain low moisture levels, specialized equipment is essential for its transportation. For example, some facilities use flexible conveyors or vibrating screens to gently move rice, reducing the risk of grain damage. Additionally, some systems incorporate air classification or aspiration to separate broken grains or impurities before transport. These specialized tools are crucial for maintaining the quality of rice, especially for premium varieties that command higher market prices. The use of such equipment reflects the industry's commitment to preserving the quality of rice throughout the supply chain.
Effective rice transportation requires careful planning and adherence to best practices to ensure that the grain remains in optimal condition. Key operational considerations include maintaining proper moisture levels, controlling temperature, and preventing contamination. Rice is highly sensitive to moisture, as excess moisture can lead to mold growth and spoilage. Therefore, during transportation, it is essential to use dry, well-ventilated containers and equipment. Temperature control is also critical, as high temperatures can accelerate the aging process of rice, reducing its nutritional value and market appeal. Additionally, strict hygiene protocols must be followed to prevent the introduction of foreign materials or pests that could compromise the quality of the rice.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of engineering solutions in the food processing industry, specializes in designing and manufacturing equipment for rice transportation and processing. With a focus on innovation and quality, the company offers a range of systems tailored to the specific needs of rice mills and exporters. The company's expertise lies in developing efficient bulk handling systems, containerized transport solutions, and specialized equipment that meet international standards. By leveraging advanced technology and a deep understanding of rice characteristics, Shandong HeadPowder Engineering Co., Ltd. helps clients optimize their rice transportation processes, ensuring minimal loss and maximum quality retention. The company's commitment to customer satisfaction and product reliability has made it a trusted partner in the global rice industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top