Glucose powder conveying systems are critical components in various industrial applications, particularly in the pharmaceutical, food, and chemical sectors where precise and efficient handling of powdered glucose is essential. This article explores the fundamental principles underlying these systems and highlights the key characteristics of their operational environments, with a focus on solutions provided by Shandong HeadPowder Engineering Co., Ltd.
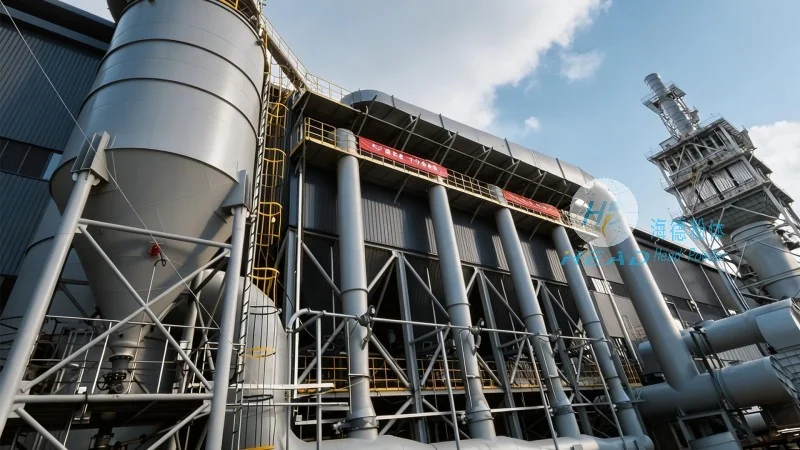
Glucose powder conveying systems are engineered to transport granular or powdered glucose from one location to another within a processing facility. The core of such systems lies in the combination of mechanical components and control mechanisms designed to ensure consistent flow, minimal product degradation, and adherence to sanitary standards. These systems are integral to processes ranging from raw material handling to final product packaging, making their reliability and efficiency paramount. Shandong HeadPowder Engineering Co., Ltd. specializes in the design and manufacturing of these systems, catering to the diverse needs of industries that rely on glucose powder handling.
The operation of glucose powder conveying systems is based on several key principles that ensure effective material movement. One primary method involves the use of pneumatic conveying, where air is used to transport the powder through a pipeline. This approach is particularly suitable for glucose powders due to its ability to handle fine particles without causing excessive friction or product attrition. Another common principle is mechanical conveying, which utilizes screws, belts, or buckets to move the powder. Mechanical systems are often preferred in environments where high pressure or large volumes of material need to be handled.
In pneumatic conveying, the system typically consists of a hopper, a feeder, a conveying line, and a receiver. The feeder controls the flow of glucose powder into the system, while the conveying line transports the material using compressed air. The receiver collects the material at the destination. This method allows for flexible routing and can be adapted to different operational requirements. Mechanical conveying systems, on the other hand, rely on rotating components to push or lift the powder. These systems are generally more robust and can handle larger quantities of material, but they may require more maintenance and are less suitable for very fine powders.
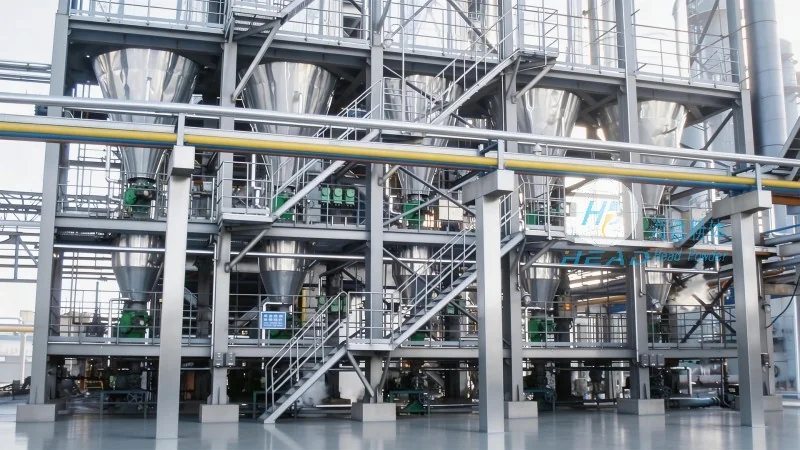
The working scene characteristics of glucose powder conveying systems vary significantly based on the industry and specific application. In pharmaceutical manufacturing, for instance, the systems must operate under stringent sanitary conditions, with materials that are often sensitive to moisture or contamination. This requires the use of stainless steel components, sealed systems, and rigorous cleaning protocols to maintain product integrity and compliance with regulatory standards. The systems from Shandong HeadPowder Engineering Co., Ltd. are designed to meet these stringent requirements, ensuring that pharmaceutical-grade glucose is handled without risk of contamination.
In the food industry, particularly in the production of glucose-based products like syrups or sweeteners, the conveying systems must ensure that the powder is handled hygienically and without cross-contamination. The systems are often integrated with other processing equipment, such as mixers or reactors, and must be designed to facilitate easy cleaning and maintenance. This is crucial for maintaining product quality and meeting food safety regulations. The company’s solutions are tailored to meet these needs, with features like CIP (Clean-in-Place) compatibility.
In chemical processing facilities, glucose powder conveying systems may be used in conjunction with other chemicals or reagents. The systems must be capable of handling a variety of particle sizes and densities, and may need to be equipped with special materials to resist corrosion or chemical reactions. The operational environment in such settings is often more demanding, with higher temperatures or pressures, requiring robust construction and advanced control systems. Shandong HeadPowder Engineering Co., Ltd. offers systems with durable materials and advanced control capabilities to handle these challenging conditions.
Glucose powder conveying systems offer several advantages that make them indispensable in modern industrial operations. One of the primary benefits is their ability to handle fine powders without causing agglomeration or product degradation. This is particularly important for glucose, which can clump together if not handled properly, affecting downstream processes. The systems also provide consistent flow rates, ensuring that the material is delivered to the next stage of production in a controlled manner.
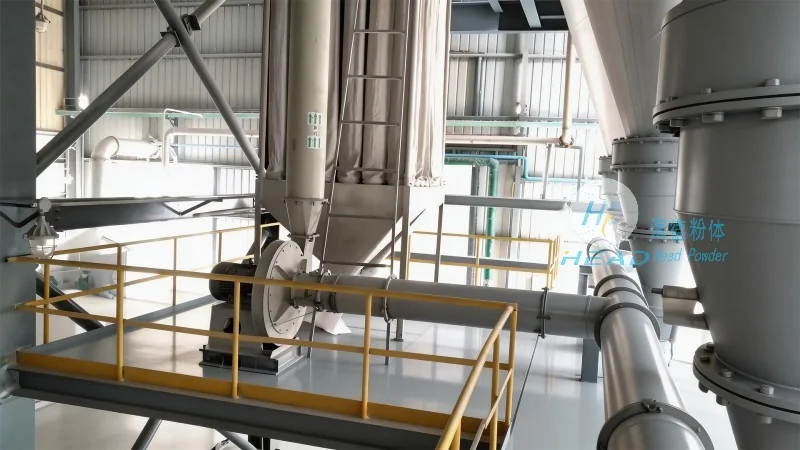
Another advantage is the flexibility in system design. Pneumatic conveying systems can be easily reconfigured to accommodate changes in production volume or process layout, making them adaptable to evolving operational needs. Mechanical conveying systems, while more rigid in design, offer high reliability and can handle large volumes of material with minimal downtime. Both types of systems can be integrated with automation and control systems, allowing for real-time monitoring and adjustment of parameters to optimize performance.
The systems also contribute to improved safety and efficiency in the workplace. By automating the powder handling process, they reduce the risk of manual handling, which can lead to dust exposure or product contamination. This not only enhances workplace safety but also improves overall operational efficiency by minimizing labor costs and reducing the time required for material transfer.
Glucose powder conveying systems are sophisticated and essential components in various industrial applications, particularly in the pharmaceutical, food, and chemical sectors. Their operation is based on fundamental principles of pneumatic or mechanical conveying, tailored to the specific characteristics of glucose powder and the operational environment. The working scene characteristics, such as sanitary requirements, material handling needs, and process integration, dictate the design and functionality of these systems. By understanding these principles and characteristics, industries can select and implement the most appropriate conveying system to ensure efficient, safe, and cost-effective handling of glucose powders. Shandong HeadPowder Engineering Co., Ltd. provides comprehensive solutions that meet these diverse requirements, supporting industries in achieving their operational goals.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top