Gravity dust removal powder material handling systems represent a sophisticated approach to managing the transport and filtration of fine particulate materials in industrial settings. These systems are engineered to efficiently separate dust from air streams while simultaneously transporting the collected material to designated storage or processing locations. The core technology behind such systems leverages principles of gravity and air dynamics to achieve both dust capture and material conveyance, making them an essential component in industries where airborne particulates are a common byproduct of operations.
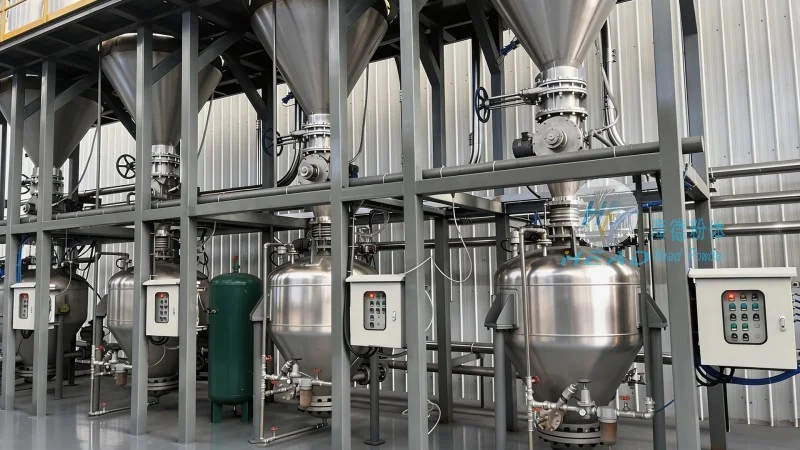
The fundamental principle of gravity dust removal systems is the use of gravity and differential air velocity to separate dust particles from the air. As contaminated air passes through the system, larger and heavier particles are forced to settle due to gravity, while finer particles are captured by filtration media. The system typically consists of a dust collection hopper, a filter section, and a material discharge mechanism. The hopper is designed to accumulate the collected dust, and the filter ensures that the air is cleaned before being released back into the environment or recirculated within the facility. The material discharge mechanism, often a gravity-fed valve or conveyor, then transports the settled dust from the hopper to a storage silo or processing unit.
Gravity dust removal powder material handling systems are widely employed in various industrial applications where the handling of fine powders and the need for dust control are critical. Common working scenes include cement and concrete production facilities, where large volumes of cement dust are generated during grinding and mixing processes. In these settings, the system efficiently captures dust from the production line, preventing air pollution and ensuring compliance with environmental regulations. Another prominent application is in the chemical and pharmaceutical industries, where the handling of sensitive powders requires strict dust control measures to maintain product purity and operational safety. The system's ability to handle abrasive and fine powders without clogging or degradation makes it suitable for these demanding environments.
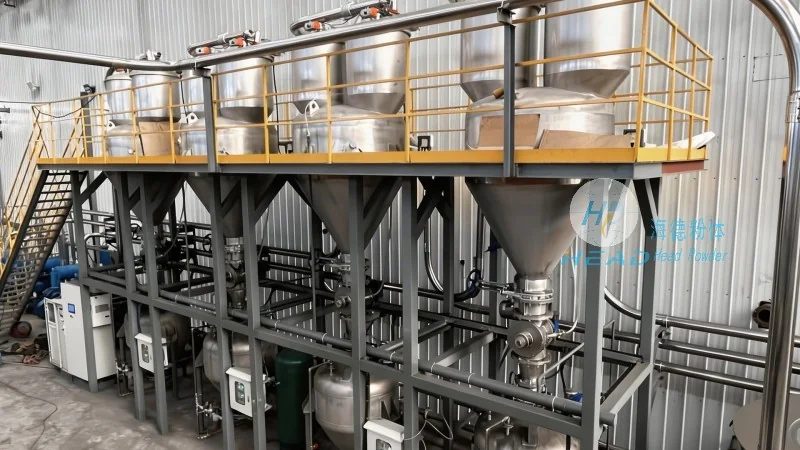
One of the key advantages of gravity dust removal powder material handling systems is their high efficiency in both dust capture and material transport. By utilizing gravity to settle larger particles and filtration to capture finer ones, the system achieves high collection efficiency, often exceeding 99% for most particulate sizes. This efficiency reduces the need for additional filtration or cleaning steps, lowering operational costs and maintenance requirements. Additionally, the system's design minimizes the risk of material re-entrainment, as the collected dust is directly transferred to storage without the need for mechanical agitation or high-pressure air streams. This reduces the potential for dust explosions and improves overall workplace safety. The operational simplicity of gravity-fed systems also contributes to their reliability, as they require fewer moving parts and less frequent maintenance compared to other material handling technologies.
When integrated into industrial processes, gravity dust removal powder material handling systems are designed to work seamlessly with existing production lines. The system can be connected directly to dust-generating equipment, such as grinding mills or mixers, to capture dust at the source. This source capture approach minimizes the spread of airborne particles throughout the facility, improving air quality and reducing the risk of dust-related health issues for workers. The collected material is then transported to a storage silo or processing unit, where it can be used as a raw material or disposed of as waste, depending on the application. The system's modular design allows for easy integration with existing infrastructure, reducing installation time and costs. Furthermore, the system can be equipped with monitoring and control systems to optimize performance and ensure consistent operation.
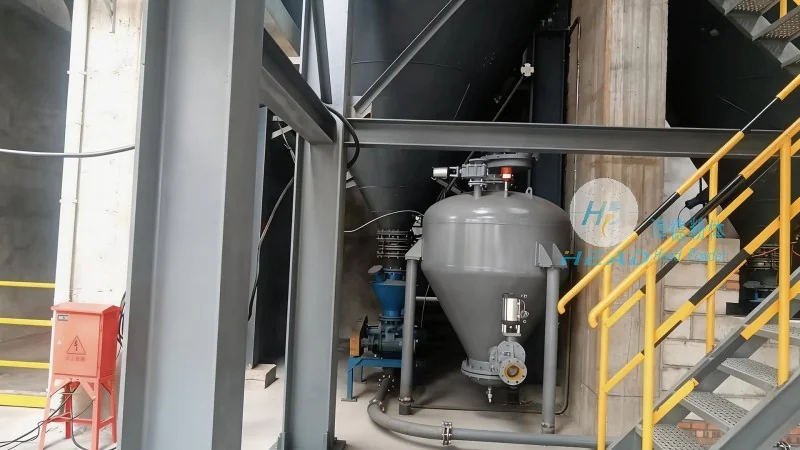
Maintenance of gravity dust removal powder material handling systems is relatively straightforward, contributing to their long operational life. Regular inspection of the filter media and hopper for clogging or accumulation is essential to maintain optimal performance. The filter media, typically made of high-efficiency particulate air (HEPA) or similar materials, may need to be replaced periodically depending on the dust load and particle size. The hopper and discharge mechanism should be checked for blockages or wear, as these can affect the smooth transport of material. Proper maintenance practices, including cleaning and lubrication of moving parts, extend the lifespan of the system and ensure consistent performance over time. The use of durable materials in the construction of the system, such as stainless steel or corrosion-resistant alloys, further enhances its longevity, especially in harsh industrial environments.
Gravity dust removal powder material handling systems play a crucial role in meeting environmental and safety compliance standards in industrial operations. By effectively capturing and containing dust, these systems help facilities comply with local and national regulations regarding air quality and particulate emissions. The reduction of airborne dust not only improves the working environment for employees but also minimizes the risk of dust explosions, which can be a significant safety hazard in powder handling operations. The system's design, with its enclosed hopper and sealed discharge mechanism, prevents dust from escaping into the workplace, reducing the potential for respiratory health issues among workers. Additionally, the ability to recycle collected dust as a raw material reduces waste and promotes sustainable practices within the industry. Overall, the implementation of gravity dust removal systems contributes to a safer, cleaner, and more environmentally responsible industrial operation.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top