HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced dust-free automatic powder handling systems. These systems are engineered to meet stringent industrial requirements for cleanroom environments and efficient material transport. This article explores the fundamental principles behind such systems and highlights key working scenarios where their application is crucial.
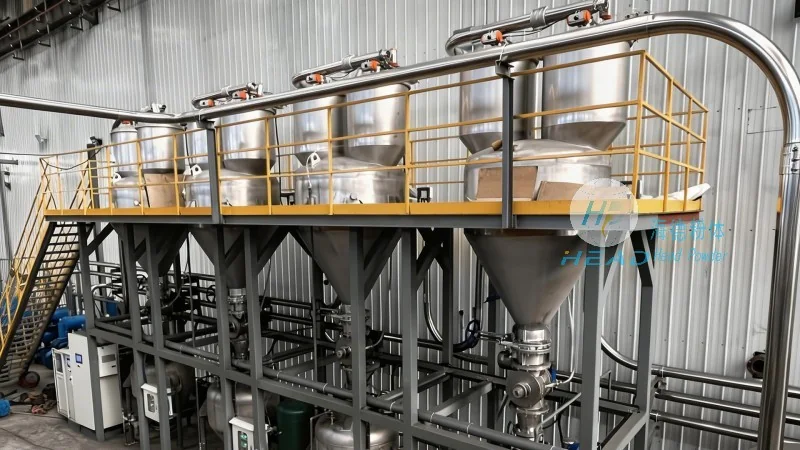
The dust-free automatic powder conveying system operates on the principle of creating a sealed environment to prevent powder contamination and air leakage. Key components include airtight hoppers, flexible hoses or rigid pipes with sealed joints, and advanced filtration systems. The system typically uses either negative pressure (suction) or positive pressure (blowing) to move powder particles through the pipeline. Negative pressure draws powder from the source into the system, while positive pressure pushes it forward. Both methods are equipped with high-efficiency particulate air (HEPA) filters to ensure that any residual particles are captured before the air is released, maintaining a clean and safe working environment.
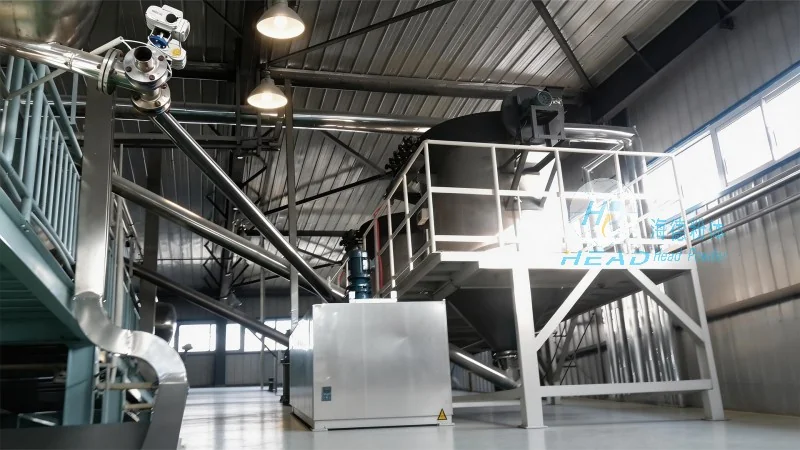
The application of dust-free automatic powder handling systems spans multiple industries, each with unique demands for material handling and environmental control. In the pharmaceutical industry, these systems are essential for adhering to Good Manufacturing Practice (GMP) standards, where contamination control is paramount. They are used to transport active pharmaceutical ingredients (APIs), excipients, and other powders without exposing them to airborne contaminants. In the food and beverage sector, the systems comply with sanitary standards, ensuring that powders like flour, sugar, or protein powders are handled hygienically, preventing cross-contamination and maintaining product purity. The chemical industry also benefits from these systems, especially when handling hazardous or reactive powders, as they provide a safe and enclosed method to transport materials while minimizing the risk of dust explosions or chemical exposure.
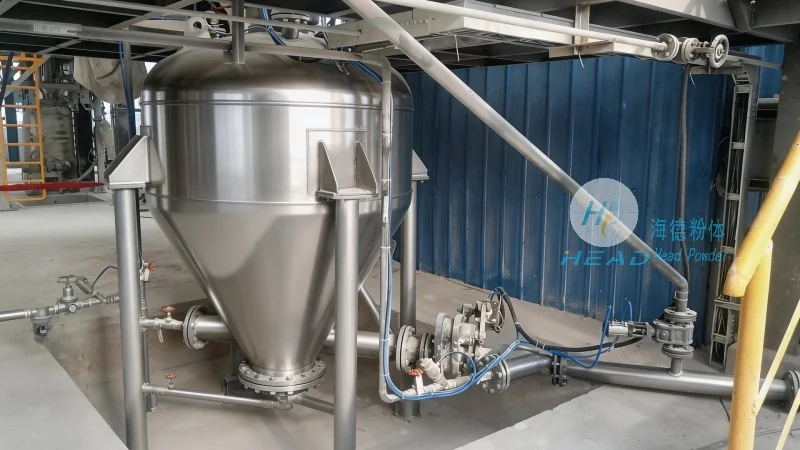
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a professional enterprise dedicated to the research, development, and manufacturing of powder handling equipment. With its headquarters in Shandong, China, the company leverages years of industry experience to deliver customized solutions tailored to specific customer needs. The company’s products are designed to integrate seamlessly with existing production lines, offering flexibility and scalability for various industrial applications. By focusing on innovation and quality, HeadPowder aims to provide reliable and efficient powder conveying solutions that enhance operational efficiency and safety in diverse industrial settings.
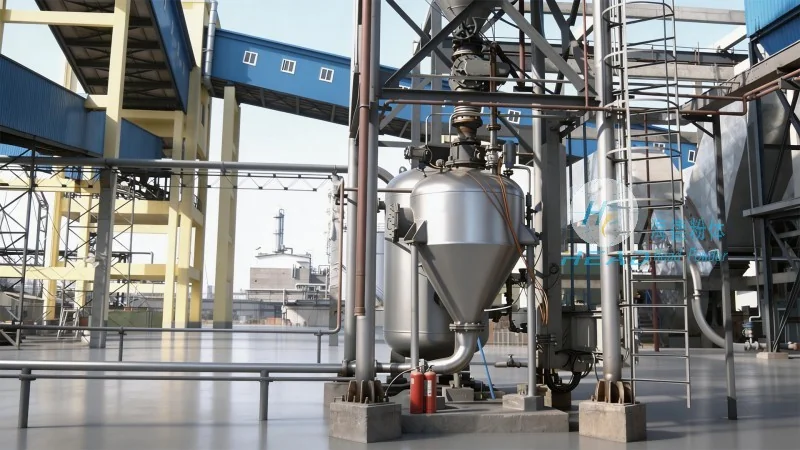
The dust-free automatic powder handling system offers several technical advantages that make it a preferred choice in industries where powder handling is critical. One of the primary benefits is the elimination of dust contamination, which not only protects the product quality but also ensures compliance with regulatory standards. The sealed system design reduces the risk of dust inhalation by employees, enhancing workplace safety. Additionally, the system improves material handling efficiency by automating the transport process, reducing manual labor and minimizing the time required for material transfer. The use of advanced filtration and sealing technologies also leads to lower maintenance costs and longer equipment lifespan, as the components are protected from dust and moisture damage. Overall, these systems provide a cost-effective and sustainable solution for industries seeking to optimize their powder handling processes while maintaining high standards of cleanliness and safety.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top