Understanding the principles and application scenarios of sulfur powder conveying is crucial for industries that rely on efficient material handling. Sulfur, a key chemical compound used in various industrial processes, requires specialized equipment and methods to ensure safe and effective transport. This article explores the fundamental principles behind sulfur powder conveying systems and highlights the key characteristics of different work scenarios where such systems are applied.
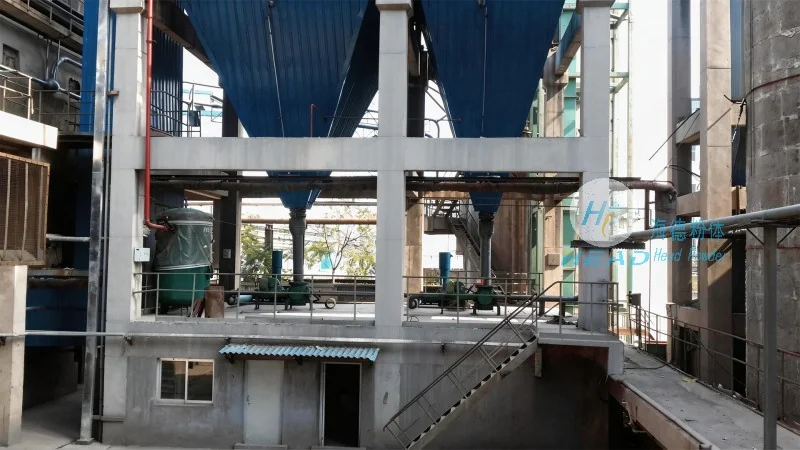
The primary principle of sulfur powder conveying involves the use of mechanical or pneumatic systems to transport sulfur particles from one location to another. In industrial settings, sulfur is often handled in bulk quantities, making efficient conveying essential to maintain production efficiency and safety standards. There are two main types of conveying systems commonly used for sulfur powder: pneumatic conveying and mechanical conveying. Pneumatic systems utilize air or other gases to move the powder through a pipeline, while mechanical systems rely on rotating components like screws or belts to transport the material.
Pneumatic conveying is particularly effective for sulfur powder due to its ability to handle fine particles and minimize dust generation. This method involves creating a pressure differential within the pipeline, which draws the sulfur powder along with the air stream. The system typically includes a hopper, a conveyor line, and a receiver, with optional components like cyclones or filters to separate the powder from the air. Mechanical conveying, on the other hand, is often preferred for applications where high temperatures or corrosive environments are present, as it avoids the use of air and reduces the risk of oxidation or contamination.
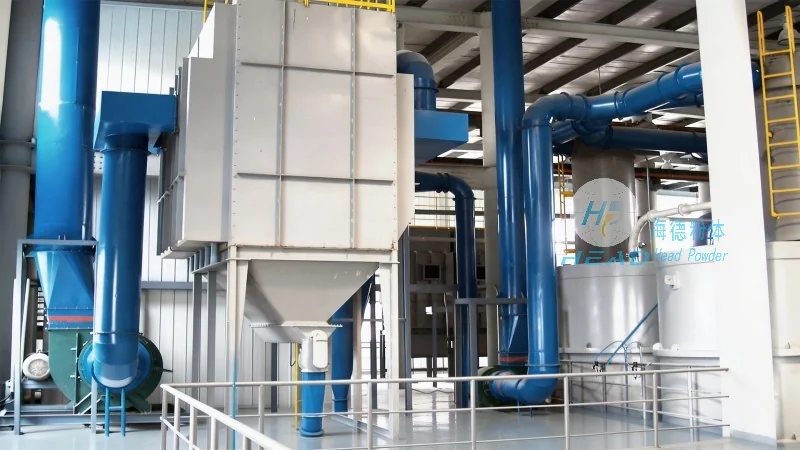
Effective sulfur powder conveying systems are designed with several key features to ensure optimal performance. First, the system must be capable of handling the specific properties of sulfur powder, such as its density, moisture content, and particle size distribution. Sulfur is a brittle material that can easily break into fine particles, which can lead to clogging or increased dust if not properly managed. Therefore, conveying systems often include features like vibration feeders or rotary valves to prevent blockages and maintain a consistent flow rate.
Second, the equipment must be constructed from materials that are resistant to sulfur's corrosive nature. Sulfur, especially when in a molten state, can attack metal surfaces, leading to wear and tear over time. Common materials used in the construction of conveying components include stainless steel, carbon steel with protective coatings, and specialized alloys designed to withstand chemical exposure. Additionally, the system should be equipped with temperature control mechanisms to prevent overheating, as sulfur can decompose at high temperatures, releasing toxic gases.
Sulfur powder conveying systems are widely used in various industrial sectors, each with unique requirements and challenges. One of the most common applications is in the chemical industry, where sulfur is used as a raw material for the production of sulfuric acid, fertilizers, and other chemicals. In these settings, the conveying system must be able to handle large volumes of sulfur powder and integrate seamlessly with existing production lines. Another key application is in the metallurgical industry, where sulfur is used as a flux or additive in the smelting of metals like copper and lead. Here, the system must be able to transport sulfur to the furnace while maintaining a stable temperature and preventing contamination.
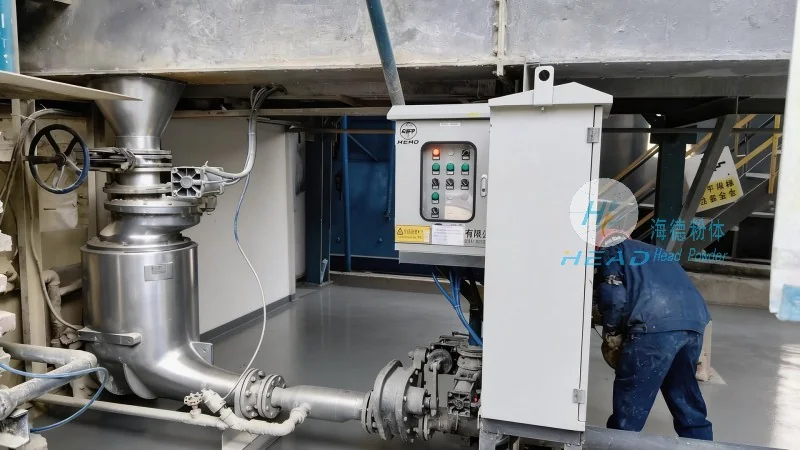
In the pharmaceutical and food processing industries, sulfur is used as a preservative or processing aid, requiring a more controlled and hygienic conveying system. These applications demand equipment that is easy to clean and maintain, with minimal risk of cross-contamination. The conveying system must also be designed to prevent the release of dust or fumes, as sulfur dust can be hazardous to human health. Finally, in the mining industry, sulfur is extracted from natural sources and transported to processing facilities. Here, the system must be robust enough to handle abrasive and heavy materials while maintaining efficiency over long distances.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of specialized conveying solutions for industrial applications. With a focus on innovation and quality, HeadPowder has developed advanced systems tailored to the unique needs of sulfur powder handling. The company's expertise lies in designing and manufacturing equipment that ensures safe, efficient, and reliable transport of sulfur and other fine powders. HeadPowder's products are known for their durability, low maintenance requirements, and compliance with international safety standards. Based in Shandong, China, HeadPowder serves clients globally, offering customized solutions to meet the diverse demands of the chemical, metallurgical, and other industries.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top