Positive pressure dilute phase powder conveying systems represent a sophisticated technology designed to transport bulk powders efficiently over long distances. This system operates by creating a positive pressure environment within the conveying pipeline, ensuring that the powder particles are suspended in a gas stream, typically air or a mixture of air and inert gases. The core principle involves the use of high-pressure blowers or compressors to generate the necessary airflow, which propels the powder through the system while maintaining a low concentration of particles in the gas phase. This approach is particularly effective for handling fine or cohesive powders, as it minimizes blockages and ensures consistent flow rates.
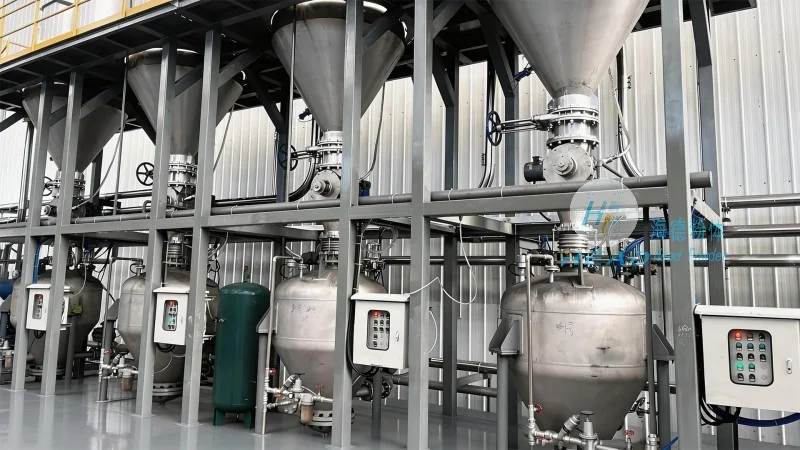
The fundamental mechanism of a positive pressure dilute phase powder conveying system relies on the balance between the pressure differential and the particle size, density, and moisture content of the material being transported. The system typically consists of a material feed hopper, a rotary valve or feeder to control the flow rate, a positive displacement blower or centrifugal fan to generate the conveying air, a pipeline network, and a receiver or discharge hopper at the destination. The blower supplies compressed air at a pressure sufficient to overcome the resistance in the pipeline and the gravitational forces acting on the powder particles. As the air flows through the pipeline, it entrains the powder particles, creating a dilute phase mixture. The velocity of the gas stream is maintained above the minimum fluidization velocity of the powder to prevent settling and ensure smooth transport. This principle allows for the reliable and continuous movement of powders from the source to the destination without the need for mechanical components in direct contact with the powder, reducing wear and maintenance costs.
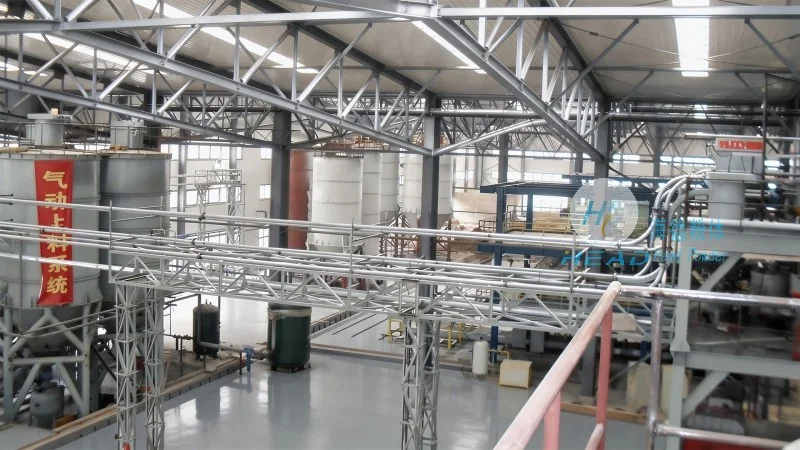
Positive pressure dilute phase powder conveying systems are widely used in various industrial applications due to their adaptability and efficiency. Common working scenes include the transportation of cement, flour, and other fine powders in the construction and food industries. In the cement industry, these systems are essential for moving raw materials like limestone and clinker from storage silos to the production lines, ensuring a steady supply for cement manufacturing. The food industry utilizes such systems for conveying flour, sugar, and other ingredients in food processing plants, maintaining hygiene and preventing contamination. Additionally, in chemical and pharmaceutical sectors, these systems handle powders like chemicals and active pharmaceutical ingredients (APIs), where precise control over particle size and flow is critical. The working scene characteristics also include the ability to handle long-distance transport, often exceeding several kilometers, with minimal pressure drop and energy consumption. The systems are designed to operate in both indoor and outdoor environments, with appropriate sealing and weatherproofing to protect against dust and moisture. This versatility makes them suitable for a wide range of industrial settings, from small-scale operations to large-scale manufacturing facilities.
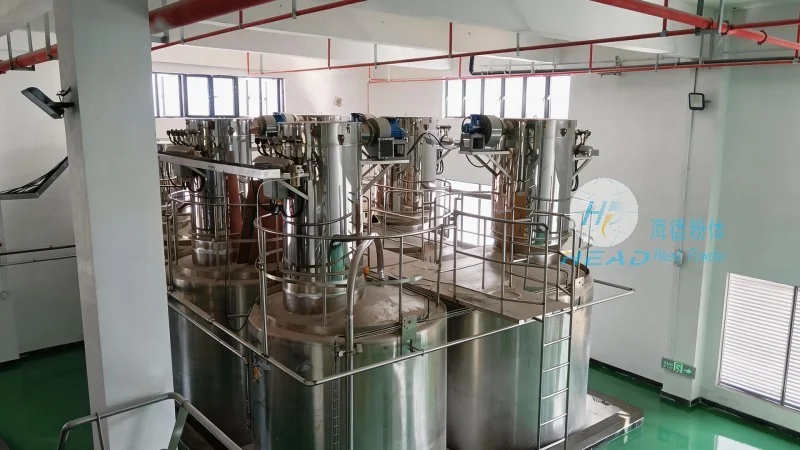
One of the primary advantages of positive pressure dilute phase powder conveying systems is their high efficiency in material transport. By maintaining a dilute phase, the system minimizes the risk of blockages and ensures consistent flow rates, which is crucial for maintaining production line stability. The use of positive pressure also reduces the need for vacuum systems, which can be less effective for handling fine powders and may require more energy. Another key advantage is the low maintenance requirement, as the system relies on air as the conveying medium, eliminating the need for mechanical components that come into direct contact with the powder. This reduces wear and tear and extends the service life of the equipment. Performance metrics for these systems typically include conveying capacity, which can range from a few kilograms per hour to several tons per hour, depending on the system size and the properties of the powder. The pressure drop across the pipeline is another critical metric, as it indicates the energy efficiency of the system. A lower pressure drop means less energy consumption and lower operating costs. Additionally, the system's ability to handle varying particle sizes and moisture content without significant performance degradation is a significant advantage, making it suitable for diverse applications.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of advanced powder conveying systems. With a strong presence in China, the company specializes in designing, manufacturing, and installing positive pressure dilute phase powder conveying systems tailored to the specific needs of various industries. Headpowder's expertise lies in understanding the unique challenges of powder handling, such as particle size distribution, moisture content, and flow characteristics, and developing customized solutions that address these challenges effectively. The company's products are known for their reliability, efficiency, and durability, meeting the stringent requirements of modern industrial applications. Headpowder's commitment to quality and innovation has made it a trusted partner for businesses seeking to optimize their powder transport processes. The company's facilities in Shandong, China, are equipped with state-of-the-art technology and skilled personnel, ensuring that each system is manufactured to the highest standards. This dedication to quality and customer satisfaction has helped headpowder establish a strong reputation in the global market, serving clients across various sectors including construction, food, chemical, and pharmaceutical industries.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top