Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a professional enterprise dedicated to the research, development, and application of powder conveying technologies. Based in Shandong, China, the company specializes in providing efficient and reliable solutions for the transportation of ammonium fertilizer powders, which are critical components in modern agricultural practices. This article explores the fundamental principles behind ammonium fertilizer powder conveying and highlights the key characteristics of its working scenarios, offering insights into the technology's practical applications.
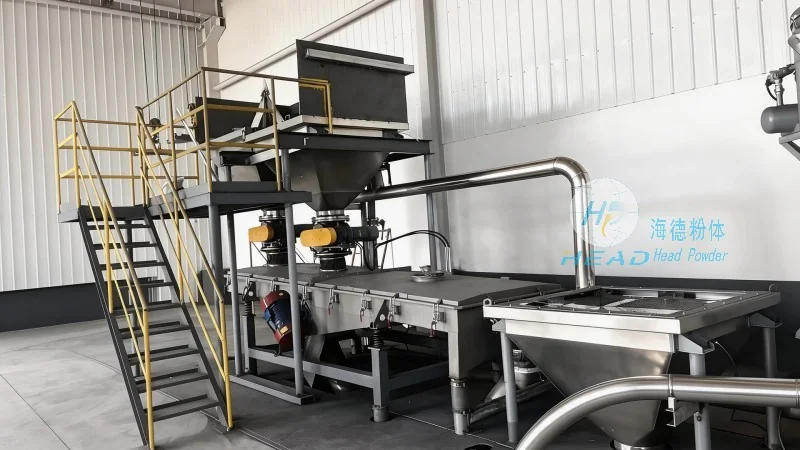
Ammonium fertilizer powder conveying involves the movement of granular or powdered ammonium-based fertilizers from one location to another, typically within agricultural facilities or between production and storage sites. The core principle of this process is to ensure the safe, efficient, and consistent transfer of the fertilizer, minimizing loss and degradation while maintaining product quality. There are primarily two methods used for powder conveying: pneumatic conveying (air-assisted) and mechanical conveying (e.g., screw conveyors, belt conveyors). Pneumatic conveying utilizes compressed air to create a flow that transports the powder through a pipeline, while mechanical systems rely on mechanical force to move the material. Both methods have distinct advantages and are selected based on factors such as the type of fertilizer, the distance of transport, and the required throughput.
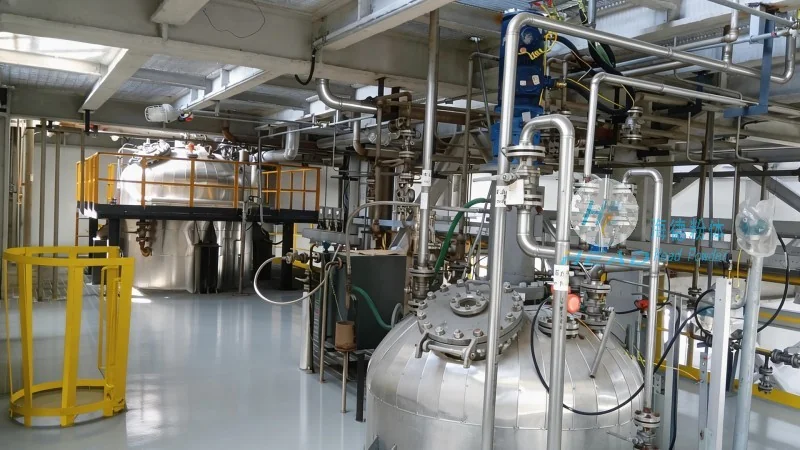
The working scene characteristics of ammonium fertilizer powder conveying are influenced by several factors, including the scale of operation, the environment, and the specific requirements of the agricultural or industrial setting. For instance, in large-scale fertilizer production plants, the conveying system must handle high volumes of material with minimal downtime, ensuring smooth production flow. The design of the conveying system is tailored to these operational demands, often incorporating features like automated control systems and robust material handling components. Additionally, the working environment, such as temperature and humidity, plays a role in determining the type of equipment used. For example, in outdoor or open-air storage facilities, the conveying system may need to be weather-resistant to protect the fertilizer from moisture and other environmental factors. Another critical characteristic is the need for safety measures, as ammonium fertilizers can be sensitive to certain conditions, and proper handling is essential to prevent accidents or product degradation.
In agricultural settings, ammonium fertilizer powder conveying is essential for distributing the fertilizer to fields, greenhouses, or other cultivation areas. The efficiency of the conveying system directly impacts the productivity of the farming operation, as delays or inefficiencies can lead to reduced crop yields. The working scene characteristics in this context include the need for flexibility, as different crops may require varying amounts of fertilizer at different times. The system must also be able to handle different types of ammonium fertilizers, such as urea or ammonium nitrate, each with its own unique properties and handling requirements. Furthermore, the environmental impact of the conveying process is a consideration, as minimizing dust and emissions is important for both worker safety and compliance with regulations. The design of the conveying system often incorporates dust collection and filtration systems to mitigate these concerns, ensuring a clean and safe working environment.
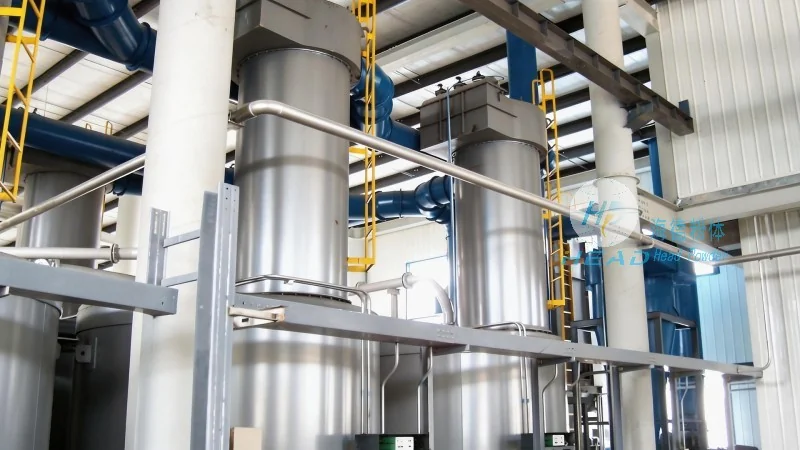
As technology advances, the field of ammonium fertilizer powder conveying continues to evolve, with new innovations aimed at improving efficiency and sustainability. For example, advancements in control systems allow for real-time monitoring and adjustment of the conveying process, optimizing energy usage and reducing waste. Additionally, the integration of automation and robotics in powder handling systems enhances precision and reduces the risk of human error. These technological developments are particularly relevant for large-scale operations, where consistency and reliability are paramount. Looking ahead, the trend towards more sustainable and eco-friendly practices may drive further innovations, such as the use of renewable energy sources for conveying and the development of more efficient materials for the equipment itself. However, the fundamental principles of powder conveying remain unchanged, as the need for reliable and efficient fertilizer transportation will continue to be a critical aspect of agricultural production.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top