High-pressure bin pump pneumatic conveying equipment represents a sophisticated solution for the efficient and reliable transport of bulk powders in industrial settings. This technology has become increasingly vital across various sectors, including chemical, food processing, and pharmaceutical industries, where the safe and efficient handling of powders is critical.
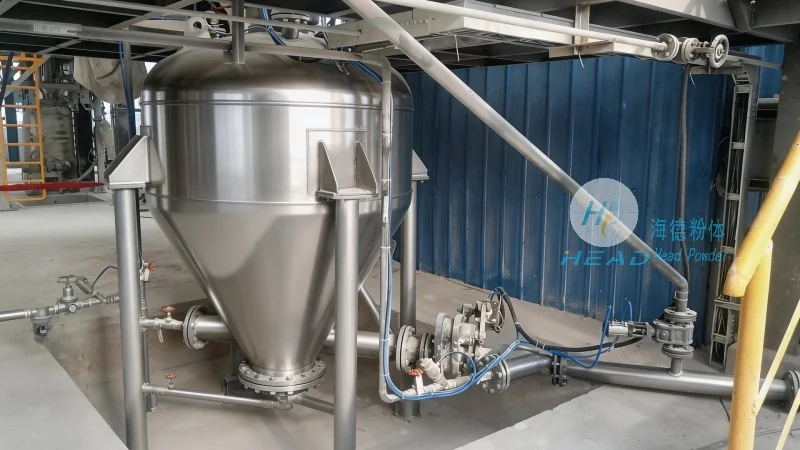
The core mechanism of high-pressure bin pump systems involves the use of a high-pressure air compressor to generate a powerful air stream that propels powder particles through a pipeline network. The process typically begins with the powder being stored in a hopper or silo, from which it is drawn into the pump chamber. As the air compressor operates, it creates a high-pressure environment that forces the air and powder mixture through the conveying line. The bin pump itself acts as a positive displacement pump, ensuring consistent flow rates and pressure levels, which are essential for maintaining the integrity of the powder and preventing clogging or degradation.
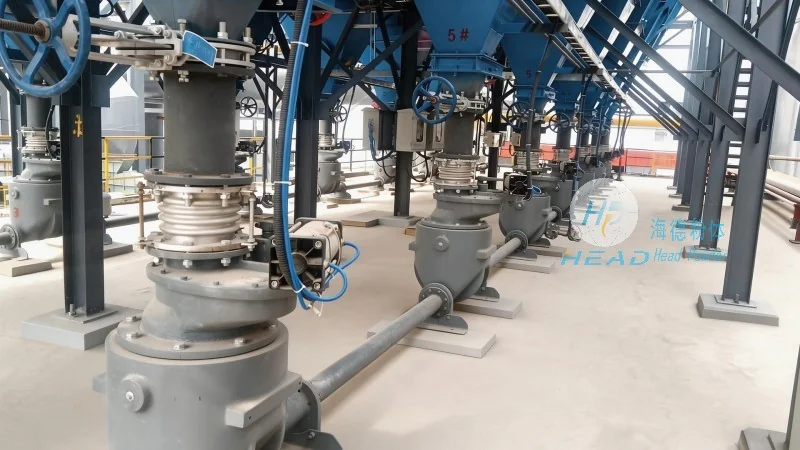
One of the most significant advantages of high-pressure bin pump pneumatic conveying equipment is its ability to handle a wide range of powder types, from fine powders to bulkier granules, with minimal degradation. The high-pressure air stream ensures that the powder is transported at high velocities, reducing the risk of particle agglomeration and maintaining product quality. Additionally, these systems offer excellent flexibility in terms of layout, as they can be configured to serve multiple destinations from a single source, making them ideal for complex production lines. Another key feature is the system's reliability and low maintenance requirements. The positive displacement design minimizes wear and tear on components, leading to longer operational life and reduced downtime. Furthermore, high-pressure bin pumps are energy-efficient compared to other pneumatic conveying methods, as they use less air at higher pressures, resulting in lower operational costs over time.
High-pressure bin pump systems are particularly well-suited for applications where precision and control are paramount. For instance, in the food and beverage industry, these systems are used to transport ingredients such as flour, sugar, and spices, ensuring that the product remains free from contamination and maintains its original properties. In the chemical industry, they are employed to handle reactive or hazardous powders, where the ability to control pressure and flow is crucial for safety. The pharmaceutical sector also benefits from the sterile and controlled environment that high-pressure bin pumps provide, as they can be integrated with cleanroom facilities to meet stringent regulatory standards. Furthermore, the system's ability to handle abrasive powders without causing excessive wear on the equipment makes it a preferred choice in mining and mineral processing applications.
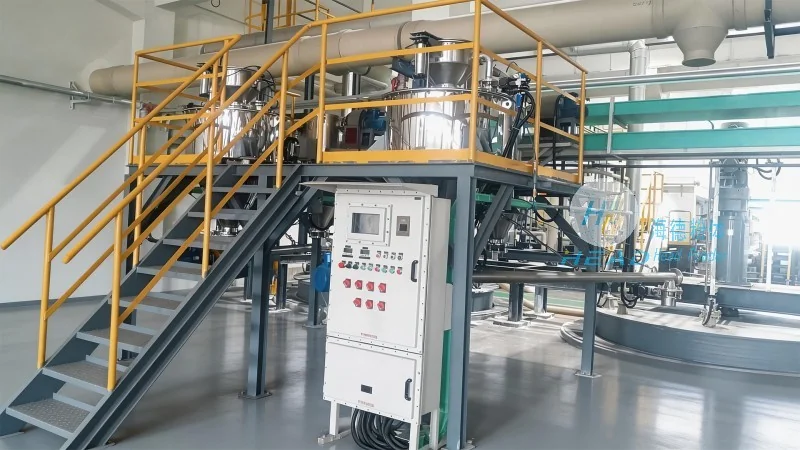
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of high-pressure bin pump pneumatic conveying equipment. With a strong focus on innovation and quality, the company has established itself as a trusted partner for businesses seeking reliable powder handling solutions. HeadPowder's products are designed to meet the diverse needs of industrial clients, offering customized solutions that enhance operational efficiency and product integrity. The company's commitment to research and development ensures that its equipment incorporates the latest technological advancements, such as advanced control systems and energy-saving features. HeadPowder's facilities are located in Shandong, China, where the company leverages local expertise and resources to deliver high-quality products to global markets. By combining technical expertise with customer-centric service, HeadPowder aims to provide sustainable and efficient powder conveying solutions that meet the evolving demands of modern industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top