Shandong HeadPowder Engineering Co., Ltd., a professional enterprise based in Shandong, China, specializes in providing comprehensive technical solutions for sodium bicarbonate processing and transportation systems. This article focuses on the key technical parameters and the detailed process of the transport system for sodium bicarbonate, offering insights into the engineering and operational aspects essential for efficient handling and delivery of this chemical compound.
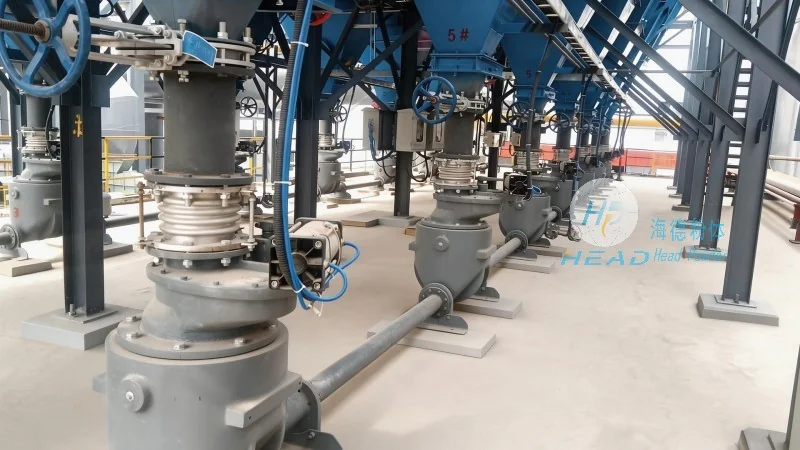
Sodium bicarbonate, also known as baking soda, is a white crystalline powder with a slightly alkaline taste. Its chemical formula is NaHCO₃, and it is widely used in various industries including food, pharmaceuticals, and chemical manufacturing. The technical parameters of sodium bicarbonate are crucial for ensuring its quality, stability, and suitability for different applications. Key parameters include:
1. **Particle Size Distribution**: The particle size of sodium bicarbonate affects its flowability, solubility, and reactivity. Typically, industrial-grade sodium bicarbonate has a particle size ranging from 0.1 to 2.0 millimeters, with a specific surface area that influences its performance in processes such as mixing and dissolution.
2. **Moisture Content**: The moisture content is a critical parameter as it impacts the product's hygroscopic nature and storage stability. Proper moisture control is essential to prevent caking and maintain the desired physical properties. The standard moisture content for sodium bicarbonate is usually below 0.5%, ensuring it remains dry and free-flowing.
3. **Purity and Impurities**: The purity level, often expressed as the percentage of NaHCO₃, is vital for meeting industry standards and regulatory requirements. Impurities such as sodium chloride, calcium carbonate, or other contaminants can affect the product's effectiveness and safety. High-purity sodium bicarbonate (typically over 99.5%) is required for pharmaceutical and food applications.
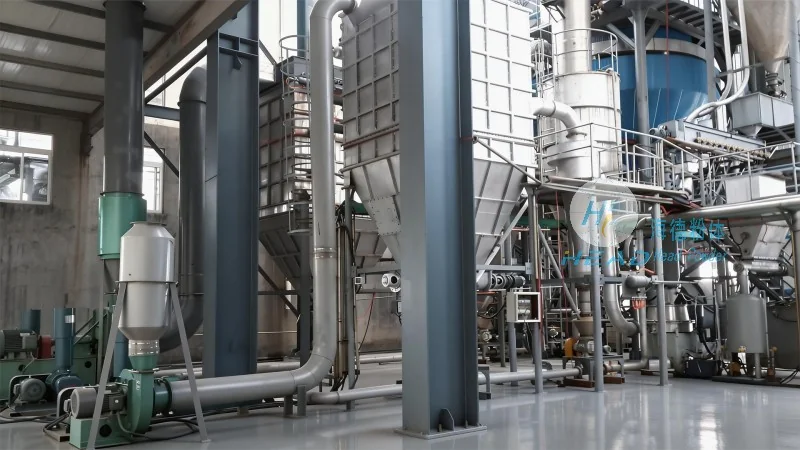
4. **Density and Bulk Density**: The density of sodium bicarbonate is approximately 2.2 g/cm³, while its bulk density varies depending on the particle size and packing. Bulk density is important for storage and transportation, as it determines the volume occupied by a given mass of the material. For example, a bulk density of 0.8 to 1.2 g/cm³ is common for powdered sodium bicarbonate, affecting the design of storage silos and conveyor systems.
The transport system for sodium bicarbonate involves several stages to ensure safe, efficient, and consistent delivery from the production site to the end-users. The process typically includes material handling, storage, and conveying equipment, all designed to maintain the product's quality and integrity.
1. **Material Handling and Loading**: After production, sodium bicarbonate is transferred from the reaction vessel to a storage silo or hopper. This step involves using vacuum or pressure systems to move the material, ensuring minimal dust generation and contamination. The loading process is carefully controlled to avoid agglomeration and maintain the desired particle size distribution.
2. **Storage and Conditioning**: The storage silo is equipped with aeration systems to control moisture and prevent caking. The material is often stored under controlled conditions, such as low humidity and temperature, to preserve its properties. Conditioning equipment, like vibrators or agitators, may be used to keep the material free-flowing and prevent blockages.
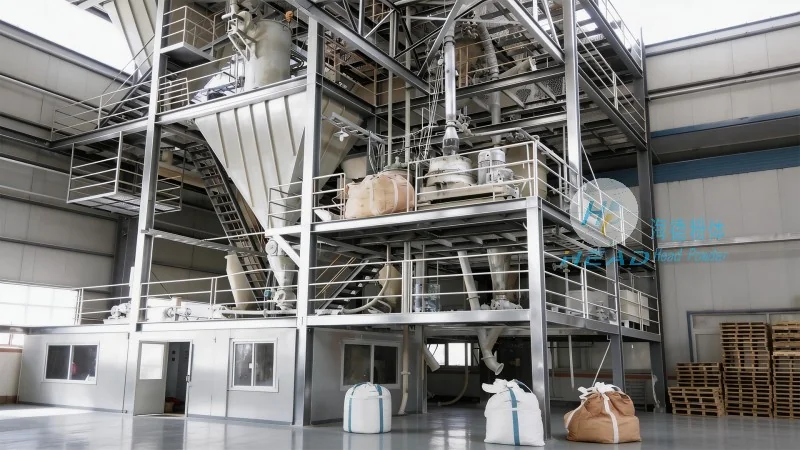
3. **Conveying and Transport**: The transport system uses various conveyor technologies, including belt conveyors, screw conveyors, and pneumatic conveying systems. For bulk transport over long distances, pneumatic conveying is often preferred due to its ability to handle fine powders without the need for mechanical contact. The system is designed to maintain the product's integrity, with minimal exposure to air and moisture to prevent degradation.
4. **Unloading and Distribution**: At the destination, the sodium bicarbonate is unloaded from the transport vessel into a receiving silo or directly into packaging equipment. The unloading process is automated to ensure accuracy and efficiency, with sensors monitoring the flow rate and level of the material. The distribution system ensures that the product is delivered to the end-users in the required form, whether as bulk or packaged goods.
Designing an effective transport system for sodium bicarbonate requires careful consideration of several engineering factors to ensure optimal performance and product quality. These considerations include material selection, equipment maintenance, and operational protocols.
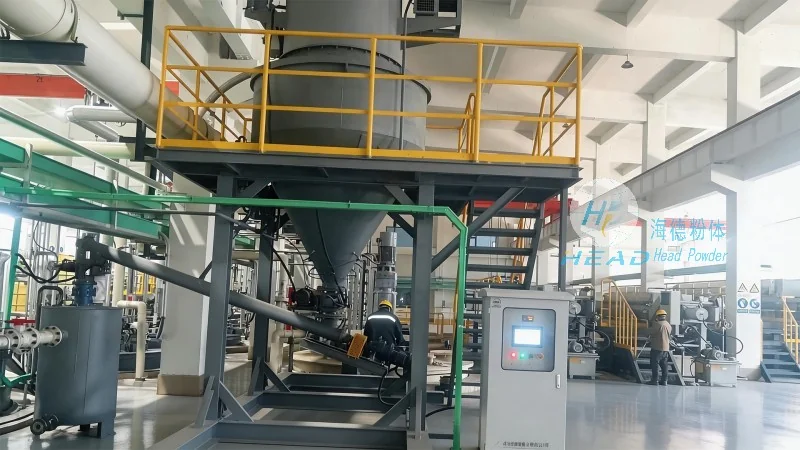
1. **Material Selection**: The equipment used in the transport system must be resistant to corrosion and chemical reactions with sodium bicarbonate. Stainless steel or specialized alloys are commonly used for hoppers, silos, and conveyor components to prevent contamination and ensure durability. The selection of materials also affects the system's longevity and maintenance costs.
2. **Equipment Maintenance**: Regular maintenance is crucial to prevent equipment failure and maintain the product's quality. This includes cleaning the conveyor belts, checking for wear and tear on bearings, and inspecting the aeration systems for blockages. Proper maintenance schedules help to minimize downtime and ensure consistent operation.
3. **Operational Protocols**: Standard operating procedures (SOPs) are established to guide the operation of the transport system. These protocols cover aspects such as start-up and shutdown procedures, material handling guidelines, and safety measures. Adherence to SOPs ensures that the system operates efficiently and safely, reducing the risk of accidents and product contamination.
Shandong HeadPowder Engineering Co., Ltd. provides comprehensive technical solutions for sodium bicarbonate, focusing on the precise control of technical parameters and the efficient design of transport systems. By adhering to industry standards and employing advanced engineering practices, the company ensures that sodium bicarbonate is handled and transported in a manner that maintains its quality and meets the requirements of various applications. The detailed understanding of technical parameters and transport processes is essential for optimizing the performance of sodium bicarbonate in industrial settings.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top