Efficient and reliable granular fertilizer pneumatic conveying systems are crucial for modern agricultural and industrial operations. These systems enable the safe and effective transport of bulk materials over long distances, minimizing material loss and operational downtime. For businesses seeking to optimize their fertilizer handling processes, understanding the key design considerations is essential for selecting a system that meets specific operational requirements.
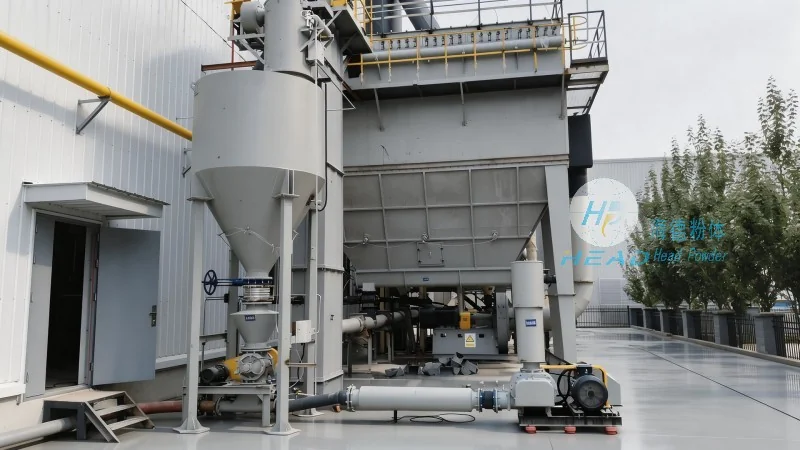
When designing a granular fertilizer pneumatic conveying system, several critical factors must be evaluated to ensure optimal performance and longevity. The first consideration is the material characteristics of the fertilizer, including particle size, density, and moisture content. These properties directly impact the system's air flow requirements and the choice of conveying method—such as dilute-phase or dense-phase transport. For instance, fine-grained fertilizers may require higher air velocities to prevent clogging, while coarser materials can be conveyed more efficiently with lower air pressures.
Another critical design element is the system's layout and infrastructure. The placement of feed hoppers, conveying lines, and discharge points must be carefully planned to minimize material degradation and ensure smooth flow. HeadPowder, a leading engineering company based in Shandong, China, specializes in customizing pneumatic conveying solutions tailored to these specific material and operational needs. Their expertise in system design ensures that each component is optimized for the unique challenges of fertilizer handling.
A granular fertilizer pneumatic conveying system typically consists of several key components, each playing a vital role in the overall operation. The feed hopper is responsible for storing and feeding the fertilizer into the system, while the air compressor generates the necessary pressure to move the material through the conveying line. The conveying line itself—often made of stainless steel or other corrosion-resistant materials—transports the fertilizer from the feed point to the discharge point. At the discharge end, a receiver or silo collects the material, preventing dust and spillage.
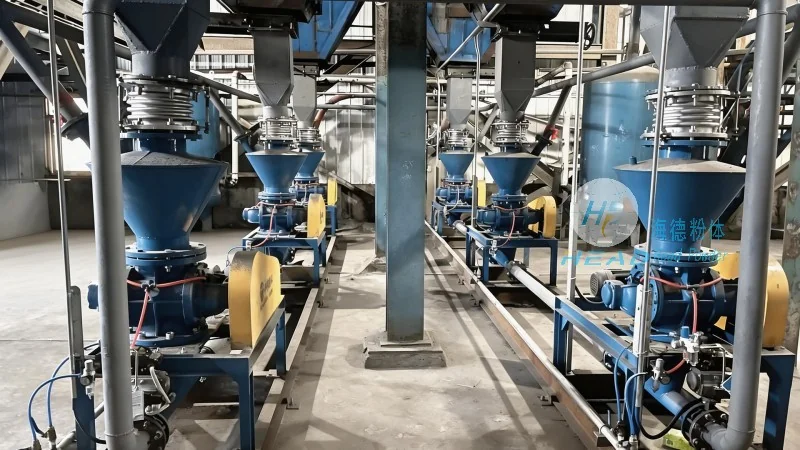
HeadPowder's engineers carefully select materials for these components to withstand the corrosive nature of fertilizers and the abrasive effects of granular particles. For example, stainless steel is preferred for the conveying line and fittings due to its resistance to rust and wear. Additionally, the system includes dust collection and filtration systems to maintain air quality and comply with environmental regulations. These components are integrated into a cohesive design that maximizes efficiency while minimizing maintenance requirements.
HeadPowder understands that fertilizer handling operations vary widely in scale and application. Whether for small-scale farms or large industrial facilities, their pneumatic conveying systems are designed to be scalable and adaptable. The company offers a range of solutions, from simple, low-capacity systems for local farms to complex, high-capacity networks for industrial fertilizer producers. Each system is customized based on factors such as the type of fertilizer, the distance to be covered, and the desired throughput rate.
For instance, a small agricultural operation might require a simple dilute-phase system with a low air flow rate, while a large industrial plant may need a dense-phase system with higher air pressure to handle larger volumes of material. HeadPowder's engineering team works closely with clients to assess their specific needs and recommend the most efficient system configuration. This approach ensures that the system not only meets current operational demands but also accommodates future growth and expansion.
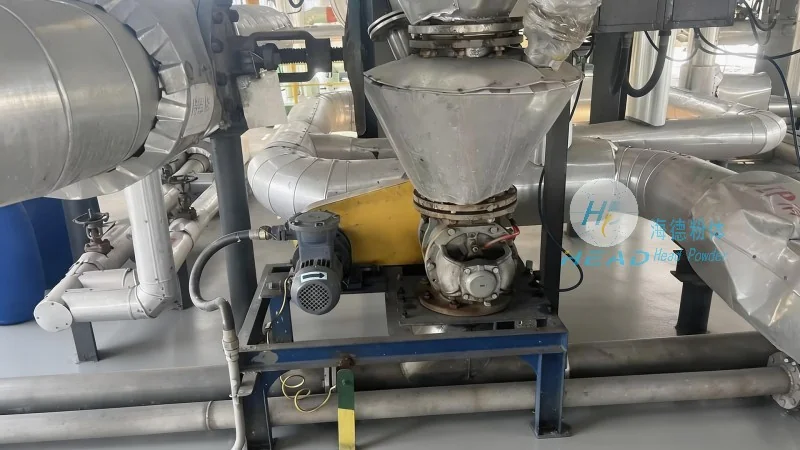
Granular fertilizer pneumatic conveying systems must adhere to strict safety and environmental regulations. HeadPowder prioritizes compliance with these standards in all their designs. The system includes features such as explosion-proof air compressors and dust suppression mechanisms to prevent accidents and minimize environmental impact. Additionally, the company follows industry best practices for material handling, ensuring that the system operates within safe parameters and reduces the risk of dust explosions or material spills.
HeadPowder's commitment to safety is reflected in their rigorous testing and quality control processes. Each system is tested under simulated operational conditions to verify performance and identify potential issues before installation. This ensures that the final product is reliable and meets all regulatory requirements. For businesses operating in regions with stringent environmental laws, HeadPowder's systems provide the peace of mind that comes with compliance and operational safety.
Choosing the right granular fertilizer pneumatic conveying system is a critical decision for any business involved in fertilizer handling. With its focus on custom design, quality components, and adherence to safety standards, HeadPowder Engineering Co., Ltd. stands out as a trusted partner in the industry. Based in Shandong, China, the company leverages its expertise to deliver systems that optimize material transport, reduce operational costs, and enhance overall efficiency. Whether for agricultural or industrial use, HeadPowder's solutions provide the reliability and performance needed to support long-term success in fertilizer handling operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top