When it comes to the efficient and reliable transport of bentonite—a crucial industrial material—pneumatic conveying systems have emerged as a highly effective solution. Bentonite, known for its unique properties such as high swelling capacity and excellent water retention, is widely used in various industries including construction, oil and gas, and environmental remediation. However, the challenges associated with handling this material, particularly its tendency to clog or degrade in traditional conveying methods, have led to the adoption of advanced pneumatic conveying technologies. This article explores the critical role of pneumatic conveying in bentonite transport, highlighting the benefits, technical considerations, and practical applications of this method.
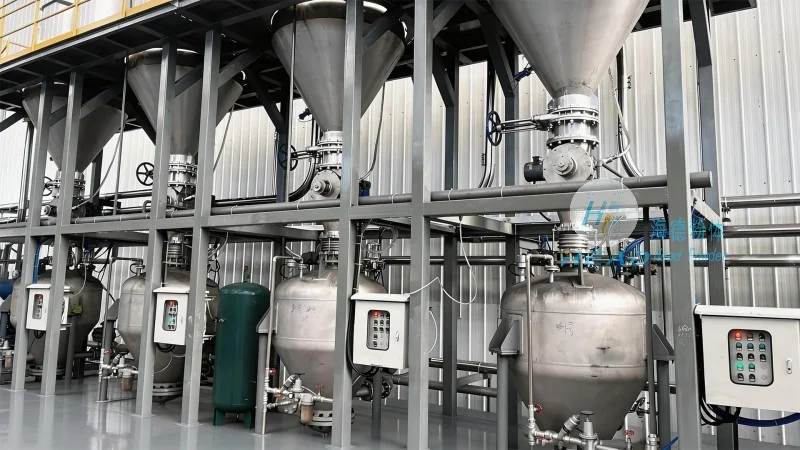
Bentonite is a type of clay composed primarily of montmorillonite, which gives it the ability to absorb water and expand significantly. This property makes it an essential additive in drilling muds, foundry sands, and as a binder in various industrial processes. However, its hygroscopic nature and fine particle size pose significant challenges during transport. Traditional methods like belt conveyors or screw conveyors often struggle with material buildup, clogging, and degradation due to friction and moisture exposure. These issues not only reduce operational efficiency but also increase maintenance costs and downtime. Recognizing these challenges, industries have turned to pneumatic conveying as a more robust alternative.
Pneumatic conveying uses compressed air or gas to transport bulk materials through a pipeline system. The process involves creating a pressure differential that moves the material from the source to the destination. There are two main types of pneumatic conveying: dilute phase and dense phase. Dilute phase systems use low air-to-material ratios, suitable for fine powders like bentonite, while dense phase systems employ higher air-to-material ratios to maintain material integrity and prevent segregation. The choice between these systems depends on the material's characteristics, distance of transport, and required flow rate.
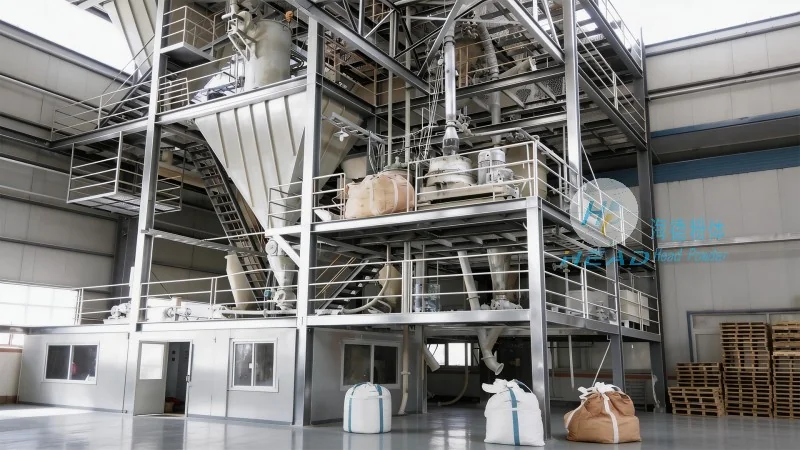
Implementing pneumatic conveying for bentonite transport offers several advantages over conventional methods. First, it eliminates the risk of clogging and material degradation, ensuring a consistent flow rate and product quality. The enclosed pipeline system also prevents contamination from external factors, maintaining the purity of the bentonite. Additionally, pneumatic conveying systems can handle high volumes of material with minimal labor, reducing operational costs and increasing productivity. Another key benefit is the ability to transport bentonite over long distances without the need for intermediate storage or transfer points, which is particularly valuable in large-scale industrial operations.
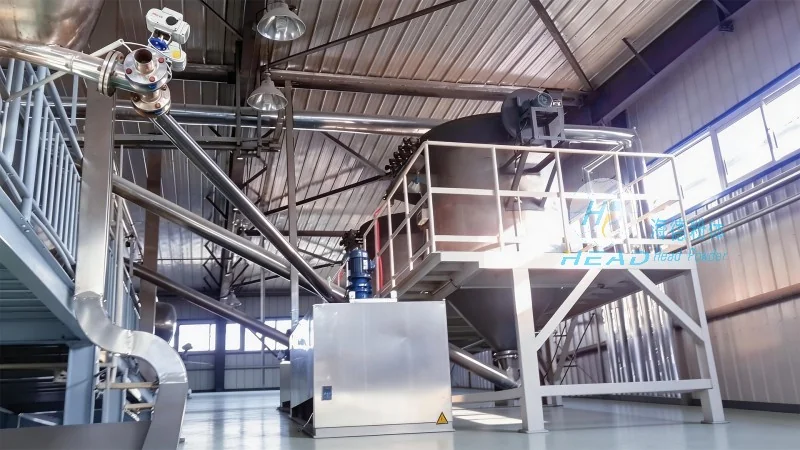
Successfully implementing pneumatic conveying for bentonite requires careful consideration of several technical factors. The first is the selection of the appropriate conveying system type, as mentioned earlier. For bentonite, dilute phase systems are often preferred due to their efficiency in handling fine powders. The pipeline design is also critical, with considerations for material flow, pressure drop, and equipment sizing. The use of appropriate air filters and moisture control systems is essential to prevent material degradation and ensure system longevity. Furthermore, regular maintenance and monitoring of the system are necessary to detect and address any issues promptly, such as clogging or air leaks, which can impact performance.
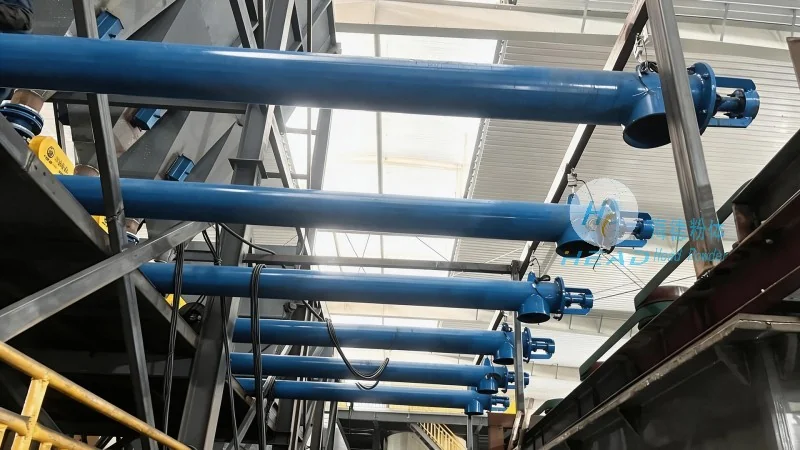
Pneumatic conveying is widely used in various applications involving bentonite transport. In the oil and gas industry, for example, bentonite is used as a component in drilling muds to maintain wellbore stability. Pneumatic conveying systems efficiently transport bentonite from storage silos to the drilling site, ensuring a steady supply of high-quality material. In the construction industry, bentonite is used as a binder in foundry sands and as a stabilizer in soil conditioning projects. Pneumatic conveying allows for the precise delivery of bentonite to these applications, maintaining the required consistency and reducing waste. Environmental remediation projects also benefit from pneumatic conveying, as it enables the transport of bentonite for soil stabilization and erosion control in contaminated sites.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of bulk material handling solutions, specializes in designing and manufacturing pneumatic conveying systems tailored to the needs of bentonite transport. With years of experience in the industry, the company has developed advanced systems that address the unique challenges of handling bentonite. Their solutions include customized pipeline designs, efficient air compression systems, and advanced control technologies that optimize material flow and minimize energy consumption. The company's commitment to quality and innovation has made it a trusted partner for industries relying on reliable bentonite transport. By leveraging their expertise, Shandong HeadPowder Engineering Co., Ltd. helps clients improve operational efficiency, reduce costs, and ensure the consistent quality of bentonite in their processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top