Wheat bran, a byproduct of the milling process, is often handled using pneumatic conveying systems to ensure efficient and safe material transport. This technology is crucial for industries that rely on wheat bran for various applications, such as animal feed, biofuel production, or industrial raw materials. Understanding the working principle and key characteristics of such systems is essential for optimizing operational efficiency and maintaining product quality.
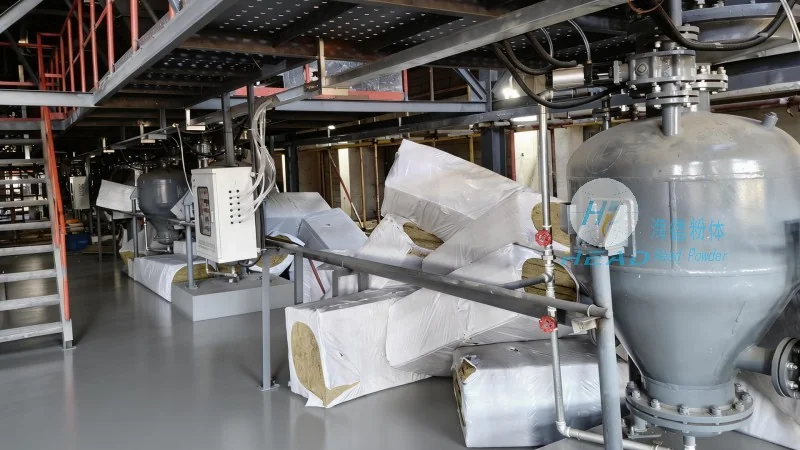
HeadPowder, a leading provider in the field of powder handling solutions, specializes in designing and manufacturing advanced pneumatic conveying systems tailored to the unique needs of industries dealing with bulk materials like wheat bran. With a focus on innovation and customer-centric solutions, the company has established itself as a trusted partner for businesses seeking reliable and efficient material transport solutions. HeadPowder's expertise lies in integrating cutting-edge technology with practical engineering to deliver systems that meet the highest standards of performance and durability.
Pneumatic conveying systems operate by using air or gas to transport dry bulk materials through a pipeline. In the case of wheat bran, the process typically involves a combination of positive and negative pressure systems. The working principle can be broken down into several key steps. First, the wheat bran is fed into a hopper or feeder, where it is then introduced into the conveying line. Air is then introduced into the system, either by creating a vacuum (negative pressure) or by blowing air into the line (positive pressure). This air flow creates a stream that carries the wheat bran particles through the pipeline to the destination point, such as a storage silo or processing unit. The system ensures that the material is transported without the need for mechanical components like belts or buckets, reducing maintenance requirements and minimizing the risk of contamination.
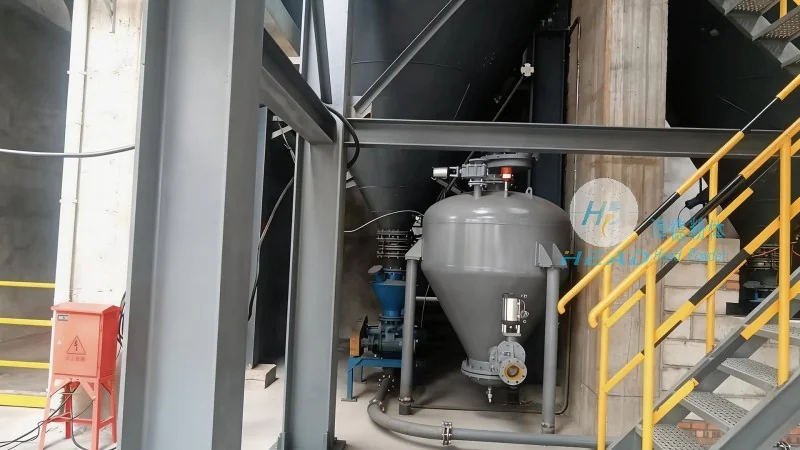
When considering pneumatic conveying for wheat bran powder, several important characteristics must be evaluated to ensure optimal performance. First, the system's capacity and flow rate are critical factors. The design must be able to handle the required volume of wheat bran while maintaining a consistent flow rate to avoid clogging or uneven distribution. Second, the system's pressure requirements are a key consideration. Different applications may require either low or high-pressure systems, and the choice depends on the distance to be covered and the material's properties. Third, the system's ability to handle varying particle sizes and moisture content is essential. Wheat bran can have a wide range of particle sizes, and the conveying system must be designed to handle these variations without causing blockages or degradation of the material. Fourth, the system's energy efficiency is an important factor for long-term operational costs. Advanced systems use energy-saving technologies, such as variable frequency drives, to optimize air usage and reduce power consumption. Finally, the system's reliability and durability are crucial for continuous operation in industrial settings. High-quality materials and robust construction ensure that the system can withstand the demands of daily use and maintain performance over time.
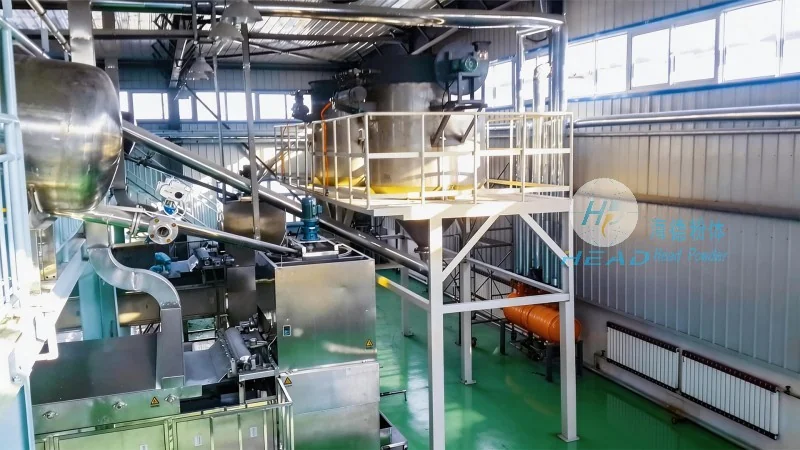
Implementing pneumatic conveying systems for wheat bran offers several significant advantages over traditional mechanical conveying methods. One of the primary benefits is the reduction in material handling costs. By eliminating the need for multiple transfer points and mechanical components, the system reduces labor and maintenance expenses. Additionally, pneumatic conveying minimizes product contamination, as the material is enclosed within the pipeline, preventing exposure to dust, moisture, or other contaminants. This is particularly important for wheat bran, which is often used in food and animal feed applications where purity is essential. Another advantage is the improved safety and hygiene. The enclosed system reduces the risk of dust explosions and improves working conditions by containing dust and preventing it from entering the workspace. Furthermore, pneumatic conveying allows for flexible and scalable solutions. The system can be easily expanded or modified to accommodate changes in production volume or process requirements, providing long-term flexibility. Finally, the system's ability to handle a wide range of particle sizes and moisture content makes it suitable for various applications, from small-scale operations to large industrial facilities.
Pneumatic conveying systems are widely used in the handling of wheat bran for various applications. For example, in animal feed production, the system can transport wheat bran from storage silos to mixing facilities, ensuring a consistent and uniform feed blend. In biofuel production, the system can move wheat bran to processing units where it is converted into ethanol or other biofuels. In industrial applications, the system can transport wheat bran to manufacturing processes where it is used as a raw material for products like paper or plastics. When operating a pneumatic conveying system for wheat bran, several considerations are important to ensure optimal performance. First, the system must be designed to handle the specific properties of wheat bran, such as its density, moisture content, and particle size distribution. Second, regular maintenance is crucial to prevent clogging and ensure consistent performance. This includes cleaning the pipeline, checking for air leaks, and replacing worn components. Third, the system's control system must be reliable and easy to operate, allowing for adjustments to flow rate and pressure as needed. Finally, safety measures must be in place to prevent dust explosions and protect workers from dust exposure. Proper ventilation and explosion-proof components are essential for safe operation.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top