Chocolate powder, as a critical ingredient in the confectionery sector, demands efficient and reliable handling to preserve product quality and maintain process stability. Pneumatic conveying, a technology that utilizes air to transport bulk materials, has emerged as a preferred solution for chocolate powder due to its advantages in hygiene, speed, and adaptability. This article delves into the working principle and key characteristics of chocolate powder pneumatic conveying, offering insights into how this technology functions and its benefits in industrial applications.
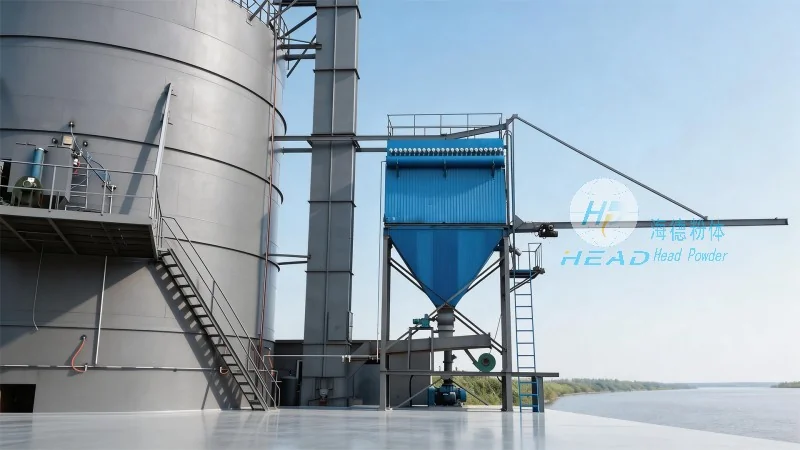
The fundamental mechanism of chocolate powder pneumatic conveying involves compressed air to move powder particles through a pipeline system. The process typically includes essential components: a material hopper for storage, a feeder to regulate flow rates, a conveying line with appropriate ductwork, and a dust collector or filter to capture airborne particles. When activated, compressed air is introduced into the conveying line, creating a pressure differential that propels chocolate powder from the hopper to the destination—such as a silo, storage tank, or processing equipment.
Two primary types of pneumatic conveying systems are employed for chocolate powder: dilute-phase and dense-phase. Dilute-phase systems operate at higher air velocities (20-30 m/s) and are suitable for short distances (up to several hundred meters). In this mode, powder particles are suspended in the air stream and move rapidly through the pipeline. Dense-phase systems, conversely, use lower air velocities (5-15 m/s) and higher powder concentrations, making them ideal for longer distances (up to several kilometers) and delicate materials like chocolate powder, which can agglomerate or be damaged by excessive force.
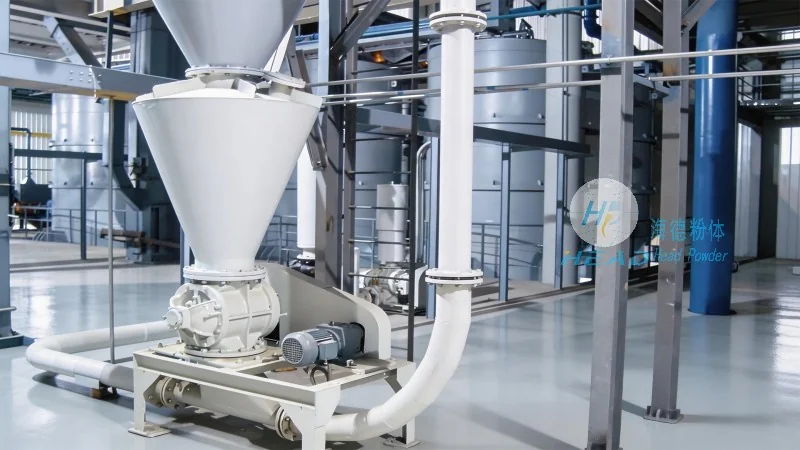
Several distinct characteristics make chocolate powder pneumatic conveying an attractive option for manufacturers. First, it delivers high efficiency in material transport, moving large volumes quickly with minimal downtime. This reduces labor costs and boosts production throughput. Second, the technology ensures excellent hygiene and cleanliness, critical in the food industry. The enclosed pipeline system prevents external contamination and minimizes dust exposure, keeping chocolate powder free from impurities and maintaining quality throughout the process.
Another notable characteristic is system flexibility. Pneumatic conveying can be easily integrated with existing production lines, allowing modular expansion or reconfiguration as needs change. The system can transport chocolate powder to multiple destinations from a single source or vice versa, adapting to various production layouts. Additionally, it requires relatively low maintenance compared to belt or screw conveyors, with fewer moving parts and less frequent cleaning.
Implementing chocolate powder pneumatic conveying offers practical benefits. The system preserves product integrity, crucial for chocolate powder sensitive to moisture, temperature, and mechanical stress. Enclosed transport and controlled air flow help maintain texture and flavor. Furthermore, it reduces cross-contamination between batches, as each pipeline can be dedicated to a specific product or ingredient.
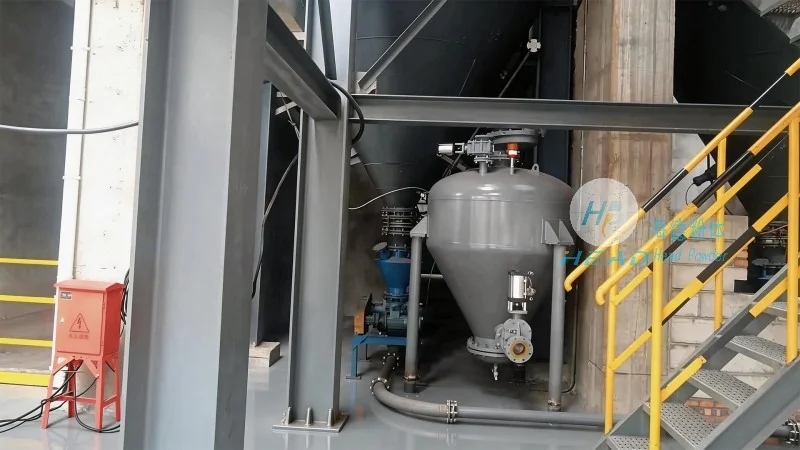
However, considerations include higher initial investment for the compressor, ductwork, and control equipment compared to other methods. Regular maintenance, such as filter cleaning and pressure checks, is required. Proper system design and sizing are vital to avoid clogging or excessive energy use, impacting long-term costs.
Chocolate powder pneumatic conveying is a sophisticated and effective technology addressing the unique challenges of handling delicate food powders like chocolate. By understanding its working principle and characteristics, manufacturers can make informed decisions about integrating this system into their processes. The combination of efficiency, hygiene, and flexibility makes pneumatic conveying a valuable asset for the confectionery industry, ensuring consistent product quality and operational success.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top