For industrial applications requiring efficient and reliable powder handling, bulk bag pneumatic conveying systems offer a versatile solution. This technology is particularly suited for transporting bulk materials in various industries such as food, pharmaceuticals, chemicals, and construction. Understanding the working principle and key characteristics of these systems is essential for selecting the right equipment for specific operational needs.
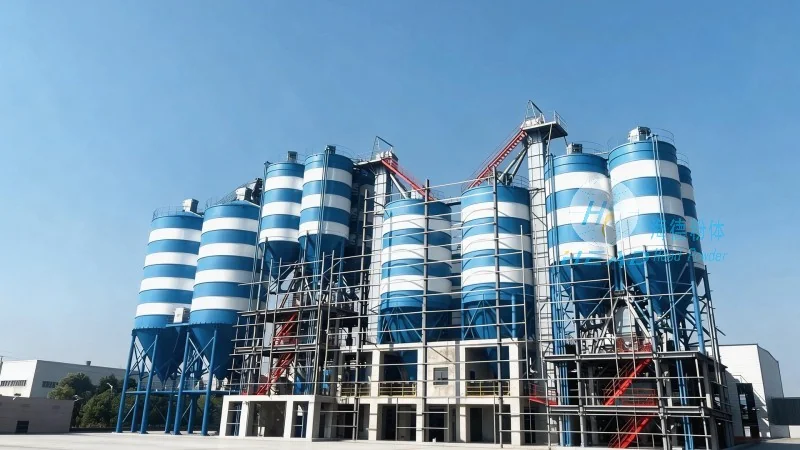
HeadPowder, a leading provider in the field, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying solutions. With a strong presence in China, particularly in Shandong, the company leverages over a decade of expertise to deliver customized systems that meet stringent industry standards. The company's commitment to quality and innovation ensures that clients receive equipment that is both efficient and durable.
The core mechanism of bulk bag pneumatic conveying involves the use of air to transport dry powder materials from a storage container, typically a bulk bag or tote, to a processing unit. The process begins with the material being discharged from the bulk bag into a hopper or feeder. A blower or compressor then generates a flow of air, which creates a low-pressure or high-pressure environment depending on the system design. This airflow draws the powder particles into the conveying line, where they are carried to the destination point. The system typically includes components such as a hopper, a feeder, a filter, and a receiver, all working in tandem to ensure smooth material transfer.
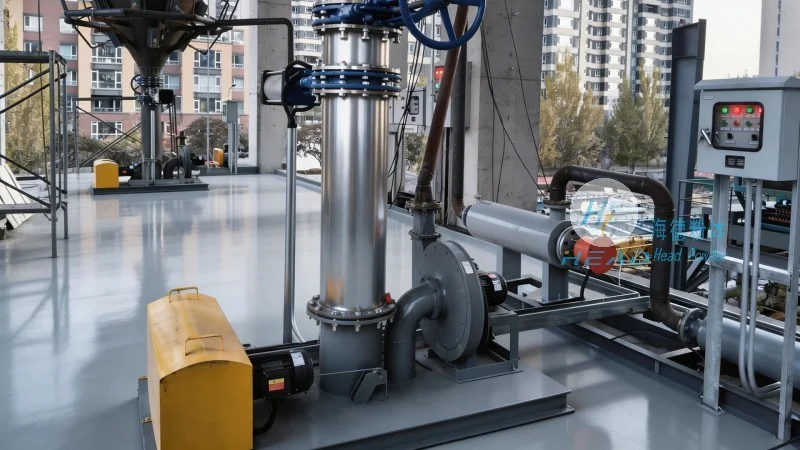
Several distinct characteristics define bulk bag pneumatic conveying systems, making them advantageous for various applications. Firstly, the system is highly flexible, allowing for the transport of materials over long distances and varying elevations. This adaptability is crucial for industrial settings where material locations may be spread out or require vertical movement. Secondly, the technology offers excellent material containment, minimizing dust emissions and ensuring compliance with environmental regulations. The enclosed system design prevents particle loss and reduces the risk of contamination, which is critical in industries like food and pharmaceuticals where product purity is paramount.
Another significant characteristic is the ability to handle a wide range of powder properties. From fine powders to coarse granules, the system can accommodate diverse material types without compromising performance. This versatility makes it suitable for applications involving different particle sizes, densities, and flow characteristics. Additionally, the system operates with minimal maintenance requirements, as the components are designed to withstand the rigors of continuous operation. The use of robust materials and efficient filtration systems ensures long-term reliability, reducing downtime and operational costs.
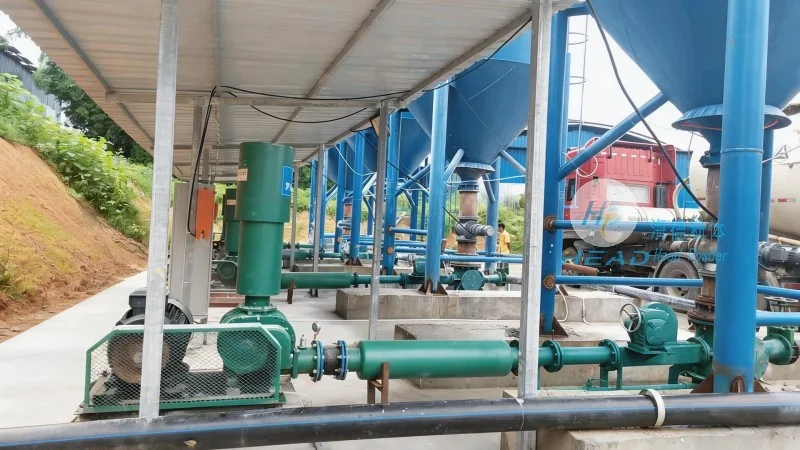
Bulk bag pneumatic conveying systems provide several advantages that enhance operational efficiency and product quality. The enclosed nature of the system reduces the risk of cross-contamination, which is vital in industries where product integrity is non-negotiable. By maintaining a clean environment, the system helps preserve the quality of the powder, extending shelf life and ensuring consistent performance. Furthermore, the system's ability to handle large volumes of material in a short period improves production throughput, allowing businesses to meet demand more effectively.
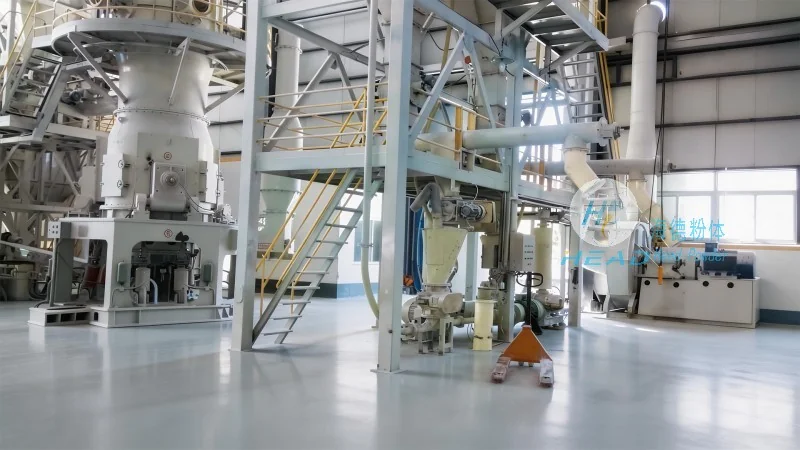
Cost-effectiveness is another key benefit. Compared to traditional methods like belt conveyors or manual handling, pneumatic conveying reduces labor costs and material handling time. The automated process minimizes human intervention, leading to lower operational expenses and increased productivity. Additionally, the system's energy efficiency, particularly with modern blower designs, contributes to lower utility costs over time. This makes it an economically viable option for both new installations and retrofitting existing facilities.
Bulk bag pneumatic conveying systems represent a sophisticated solution for efficient powder handling in industrial settings. By understanding the working principle and leveraging the key characteristics of these systems, businesses can optimize their material transport processes. HeadPowder, with its expertise and commitment to quality, continues to provide tailored solutions that meet the evolving needs of various industries. The technology's adaptability, reliability, and cost-effectiveness make it a preferred choice for companies seeking to enhance their operational efficiency and product quality.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top