For industrial applications requiring precise and consistent material handling, continuous quantitative material conveying systems offer efficient solutions. These systems are designed to transport bulk materials in a controlled manner, ensuring accurate measurement and delivery. Understanding the working principle and key features of such systems is crucial for selecting the right equipment for specific operational needs.
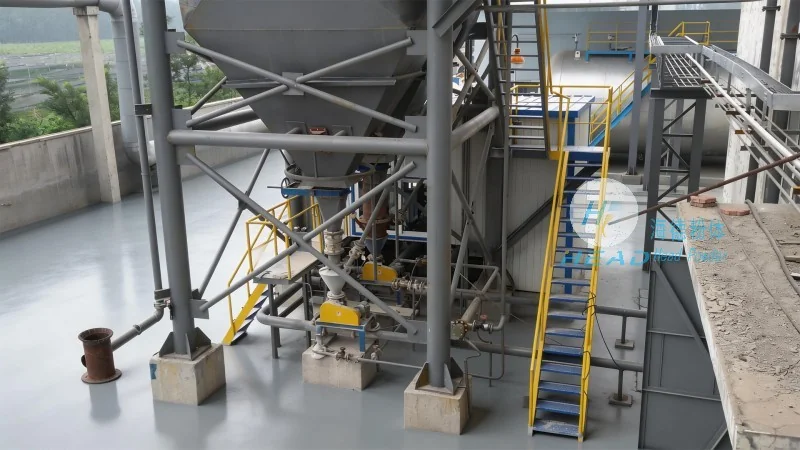
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in the design, development, and production of advanced material handling equipment. With a strong commitment to quality and innovation, HeadPowder has established itself as a trusted partner in the industry, providing reliable solutions for various material conveying challenges. HeadPowder is headquartered in Shandong, China, where the company leverages its expertise to deliver cutting-edge technology tailored to global market demands.
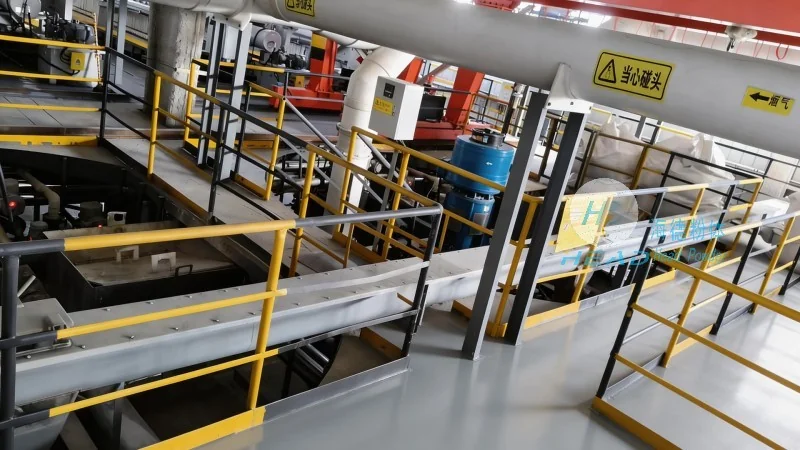
Continuous quantitative material conveying systems operate on a principle of precision and automation, ensuring that bulk materials are transported and measured with high accuracy. The core components typically include a conveyor mechanism, a dosing or metering device, and control systems that work in tandem to achieve consistent output. The conveyor system moves the material continuously, while the dosing unit measures and releases the material in precise quantities. Advanced control systems, often equipped with sensors and feedback mechanisms, adjust the flow rate in real-time to maintain the desired output. This integrated approach ensures that the system can handle a wide range of materials, from powders and granules to bulk solids, with minimal variation in quantity. The process begins with the material being fed into the conveyor, where it is transported to the dosing point. The dosing device then calculates the required volume based on preset parameters, such as flow rate, material density, and target output. By continuously monitoring the material flow and adjusting the conveyor speed or dosing rate, the system maintains a stable and accurate delivery. This method is particularly effective for applications where uniform material distribution is critical, such as in pharmaceuticals, food processing, and chemical manufacturing.
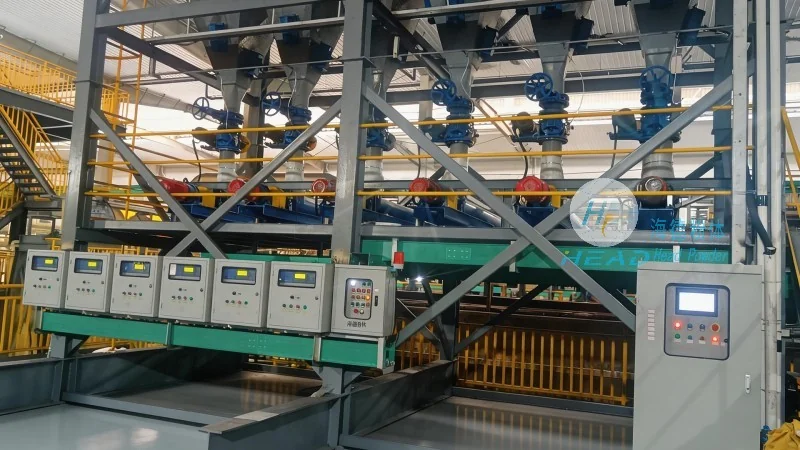
Continuous quantitative material conveying systems are characterized by several distinct features that enhance their performance and usability. One of the primary features is the ability to deliver materials in precise, repeatable quantities, which is essential for applications requiring strict dosage control. The systems are equipped with advanced control technology, including programmable logic controllers (PLCs) and digital displays, allowing operators to set and adjust parameters easily. This flexibility enables the system to adapt to different material types and processing requirements without significant modifications. Another notable feature is the continuous operation capability, which ensures a steady flow of material without interruptions. Unlike batch processing systems, continuous conveyors maintain a consistent output, reducing downtime and increasing overall productivity. The systems also incorporate safety features, such as emergency stop buttons and overload protection, to ensure safe operation in industrial environments. Additionally, many modern systems are designed with modular components, allowing for easy maintenance and replacement of parts. This modularity enhances the system's longevity and reduces maintenance costs over time. The integration of sensors and feedback loops further enhances the system's accuracy, as real-time data is used to adjust the conveying process dynamically. This closed-loop control system minimizes errors and ensures that the output remains within the desired tolerance range. Furthermore, the systems are often designed to be compatible with various downstream equipment, such as mixers, packers, or processing units, facilitating seamless integration into existing production lines.
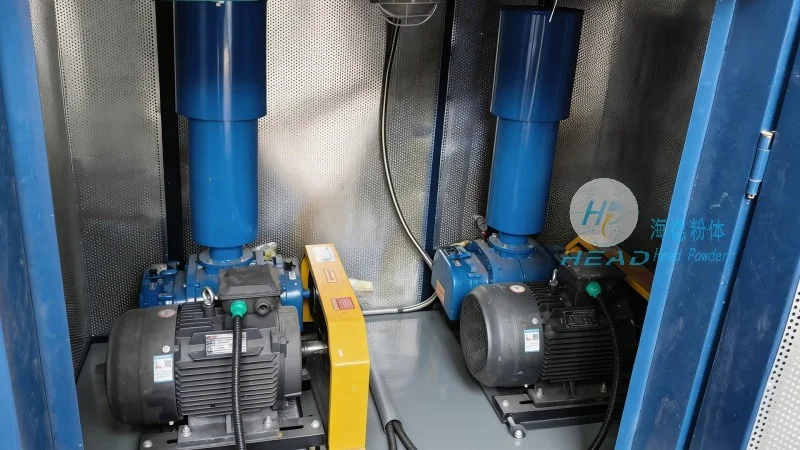
The continuous quantitative material conveying systems offered by Shandong HeadPowder Engineering Co., Ltd. provide numerous advantages for industrial operations. The primary benefit is the high level of accuracy and consistency in material delivery, which is critical for processes where precise dosing is required. This accuracy reduces waste and improves product quality, leading to cost savings and increased efficiency. The systems are also designed for high reliability, with robust construction and durable components that can withstand harsh industrial conditions. This durability ensures long-term performance and minimal downtime, contributing to overall operational stability. The continuous operation capability of these systems enhances productivity by maintaining a steady flow of material, eliminating the need for frequent stops and starts. This is particularly beneficial in high-volume production environments where continuous operation is essential. Additionally, the systems are user-friendly, with intuitive control interfaces that allow operators to monitor and adjust settings easily. This ease of use reduces training time and operational complexity, making the systems suitable for a wide range of users. The applications of these systems are diverse, spanning industries such as pharmaceuticals, food and beverage, chemicals, and mining. In pharmaceutical manufacturing, the systems are used to deliver raw materials with strict dosage requirements, ensuring compliance with regulatory standards. In food processing, they are employed to handle ingredients like powders and granules, maintaining consistent product quality. In chemical industries, the systems are used to transport bulk chemicals, ensuring safe and accurate handling. In mining operations, they are utilized to convey raw materials from storage to processing units, improving material flow and efficiency. Overall, the continuous quantitative material conveying systems from HeadPowder are designed to meet the demanding needs of modern industrial applications, providing reliable, accurate, and efficient material handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top