HeadPowder Engineering Co., Ltd. specializes in the design and manufacturing of advanced pneumatic conveying systems tailored for the sugar industry. This article provides an in-depth look at the key aspects of designing efficient sugar pneumatic conveying equipment, emphasizing the technical considerations and practical solutions that ensure optimal performance in sugar processing operations.
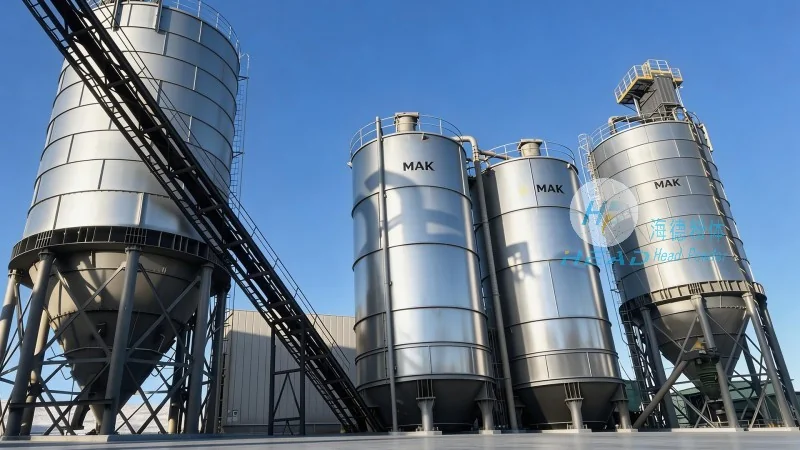
Pneumatic conveying is a critical technology in the sugar industry, enabling the safe and efficient transport of granular or powdered sugar from one location to another. Unlike traditional mechanical conveyors, pneumatic systems use air or other gases to move materials, reducing the risk of contamination and minimizing the need for physical contact with the product. This method is particularly advantageous in sugar processing, where maintaining product purity and preventing moisture absorption are paramount.
When designing a sugar pneumatic conveying system, several factors must be carefully evaluated to ensure reliability and efficiency. First, the material characteristics of the sugar, such as particle size, density, and moisture content, play a crucial role in determining the appropriate conveying method. For instance, fine granulated sugar may require a higher air velocity to prevent blockages, while larger crystals might benefit from a lower velocity to maintain flow stability. Additionally, the system's capacity and the distance over which the sugar needs to be transported are critical parameters that influence the selection of equipment components, including the type of air mover, the size of the conveying line, and the design of the feed and discharge mechanisms.
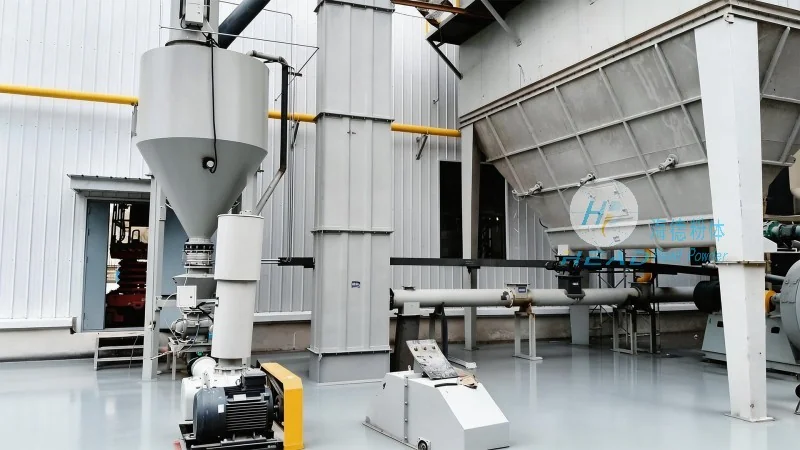
A standard sugar pneumatic conveying system typically consists of several key components, each playing a vital role in the overall operation. The primary components include an air mover (such as a rotary lobe blower or a positive displacement blower), a conveying line (often made of stainless steel to resist corrosion from sugar and moisture), a feed hopper (designed to handle the sugar feed without causing clogging), and a discharge valve or receiver. The air mover provides the necessary pressure and airflow to transport the sugar particles, while the conveying line ensures the material moves smoothly from the feed point to the discharge point. The feed hopper is equipped with a metering device, such as a rotary valve or a screw feeder, to control the flow rate of the sugar into the system. The discharge mechanism, which may include a cyclone separator or a filter, separates the sugar from the air and directs it to the final storage or processing location.
Implementing a pneumatic conveying system for sugar transport offers numerous benefits that enhance operational efficiency and product quality. One of the most significant advantages is the ability to maintain a closed system, which prevents the sugar from being exposed to contaminants or moisture from the environment. This is particularly important in food processing, where product purity is a top priority. Additionally, pneumatic systems can handle a wide range of sugar types, from raw sugar crystals to refined powdered sugar, without causing degradation or loss of quality. The flexibility of pneumatic conveying also allows for easy integration with existing processing lines, reducing the need for extensive modifications to the facility. Furthermore, these systems are generally more energy-efficient compared to traditional mechanical conveyors, as they can transport materials over longer distances with less power consumption.
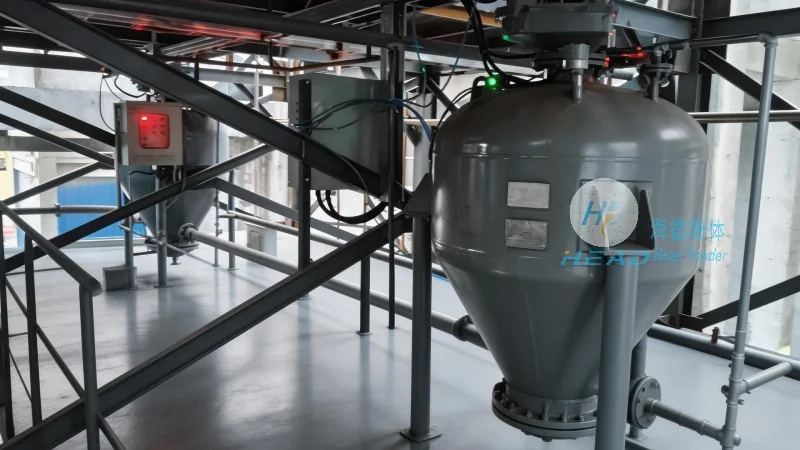
HeadPowder Engineering Co., Ltd. specializes in providing customized pneumatic conveying solutions tailored to the specific needs of sugar processing facilities. Our team of experienced engineers works closely with clients to understand their operational requirements, including the type of sugar being processed, the desired capacity, and the distance of transport. Based on this information, we design and manufacture systems that meet the highest standards of efficiency, reliability, and safety. Our solutions are designed to handle the unique challenges of sugar processing, such as the risk of clogging, the need for gentle handling to preserve product quality, and the requirement for easy maintenance and cleaning. We use high-quality materials, such as stainless steel, to ensure the equipment is durable and resistant to corrosion from sugar and moisture. Our systems are also equipped with advanced control systems that allow for precise monitoring and adjustment of the conveying process, ensuring optimal performance and minimizing downtime.
Designing an effective sugar pneumatic conveying system requires a deep understanding of both the material being transported and the operational requirements of the sugar processing facility. By carefully considering factors such as material characteristics, system capacity, and environmental conditions, engineers can develop systems that provide reliable, efficient, and safe transport of sugar. HeadPowder Engineering Co., Ltd. is committed to delivering innovative and customized solutions that meet the needs of the sugar industry, helping facilities improve their operational efficiency and maintain the highest standards of product quality.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top