Desulfurization and dust removal ash material conveying systems are critical components in industrial facilities that employ flue gas treatment technologies. These systems are designed to handle the byproducts generated during the desulfurization and dust removal processes, ensuring efficient and safe transport of ash materials from the treatment units to disposal or recycling sites. The following sections will explore the working principle and key characteristics of such conveying systems, providing insights into their operational mechanisms and advantages.
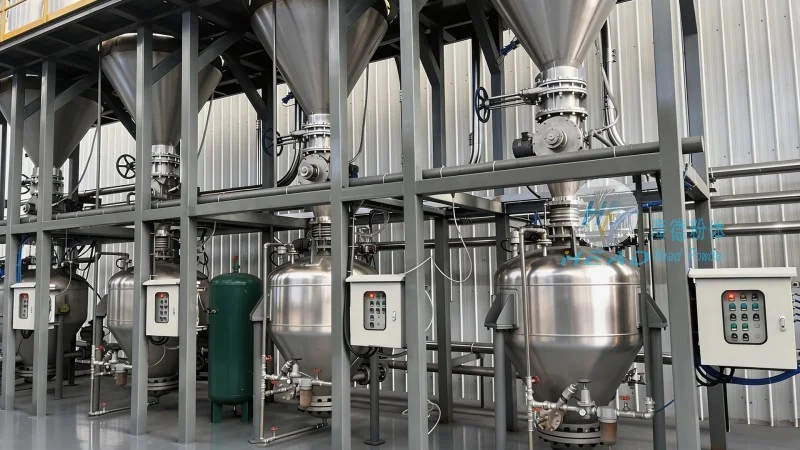
The core working principle of desulfurization and dust removal ash material conveying systems revolves around the integration of several key components, including ash collection devices, conveying mechanisms, and control systems. The process typically begins with the collection of ash from the desulfurization and dust removal units, such as wet or dry scrubbers, electrostatic precipitators, or bag filters. Once collected, the ash is transferred to a storage hopper or silo, where it is then fed into the conveying system.
Conveying mechanisms commonly used in these systems include pneumatic conveying (air-suspended transport), mechanical conveying (e.g., screw conveyors, belt conveyors), and hybrid systems that combine both pneumatic and mechanical components. Pneumatic conveying, for instance, utilizes compressed air to lift and transport ash particles through a pipeline network. The ash is suspended in the air stream and directed to the discharge point, such as a storage silo or a disposal site. Mechanical conveyors, on the other hand, rely on rotating components like screws or belts to move the ash along a fixed path, providing a more direct and contact-based transport method.
Control systems play a vital role in regulating the flow of ash and ensuring the smooth operation of the conveying process. Sensors and monitoring devices are integrated to detect ash levels, pressure variations, and system performance, allowing for real-time adjustments and maintenance. This automation enhances operational efficiency and minimizes downtime, ensuring consistent performance of the ash conveying system.
Desulfurization and dust removal ash material conveying systems exhibit several distinct characteristics that make them suitable for industrial applications. One of the primary advantages is their ability to handle high-volume ash flows with minimal operational complexity. These systems are designed to process large quantities of ash generated from continuous flue gas treatment operations, ensuring that the material is transported efficiently without causing blockages or system failures.
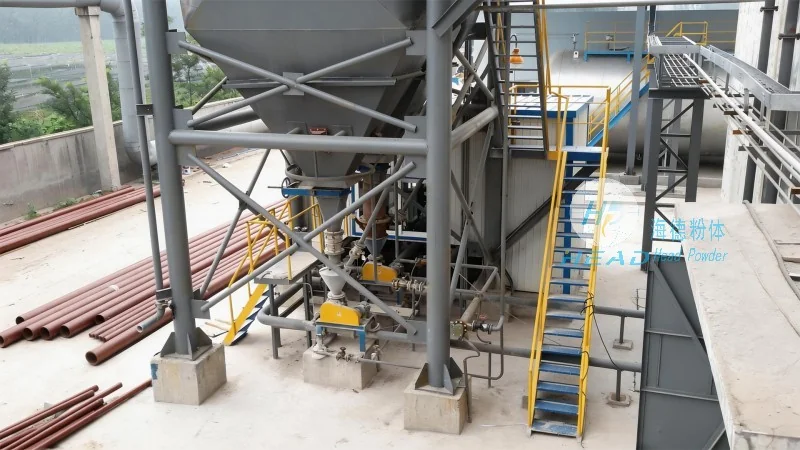
Another notable characteristic is the system's adaptability to different ash types and moisture content. Whether dealing with dry or wet ash, the conveying mechanisms are engineered to accommodate varying particle sizes and physical properties. This flexibility allows facilities to use the same conveying system for different treatment processes, reducing the need for multiple specialized equipment and lowering operational costs.
Environmental considerations are also a key characteristic of these systems. By ensuring that ash is transported safely and without releasing pollutants into the environment, the systems contribute to overall environmental compliance. The enclosed conveying pipelines and controlled discharge points minimize dust emissions and prevent contamination of surrounding areas, aligning with regulatory standards for industrial waste management.
Efficiency and reliability are further hallmarks of desulfurization and dust removal ash material conveying systems. Advanced control technologies and robust mechanical components ensure consistent performance, even under varying operational conditions. This reliability is crucial for maintaining the continuous operation of flue gas treatment plants, as any disruption in ash transport can impact the overall effectiveness of the desulfurization and dust removal processes.
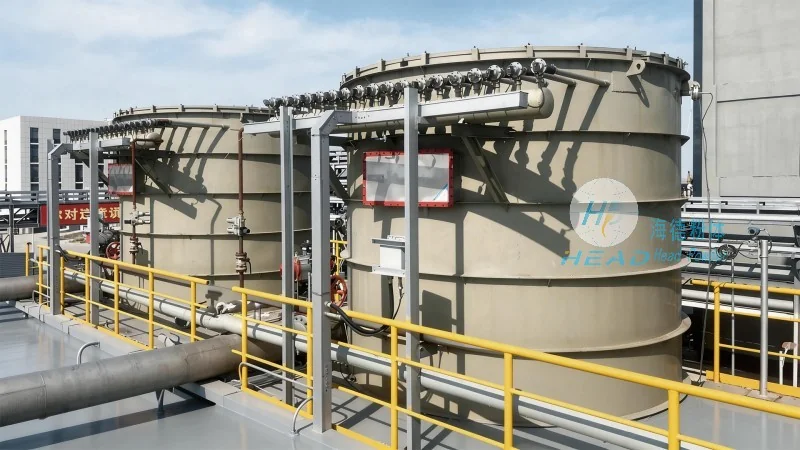
Desulfurization and dust removal ash material conveying systems are widely used in power plants, industrial boilers, and other facilities that rely on flue gas treatment to meet environmental regulations. The systems are essential for managing the byproducts of sulfur dioxide (SO₂) removal and particulate matter (PM) control, which are critical for reducing air pollution and complying with national and international environmental standards.
In power plants, for example, these systems transport ash from wet limestone scrubbers or dry sorbent injection systems to storage or disposal sites. The efficient conveyance of ash ensures that the treatment process remains uninterrupted, allowing the plant to continue generating electricity while maintaining compliance with emissions limits. Similarly, in industrial manufacturing facilities, such as cement plants or steel mills, ash conveying systems are integral to the overall waste management strategy, enabling the recycling or safe disposal of treated ash materials.
The systems also contribute to cost-effectiveness by optimizing the use of resources and reducing operational overhead. By minimizing downtime and maximizing throughput, facilities can achieve better economic performance while adhering to environmental requirements. This balance between efficiency and compliance makes desulfurization and dust removal ash material conveying systems a vital investment for industrial operations.
Desulfurization and dust removal ash material conveying systems are sophisticated solutions that address the challenges of handling and transporting ash generated from flue gas treatment processes. Through their integrated design and advanced control technologies, these systems ensure efficient, reliable, and environmentally responsible transport of ash materials. As industrial facilities continue to prioritize environmental compliance and operational efficiency, the importance of such conveying systems will only grow, making them a key component in modern industrial infrastructure.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top