Urea material pneumatic conveying is a critical industrial process used for transporting urea, a vital fertilizer and chemical compound, from one location to another. This method involves using a stream of air or other gas to move urea particles through a pipeline system. The technology is widely adopted in the fertilizer industry due to its efficiency, flexibility, and ability to handle bulk materials safely and effectively.
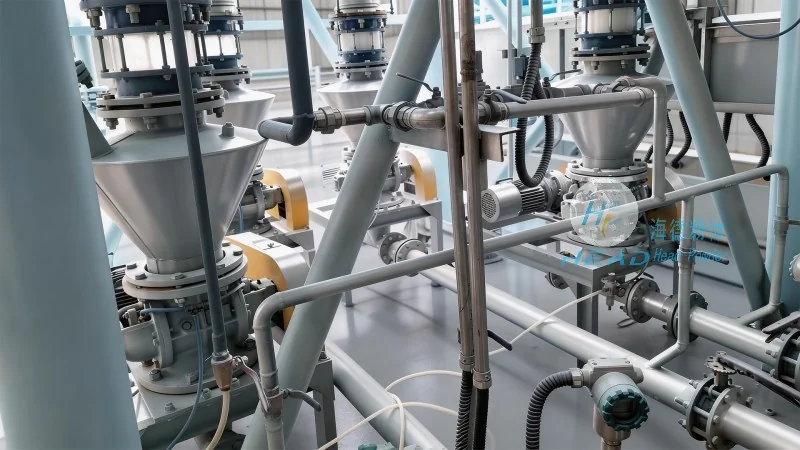
HeadPowder, a leading provider of engineering solutions, specializes in designing and implementing pneumatic conveying systems tailored for urea and other bulk materials. With headquarters in Shandong, China, the company leverages decades of experience to deliver reliable and efficient solutions for clients across the global fertilizer sector.
Pneumatic conveying systems for urea typically consist of several key components, including a hopper for material storage, a feeder to control the flow rate, a conveying line (often made of stainless steel or other corrosion-resistant materials), and a receiver for the discharged material. The system operates by creating a pressure differential: either positive pressure (where air is forced through the pipeline) or negative pressure (where air is drawn out, creating a vacuum). In the case of urea, positive pressure systems are more common due to the material's properties and the need for consistent flow.
The process begins when urea is fed from the hopper into the conveying line. The feeder ensures a steady flow, preventing blockages or uneven material distribution. As the material enters the pipeline, it is entrained by the moving air, which carries the urea particles through the system. The air velocity must be sufficient to keep the particles suspended and prevent settling or clogging. The receiver at the end of the line collects the urea, which is then discharged for further processing or storage.
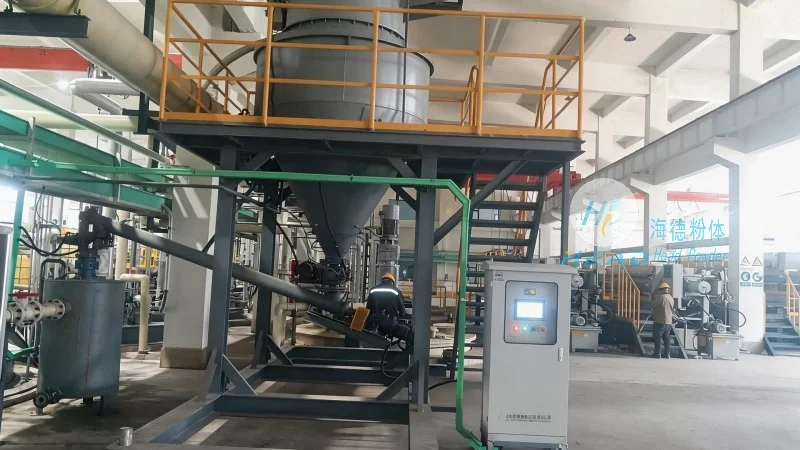
Designing an effective urea pneumatic conveying system requires careful consideration of several factors to ensure optimal performance, safety, and longevity. Key design principles include:
Material Handling Requirements: Urea is a hygroscopic material, meaning it absorbs moisture from the air. This property necessitates the use of dry, filtered air to prevent clumping or degradation. The system must also account for urea's density and particle size distribution, as these affect the required air velocity and pressure. For example, finer urea particles may require higher air speeds to maintain suspension.
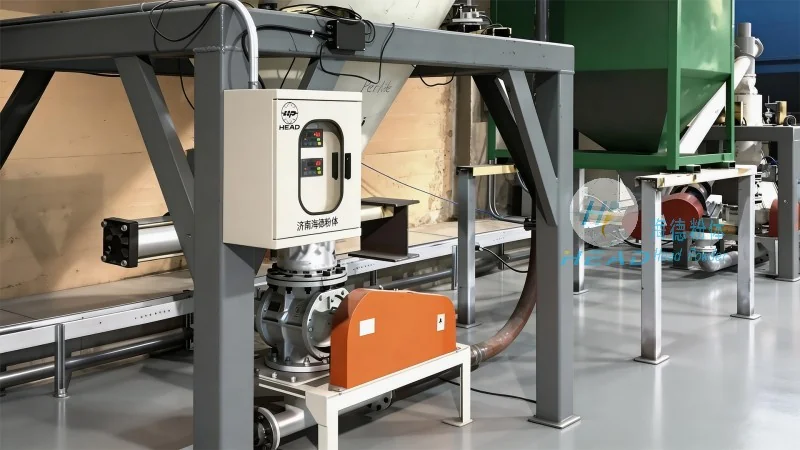
System Configuration: The choice between positive and negative pressure systems depends on the application and distance of material transport. Positive pressure systems are suitable for short to medium distances and can handle vertical lifts, while negative pressure systems are better for longer horizontal runs or when the material needs to be transported from a higher to a lower elevation. The design also considers the number of turns, bends, and fittings in the pipeline, as these can increase pressure drop and affect system efficiency.
Equipment Selection: Components such as hoppers, feeders, and receivers must be designed to handle urea's characteristics. Hoppers are often equipped with agitators or vibrators to prevent material bridging or caking. Feeders, like rotary valves or screw conveyors, ensure consistent material flow without causing excessive wear. Receivers are typically equipped with dust collection systems to control emissions and maintain air quality.
Pressure and Flow Management: Proper control of air pressure and flow rate is critical to prevent material degradation or system failure. The system must be designed to maintain a consistent pressure differential, which ensures that urea particles remain suspended and do not settle in the pipeline. Pressure drop calculations are essential to determine the appropriate air velocity and system capacity. For instance, a higher air velocity may be needed for longer pipelines or when transporting larger particle sizes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top