When discussing material handling and processing, the pneumatic conveying of magnesium sulfate stands out as a critical method for efficient and reliable transport. This technique involves using a stream of gas, typically air, to move bulk materials like magnesium sulfate through a pipeline system. As a key component in various industrial applications, understanding the principles behind this process is essential for optimizing operations and ensuring safety.
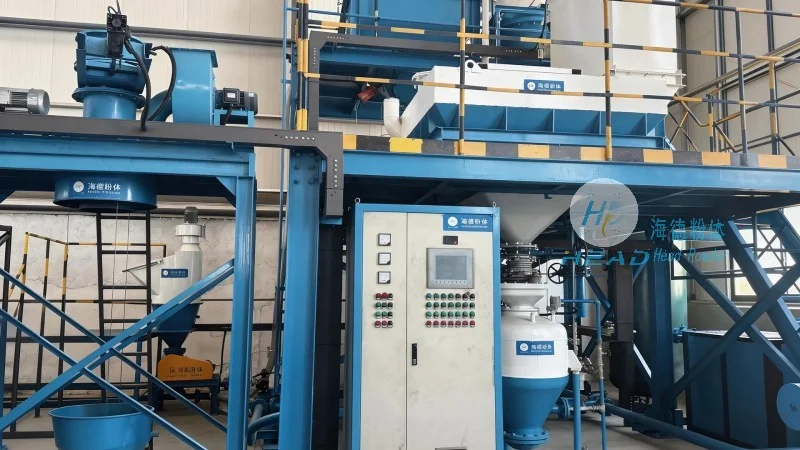
The design of a pneumatic conveying system for magnesium sulfate material relies on several core components that work in tandem to facilitate material transport. These components include the material feed system, which ensures consistent and controlled loading of the magnesium sulfate into the conveying line. The air supply system, often equipped with compressors and filters, provides the necessary pressure and clean air to move the material. Additionally, the conveying line itself, made from materials resistant to corrosion and abrasion, is crucial for maintaining the integrity of the magnesium sulfate during transport. Other essential parts include the separation and collection equipment, which helps in recovering the material from the air stream and preventing dust emissions.
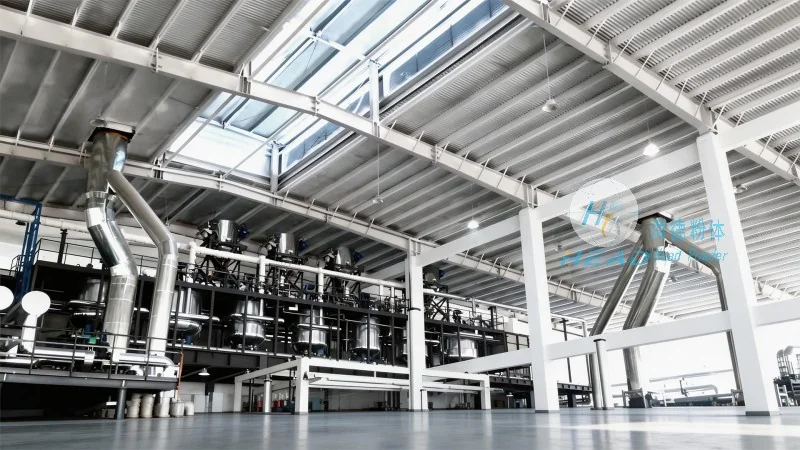
Efficient design of a pneumatic conveying system for magnesium sulfate hinges on several key principles that balance performance, cost, and operational safety. One of the primary considerations is the selection of the appropriate conveying velocity. The velocity must be high enough to prevent material settling or blockages but low enough to avoid excessive wear on the system components. This balance is critical for maintaining the longevity of the equipment and ensuring consistent material flow. Another important principle is the system's pressure and flow rate optimization. Properly sizing the air compressor and pipeline diameter ensures that the system operates within its optimal range, minimizing energy consumption and maximizing throughput. Furthermore, the design must account for the physical properties of magnesium sulfate, such as its particle size, density, and moisture content. These factors influence the selection of the conveying method—whether it's a dilute phase or dense phase system—and the overall system configuration.
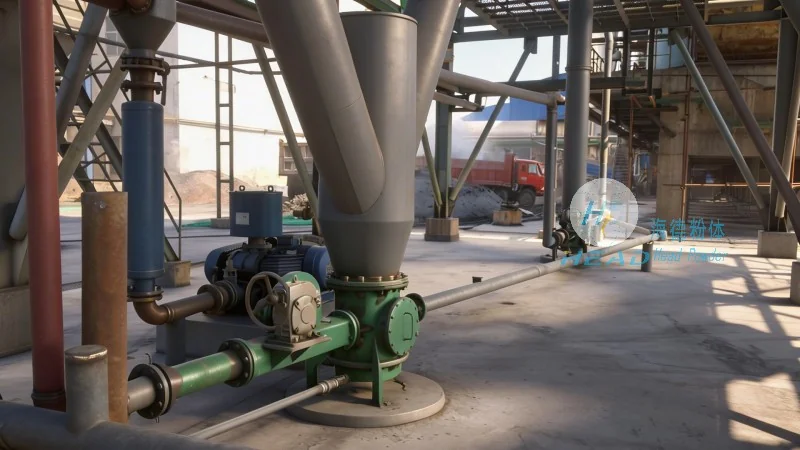
Implementing a pneumatic conveying system for magnesium sulfate offers numerous advantages over traditional methods like belt conveyors or bucket elevators. One of the most significant benefits is the ability to transport material in a closed system, which helps in controlling dust emissions and maintaining a clean working environment. This is particularly important for magnesium sulfate, which can be a respiratory irritant if not handled properly. Additionally, pneumatic conveying allows for flexible and compact system layouts, as the pipelines can be routed around obstacles and integrated into existing plant layouts without major structural changes. The system also enables continuous material flow, reducing downtime and improving overall production efficiency. Furthermore, the process is relatively simple to automate, with sensors and controls that can monitor and adjust the conveying parameters in real-time, ensuring consistent performance and minimizing the risk of material loss or contamination.
While pneumatic conveying offers many benefits, there are also challenges and considerations that must be addressed during the design and operation of the system. One of the main challenges is the potential for material buildup or blockages in the pipeline, especially if the magnesium sulfate particles are sticky or have a high moisture content. To mitigate this, the system may include features like in-line mixers or vibrators to prevent clogging. Another consideration is the wear and corrosion of system components due to the abrasive nature of magnesium sulfate particles. Using materials like stainless steel or specialized coatings can help extend the lifespan of the equipment. Additionally, energy consumption is a factor, as pneumatic conveying systems can be energy-intensive, especially at high pressures. Optimizing the system design to use the minimum required pressure and flow rate can help reduce energy costs and environmental impact. Finally, the system must comply with safety regulations, particularly regarding dust explosion prevention and material handling safety, which may require additional equipment like explosion-proof motors or dust collection systems.
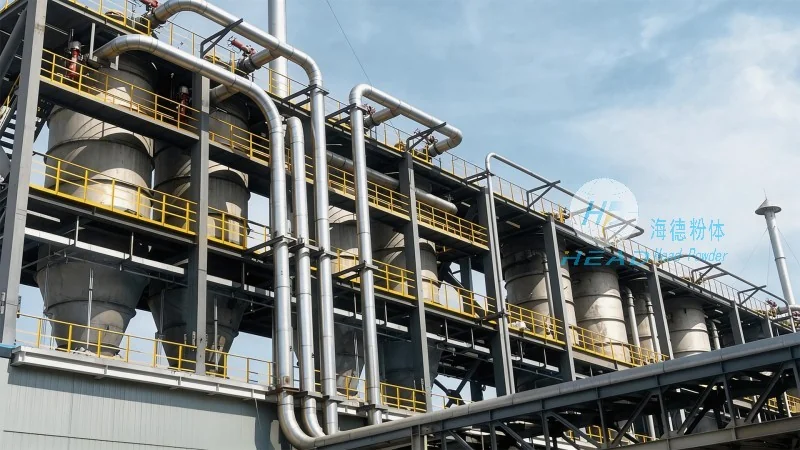
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, has successfully implemented pneumatic conveying systems for magnesium sulfate in various industrial applications. One notable project involved a client in the chemical processing industry who needed to transport large quantities of magnesium sulfate from a storage silo to a processing unit. The HeadPowder team designed a custom dilute phase system that utilized a high-efficiency air compressor and a specially designed pipeline network. The system was configured to operate at a pressure of 0.8 MPa, with a conveying velocity of 20 m/s, ensuring reliable and continuous material flow. The client reported significant improvements in production efficiency, with a reduction in downtime from 5% to less than 1% and a decrease in labor costs associated with manual material handling. The system also helped in maintaining a clean and safe working environment, as the closed pipeline design minimized dust emissions and required less frequent cleaning of equipment. This case study highlights the effectiveness of pneumatic conveying systems designed by HeadPowder, demonstrating how tailored solutions can address specific industrial challenges and deliver measurable benefits.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top