Dry gravel material pneumatic conveying is a specialized method used to transport dry, granular materials like gravel through a pipeline using air pressure. This technology is widely applied in various industries, including mining, construction, and material processing, where efficient and reliable material handling is crucial. Understanding the fundamentals of this process and its design principles is essential for optimizing operational efficiency and ensuring the longevity of conveying systems.
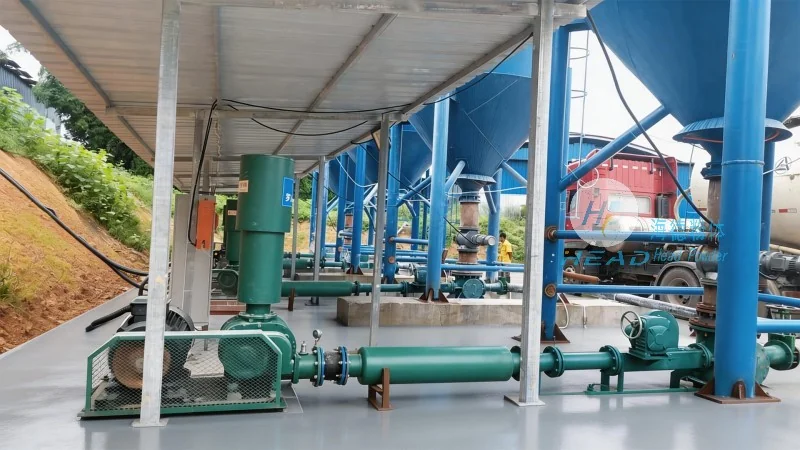
Dry gravel material pneumatic conveying involves the movement of dry, solid particles such as gravel through a pipeline by utilizing compressed air or gas. Unlike traditional bulk material handling methods that rely on gravity or mechanical equipment, pneumatic conveying offers a flexible and efficient solution for transporting materials over short to medium distances. The process typically involves a source of material, a conveying line, and a receiver where the material is deposited. Compressed air is introduced at one end of the pipeline, creating a pressure differential that propels the gravel particles forward. This method is particularly advantageous for materials that are difficult to handle with conventional equipment, such as those with high abrasiveness or irregular shapes.
The design of a dry gravel material pneumatic conveying system is governed by several critical principles that ensure optimal performance and reliability. These principles include the selection of appropriate air velocity, the sizing of the conveying line, and the choice of components like pumps, filters, and receivers. Air velocity is a key factor, as it must be sufficient to lift and transport the gravel particles without causing excessive wear on the system components. The conveying line diameter and length are also critical, as they directly impact the pressure drop and energy consumption of the system. Additionally, the system must be equipped with proper filtration and separation mechanisms to prevent the buildup of dust and debris, which can affect the performance and longevity of the equipment.
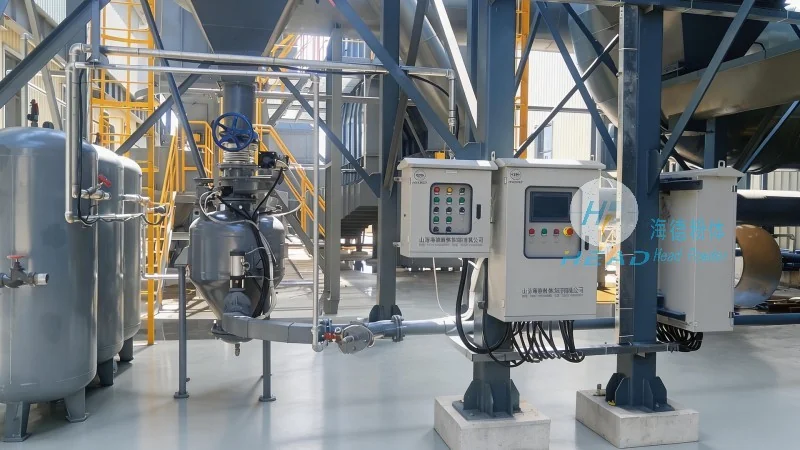
A typical dry gravel material pneumatic conveying system consists of several key components, each playing a vital role in the overall operation. The primary components include the material feeder, which feeds the gravel into the conveying line, the air compressor or blower that generates the necessary pressure, the conveying line itself, and the receiver or discharge device where the material is collected. The material feeder is designed to handle the specific characteristics of the gravel, such as its size, density, and flowability, ensuring a consistent feed rate. The air compressor provides the required pressure to move the material through the line, and the conveying line is constructed from durable materials like stainless steel or plastic to withstand the abrasive nature of the gravel. The receiver is equipped with filters and separation devices to capture any fine particles and prevent them from entering the system, maintaining the purity of the conveyed material.
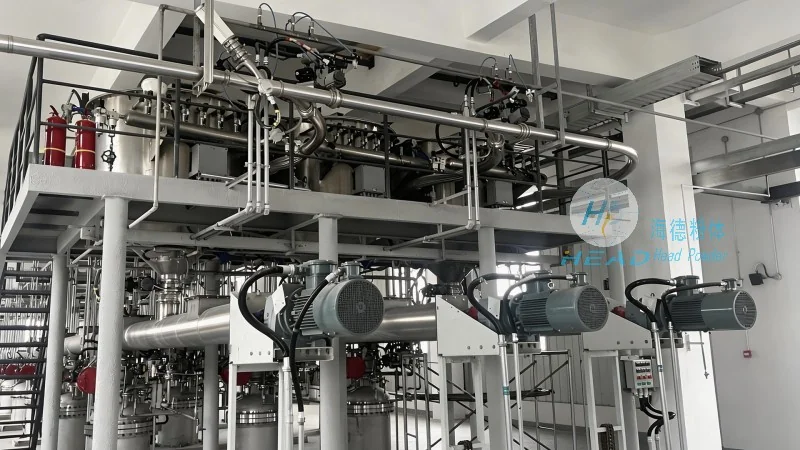
Dry gravel material pneumatic conveying offers several advantages over traditional material handling methods. One of the main benefits is its ability to transport materials in a closed system, which reduces dust emissions and improves workplace safety. This is particularly important in industries where dust can be a health hazard or cause environmental issues. Additionally, pneumatic conveying systems are highly flexible, allowing for changes in the conveying route or material type without significant modifications to the system. The technology is also suitable for transporting materials over long distances, making it an ideal solution for mining operations where raw materials need to be moved from extraction sites to processing facilities.
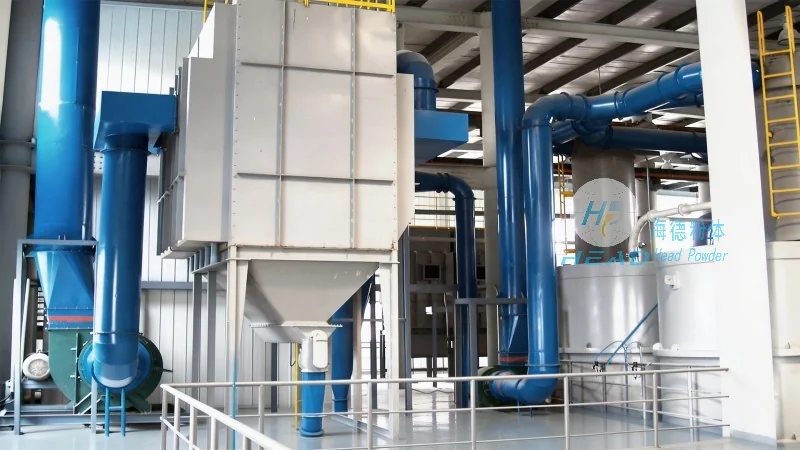
When designing a dry gravel material pneumatic conveying system, several factors must be considered to ensure its effectiveness and longevity. These factors include the material properties of the gravel, such as its size distribution, density, and abrasiveness, as well as the required conveying distance and flow rate. The system must be designed to handle the specific characteristics of the gravel to prevent issues like blockages or excessive wear. Regular maintenance is also crucial for the performance of the system, as components like filters, pumps, and conveying lines require periodic inspection and replacement to maintain optimal operation. Proper maintenance can significantly extend the lifespan of the system and reduce downtime, ensuring consistent material handling performance.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of pneumatic conveying solutions and related engineering services. With a strong focus on innovation and quality, HeadPowder specializes in designing and manufacturing customized pneumatic conveying systems for various industrial applications. The company is committed to delivering reliable and efficient solutions that meet the specific needs of its clients, ensuring optimal performance and long-term durability. HeadPowder's expertise in material handling technology, combined with its dedication to customer satisfaction, makes it a trusted partner for businesses seeking advanced pneumatic conveying solutions. Located in Shandong, China, HeadPowder leverages its local resources and industry knowledge to provide comprehensive support to clients worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top