Gas-pneumatic conveying systems are widely used in industrial applications for the efficient transport of bulk materials, including dust and powders. The principle of these systems relies on the use of compressed air to create a flow that moves material from a source to a destination. This method offers several advantages over traditional mechanical conveying methods, such as reduced equipment wear, lower maintenance costs, and the ability to handle materials that are difficult to transport by other means. The system operates by generating a high-velocity air stream within a pipeline, which entrains the material particles and propels them forward. The air flow is typically controlled by a blower or compressor, and the conveying velocity is adjusted based on the material's properties, such as particle size, density, and moisture content.
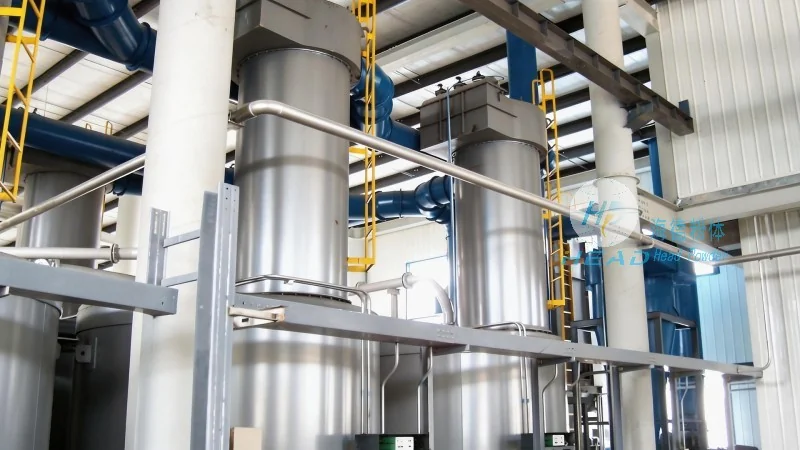
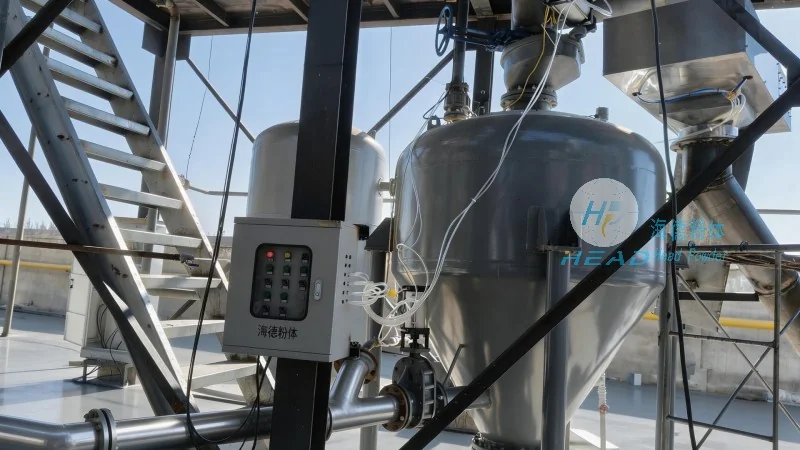
The operation of a dust gas-pneumatic conveying system involves several key components working in concert. The primary components include a material hopper, a conveyor line, a venturi or eductor, and a receiver or discharge point. The process begins when material is fed from the hopper into the conveyor line. Compressed air is then introduced into the system, typically at the venturi or eductor, where it creates a low-pressure zone that draws the material into the air stream. The mixture of air and material travels through the pipeline to the receiver, where the material is separated from the air and collected. The material hopper is designed to hold the bulk material and ensure a consistent feed rate, often equipped with level sensors and feeding mechanisms such as screw conveyors or rotary valves. The conveyor line, usually made of stainless steel or other corrosion-resistant materials, is sized to handle the specific flow rate and particle characteristics of the material. The venturi or eductor is the heart of the system, where the compressed air is accelerated to create the necessary suction force. The design of the venturi nozzle and the air inlet size determines the system's conveying capacity and efficiency. The receiver or discharge point is where the material is deposited, often equipped with dust collection systems or air filtration to prevent re-entrainment of dust.
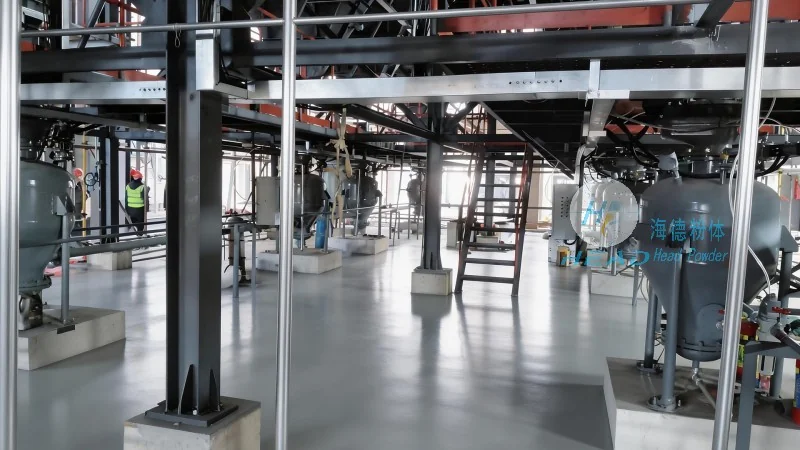
For dust and powder handling, gas-pneumatic conveying systems provide significant benefits. These include the ability to transport materials over long distances with minimal loss, the reduction of dust emissions compared to open systems, and the flexibility to handle a wide range of particle sizes and densities. Additionally, the system can be designed to operate under negative pressure, which helps contain dust and prevent environmental contamination. The low friction and wear on components also contribute to longer service life and lower operational costs. Compared to mechanical systems like belt conveyors or screw conveyors, gas-pneumatic systems are less prone to material buildup and clogging, especially for fine powders. This makes them ideal for applications where material flow needs to be continuous and reliable.
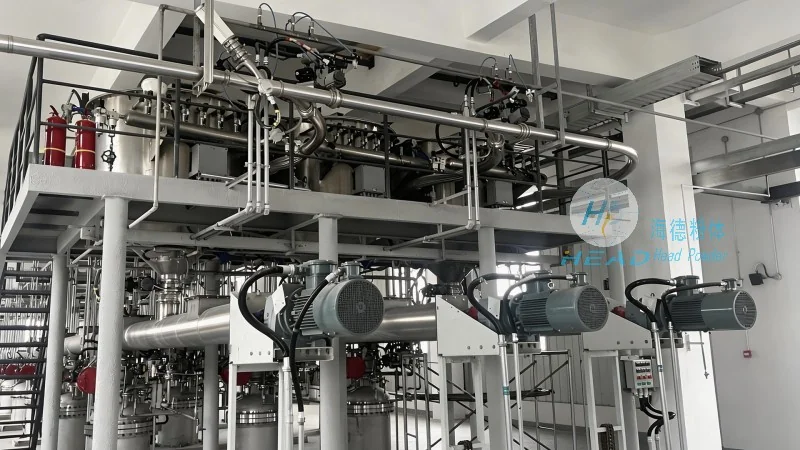
Gas-pneumatic conveying systems are employed in various industrial sectors where dust and powders need to be moved efficiently. For instance, in the pharmaceutical industry, these systems are used to transport raw materials and finished products with high precision and minimal contamination. The sterile design of the conveying lines and components ensures that the materials remain free from particulate contamination, which is critical in pharmaceutical manufacturing. In the food processing industry, they are utilized to convey ingredients and products while maintaining sanitary conditions. The systems are often equipped with cleaning-in-place (CIP) features and made from food-grade materials to meet regulatory standards. The chemical industry also benefits from these systems for handling reactive powders and ensuring safe material transfer. In chemical plants, the ability to handle hazardous materials under controlled conditions is essential, and gas-pneumatic conveying provides a safe and efficient solution. Each application leverages the system's ability to handle fine particles and maintain a controlled environment, ensuring product quality and operational safety.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of dust gas-pneumatic conveying solutions. The company specializes in designing, manufacturing, and installing customized conveying systems tailored to the specific needs of clients. With a focus on innovation and quality, headpowder delivers systems that meet industry standards and enhance operational efficiency. The company's headquarters is located in Shandong, China, where it leverages local expertise and resources to serve a global clientele. Headpowder's team of engineers and technicians work closely with clients to understand their material handling challenges and develop tailored solutions. The company's product line includes a range of conveying equipment, from small-scale systems for laboratory use to large industrial systems for bulk material transport. All systems are manufactured using high-quality materials and undergo rigorous testing to ensure performance and reliability. Headpowder's commitment to customer satisfaction and technical excellence has made it a trusted partner in the industry for over [years, if known, but as per info, just state as leading provider].

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top