Camellia seed pneumatic conveying equipment is a specialized system designed to transport camellia seeds efficiently and safely. This equipment plays a crucial role in the processing industry, particularly in applications where handling bulk solid materials is required. The core of this technology lies in the pneumatic conveying method, which utilizes air flow to move particles through a pipeline network. Understanding the structure and operational principles of such equipment is essential for optimizing material handling processes in various industrial settings.
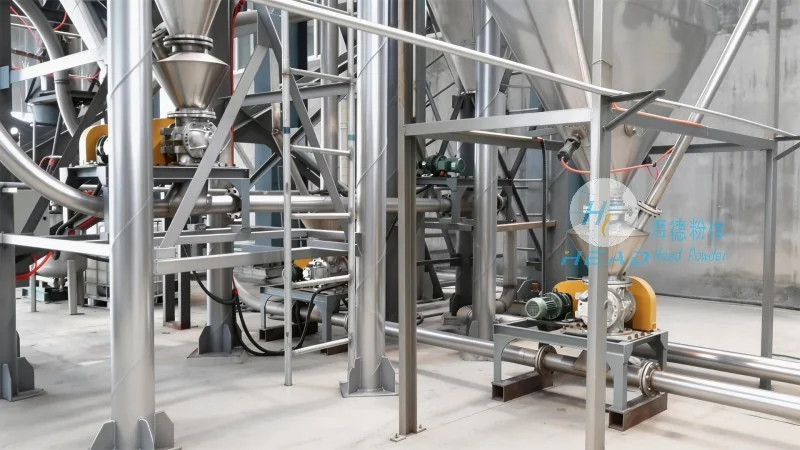
Pneumatic conveying systems for camellia seeds are engineered to handle the unique characteristics of this material. Camellia seeds are typically small, irregularly shaped, and may have varying moisture content, which can affect their flow properties. The equipment must be designed to accommodate these characteristics while ensuring minimal product damage and efficient transport. The system generally consists of a feeding mechanism, a conveying pipeline, a separation unit, and a discharge outlet. Each component works in tandem to ensure smooth and continuous operation.
The structure of a typical camellia seed pneumatic conveying system includes several critical components. The feeding unit is responsible for introducing the seeds into the system, often using a hopper or a rotary valve to control the flow rate. The conveying pipeline is where the seeds are transported by the air stream, which can be either positive pressure or negative pressure systems. Positive pressure systems use a blower to push air and material through the pipeline, while negative pressure systems use a vacuum to draw material in. The separation unit, such as a cyclone or a filter, is used to separate the seeds from the air stream, ensuring that the material is collected efficiently and without contamination. Finally, the discharge outlet allows the processed seeds to be removed from the system.
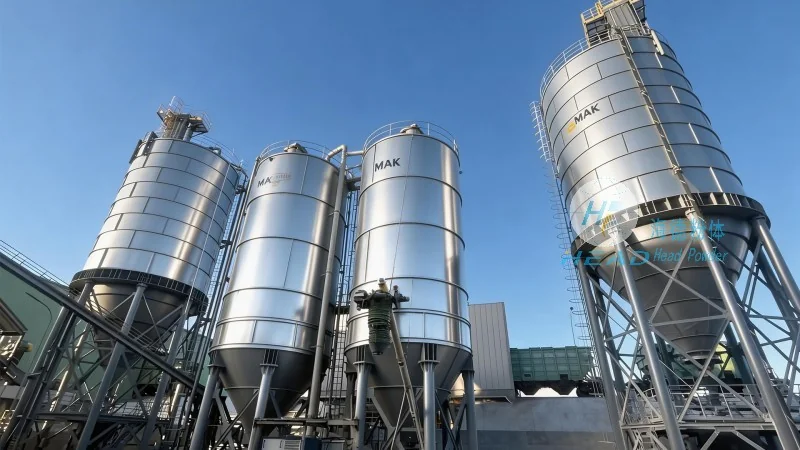
The operational principle of camellia seed pneumatic conveying equipment is based on the interaction between the material and the air flow. When the seeds are introduced into the system, they are entrained by the air stream and carried through the pipeline. The velocity of the air is crucial; it must be sufficient to lift and transport the seeds without causing excessive wear or damage. The system is designed to maintain a consistent air flow rate to ensure stable material transport. The separation process occurs as the air and material mixture enters the separation unit, where centrifugal force or filtration helps to separate the seeds from the air. This separation is critical for maintaining product quality and preventing dust or other contaminants from being released into the environment.
Implementing pneumatic conveying equipment for camellia seeds offers several advantages over traditional methods like belt conveyors or bucket elevators. One of the primary benefits is the ability to handle materials in a closed system, which reduces dust emissions and improves workplace safety. This is particularly important for camellia seeds, which can be a source of respiratory irritation if not handled properly. Additionally, pneumatic conveying systems can be more flexible in terms of layout, as they can be installed in various configurations to fit the specific needs of a facility. The equipment also allows for better control over the flow rate and material distribution, leading to more consistent processing outcomes.
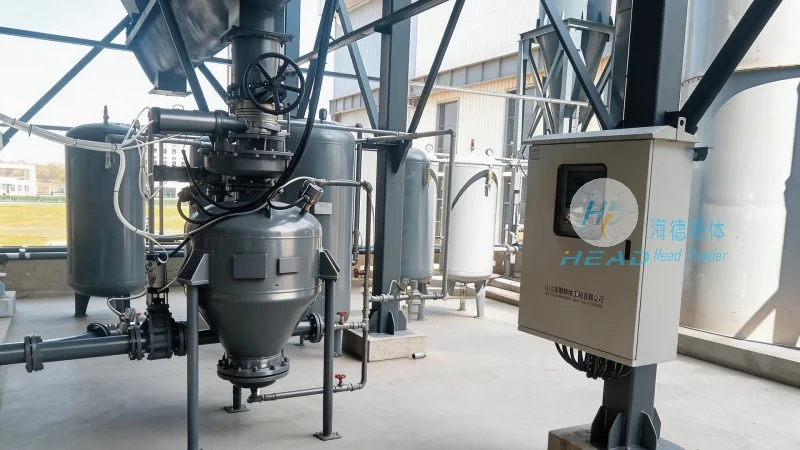
Camellia seed pneumatic conveying equipment is widely used in various industries, including food processing, pharmaceuticals, and agriculture. In the food industry, it is commonly used in the processing of camellia oil, where the seeds are transported from storage to processing lines. The equipment ensures that the seeds are handled hygienically and efficiently, minimizing the risk of contamination. In the pharmaceutical industry, the closed system of pneumatic conveying helps to maintain the purity of the material, which is essential for meeting regulatory standards. Agriculture and related processing facilities also benefit from the flexibility and efficiency of these systems, as they can be adapted to handle different types and quantities of camellia seeds.
Shandong HeadPowder Engineering Co., Ltd., also known as HeadPowder, is a leading manufacturer and supplier of specialized conveying equipment. With a focus on innovation and quality, the company has established itself as a trusted partner in the industry. HeadPowder's expertise lies in designing and manufacturing equipment tailored to the specific needs of clients, ensuring that their products meet the highest standards of performance and reliability. The company's facilities are located in Shandong, China, where it leverages advanced technology and skilled workforce to produce top-tier conveying solutions. HeadPowder is committed to providing comprehensive support to its clients, from initial consultation to after-sales service, ensuring that customers receive the best possible solutions for their material handling needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top