Graphite material handling systems are specialized equipment designed to transport and manage graphite materials efficiently. These systems are crucial in industries where graphite is used as a raw material or a finished product, such as in refractory manufacturing, battery production, and chemical processing. The design of these systems must consider the unique properties of graphite, including its high thermal conductivity, electrical conductivity, and chemical resistance. Graphite's ability to conduct heat and electricity makes it valuable in high-temperature applications and electronic components, while its chemical inertness allows it to resist corrosion in harsh environments. Consequently, the handling of graphite requires specialized equipment that can maintain these properties and prevent contamination. HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design and production of such systems, offering tailored solutions for various industrial applications.
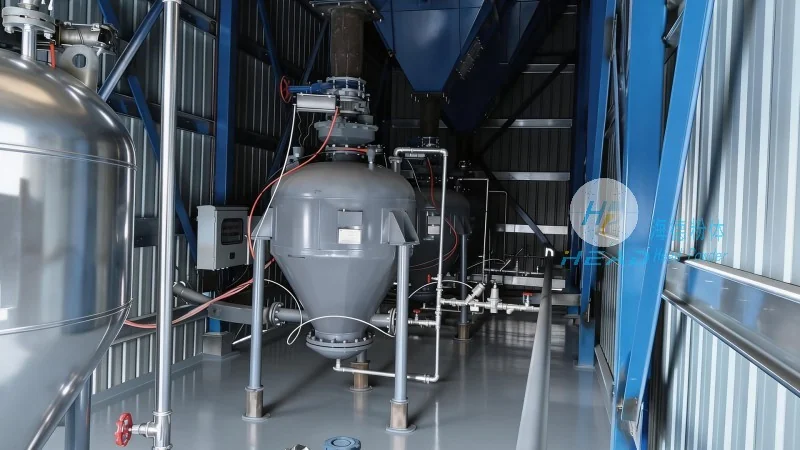
The core components of a graphite material handling system typically include feeders, conveyors, storage bins, and discharge mechanisms. Each component is engineered to handle the specific characteristics of graphite, ensuring minimal material degradation and optimal operational performance. For instance, feeders are often equipped with adjustable speed controls to regulate the flow of graphite, preventing overloading or clogging. The design of feeders may vary; for fine powders, a rotary valve or a vibratory feeder is commonly used, while for larger pieces, a belt feeder or a screw conveyor is preferred. Conveyors may use belt or screw mechanisms, chosen based on the particle size and moisture content of the graphite. Belt conveyors are suitable for dry, free-flowing graphite, while screw conveyors are effective for handling moist or sticky materials. Storage bins are designed with smooth, non-stick surfaces to avoid material buildup and ensure uniform discharge. These bins are often equipped with liners or coatings that resist the abrasive nature of graphite, extending their service life.
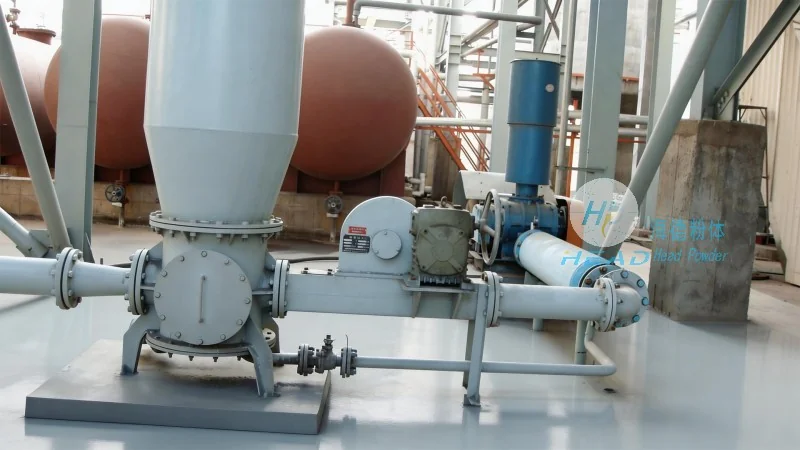
The design principles for graphite material handling systems prioritize several key factors: material flow optimization, equipment durability, and safety. Material flow optimization involves creating a continuous and controlled movement of graphite from the source to the processing or packaging stage. This is achieved through the integration of feeders, conveyors, and storage systems that work in harmony. The system's layout is carefully planned to minimize the distance and number of transfers, reducing energy consumption and material loss. Equipment durability is critical due to the abrasive nature of graphite, which can cause wear on components over time. Therefore, materials such as stainless steel, hardened steel, or specialized coatings are used for parts that come into direct contact with the graphite. For example, conveyor belts may be made of high-density polyethylene or rubber with a hard surface to resist abrasion. Safety considerations are paramount, as graphite dust can be hazardous. Systems often include dust collection and filtration systems to maintain a safe working environment. Additionally, enclosed designs and local exhaust ventilation are implemented to prevent dust from spreading into the workplace. These measures comply with occupational health and safety regulations and protect both personnel and the environment.
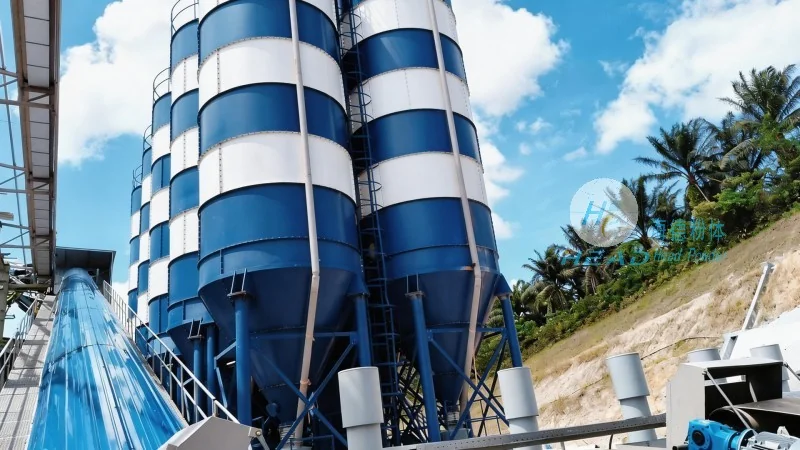
The design of graphite material handling systems varies based on the specific application. For example, in battery manufacturing, the system may need to handle fine graphite powders with high precision to ensure uniform coating on electrodes. The design must minimize particle agglomeration and ensure a consistent particle size distribution. This often involves using air classifiers or sieving equipment to separate fine from coarse particles before feeding them into the system. In refractory production, larger graphite pieces may be handled, requiring robust conveyors and storage bins that can withstand heavy loads. The system may include a screening process to remove oversized or undersized pieces, ensuring that only the correct size graphite is used in the final product. In chemical processing, the system may need to handle graphite in a wet or slurry form, requiring specialized equipment such as slurry pumps and hydrocyclones. These components are designed to handle the abrasive and corrosive nature of the slurry while maintaining the integrity of the graphite particles.
Modern graphite material handling systems offer several operational advantages. These include improved material throughput, reduced downtime due to maintenance, and enhanced safety features. The use of automated controls allows for precise regulation of the material flow, minimizing waste and optimizing production efficiency. For instance, a system with a programmable logic controller (PLC) can adjust the feeder speed in real-time based on the demand from the processing line, ensuring a steady supply of graphite without overloading the system. Advanced systems may also incorporate sensors to monitor the condition of components, predicting maintenance needs and preventing unexpected failures. This proactive approach to maintenance extends the lifespan of the equipment and reduces operational costs. Additionally, the integration of data collection and analysis tools provides insights into system performance, enabling continuous improvement and optimization. This data-driven approach helps identify bottlenecks and inefficiencies, allowing for targeted upgrades and adjustments.
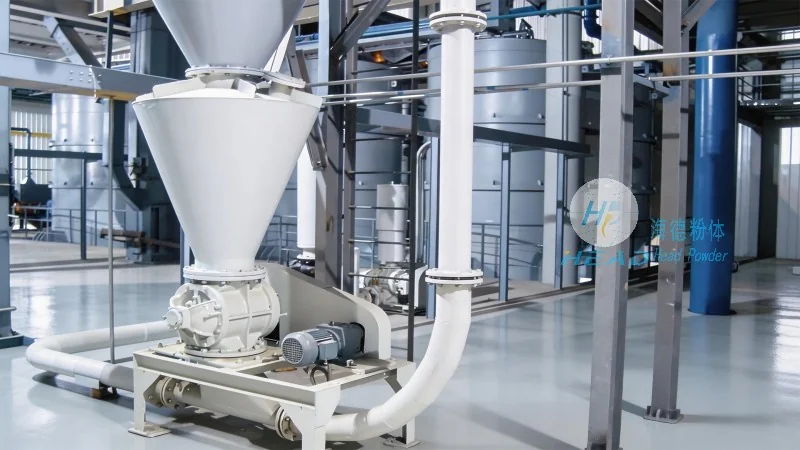
Graphite material handling systems are often customized to fit the specific needs of a facility. This includes integration with existing production lines, storage areas, and processing equipment. Customization may involve adjusting the size and capacity of the system, modifying the material handling components, or incorporating additional features such as dust suppression or material sorting. The goal is to create a seamless workflow that enhances overall operational efficiency without disrupting current processes. This approach ensures that the new system complements the existing infrastructure rather than requiring a complete overhaul. For example, a system may be designed to fit into a limited space by using vertical storage bins or compact conveyors. Integration with existing control systems is also crucial, allowing the new equipment to communicate with the facility's central control panel. This ensures that the system operates in sync with other processes, preventing conflicts and maintaining overall production stability. Customization also allows for the inclusion of specific safety features required by the facility's local regulations, ensuring compliance and operational safety.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top