For industrial applications requiring precise material handling, metering bin pump pneumatic conveying systems offer an efficient solution. This technology is widely used in various sectors, including chemical, food, and pharmaceutical industries, where accurate control of bulk materials is crucial. The core of this system lies in the metering bin pump, which combines the functions of a feeder and a pump to deliver materials through a pipeline under pressure.
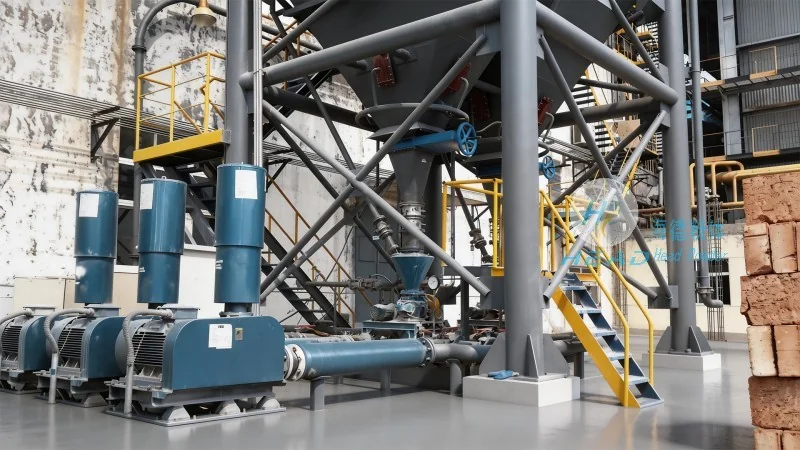
Metering bin pump pneumatic conveying is a type of pneumatic conveying system that uses a bin pump to meter and transport bulk materials. Unlike traditional systems that rely on pressure or vacuum alone, the metering bin pump provides precise control over the flow rate, ensuring consistent and reliable material transfer. This is achieved through a combination of mechanical and pneumatic components that work in tandem to maintain a stable pressure and flow within the system.
The design of a metering bin pump system is centered on several key principles that ensure optimal performance and efficiency. First, the system must be capable of handling a wide range of materials, from fine powders to bulk solids, with minimal degradation or segregation. This is achieved through the use of specialized hopper designs and feeding mechanisms that minimize material flow interruptions and maintain uniformity.
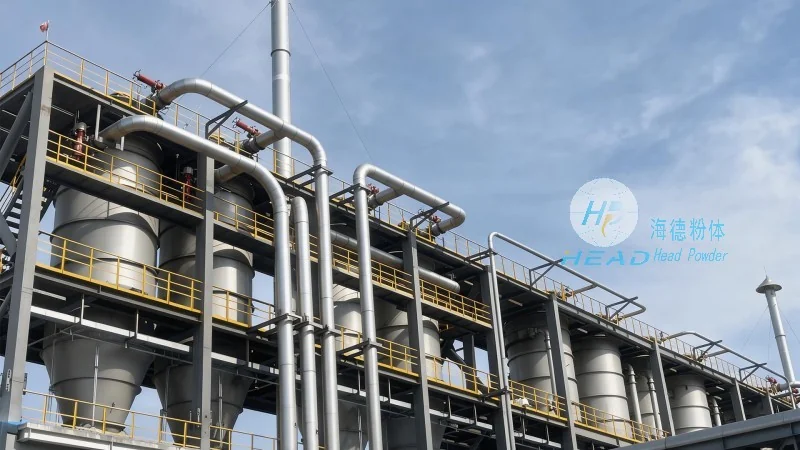
Second, the system incorporates a pressure vessel or bin that stores the material to be conveyed. The bin is equipped with a valve system that controls the release of material into the conveying line. The pump itself operates by creating a pressure differential, drawing material from the bin and propelling it through the pipeline using compressed air or other gases. This design allows for continuous operation without the need for frequent stops, enhancing productivity.
Several critical components make up a metering bin pump pneumatic conveying system. The most important is the metering bin, which serves as the storage and feeding unit. The bin is typically designed with a conical or hopper shape to facilitate material flow and prevent clogging. The feeding mechanism, often a rotary valve or a screw feeder, regulates the amount of material entering the conveying line, ensuring a consistent flow rate.
The pump unit, which may be a positive displacement pump or a diaphragm pump, generates the necessary pressure to move the material through the pipeline. Compressed air or other gases are introduced into the pump to create the pressure differential. The pipeline system, including elbows, tees, and filters, is designed to minimize pressure loss and prevent material buildup. Finally, the system includes a receiver or discharge bin at the end of the line, where the material is deposited.
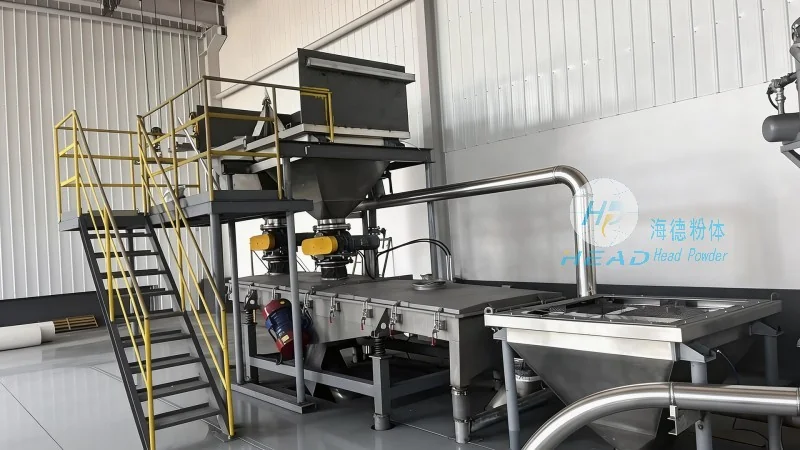
There are several advantages to using metering bin pump systems for material handling. One of the primary benefits is the ability to achieve precise control over the flow rate, which is essential for processes that require exact material quantities. This leads to improved product quality and reduced waste. Additionally, the system is relatively compact and can be integrated into existing facilities, making it a cost-effective solution for many applications.
Another advantage is the system's ability to handle a wide variety of materials, including those that are abrasive or corrosive. The design of the components, such as the hopper and pump, is typically made from durable materials like stainless steel or high-grade plastics to withstand the wear and tear of these materials. This ensures long-term reliability and minimal maintenance.
Metering bin pump pneumatic conveying systems are used in a variety of industrial applications. In the chemical industry, they are used to transport powders and granules for processing and packaging. In the food industry, they are employed to handle ingredients like flour, sugar, and spices, ensuring that the materials are transferred without contamination. In the pharmaceutical industry, the system is used to convey raw materials and finished products, maintaining strict hygiene and quality control standards.
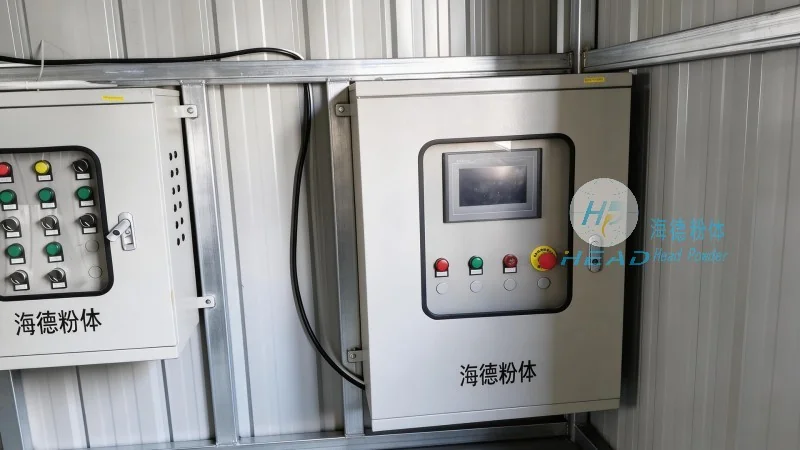
In addition to these sectors, the system is also used in the mining and construction industries for transporting bulk materials like sand, gravel, and cement. The ability to handle abrasive materials makes it suitable for these applications, where traditional conveying methods may not be effective.
Metering bin pump pneumatic conveying is a sophisticated and efficient technology that offers precise control over material handling in industrial settings. The design principles, which focus on reliability, accuracy, and durability, make it an ideal solution for a wide range of applications. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing these systems to meet the specific needs of various industries. With their expertise and commitment to quality, they ensure that clients receive systems that are not only effective but also long-lasting and cost-efficient.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top