Welcome to Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial dust collection solutions. In this article, we will explore the pulse jet dust collector material handling system, its core design principles, and how it effectively manages dust and particulate matter in various industrial applications.
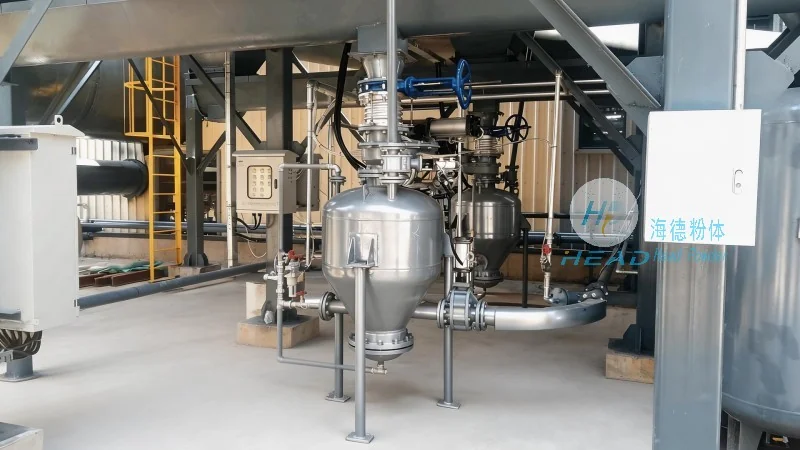
A pulse jet dust collector is a critical component in industrial settings where air filtration and material handling are essential. This system combines dust collection with material transport, making it ideal for processes that generate airborne particles, such as in manufacturing, mining, and construction. The primary function of this system is to capture dust and other particulates from the air stream and transport them to a collection point, ensuring a clean and safe working environment.
The design of a pulse jet dust collector material handling system is built on several key principles that ensure efficient operation and long-term performance. The most fundamental principle is the use of reverse air pulses to dislodge accumulated dust from the filter media. This process, known as "pulsing," involves rapidly increasing the pressure in the filter housing, creating a high-velocity air jet that shakes the filter bags or cartridges, causing the dust to fall into the hopper below. The design must also consider the material being handled, as different particles may require varying pulse pressures and frequencies to achieve optimal cleaning.
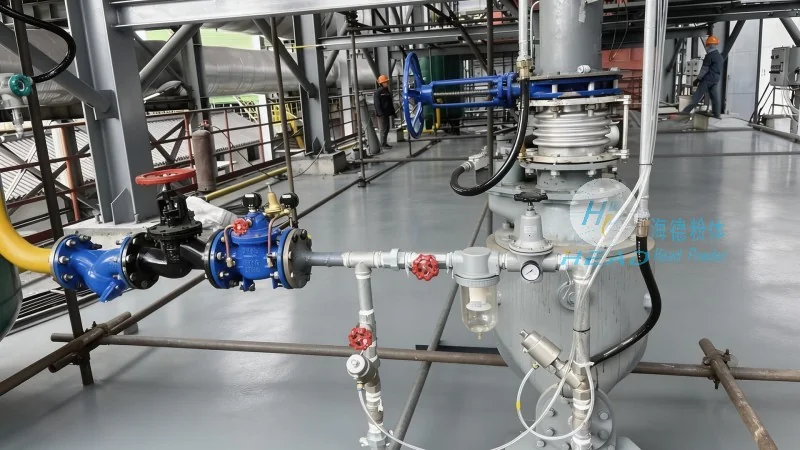
Several key components work together to make the pulse jet dust collector material handling system effective. The main components include the filter housing, which houses the filter bags or cartridges; the pulse valve, which controls the release of compressed air; the hopper, where collected dust is stored; and the control instrument, which regulates the timing and duration of the pulses. The filter bags are typically made of durable materials like polyester or polypropylene, designed to trap fine particles while allowing clean air to pass through. The pulse valve is a critical component that delivers short bursts of high-pressure air to the filter bags, ensuring thorough cleaning without excessive energy consumption.
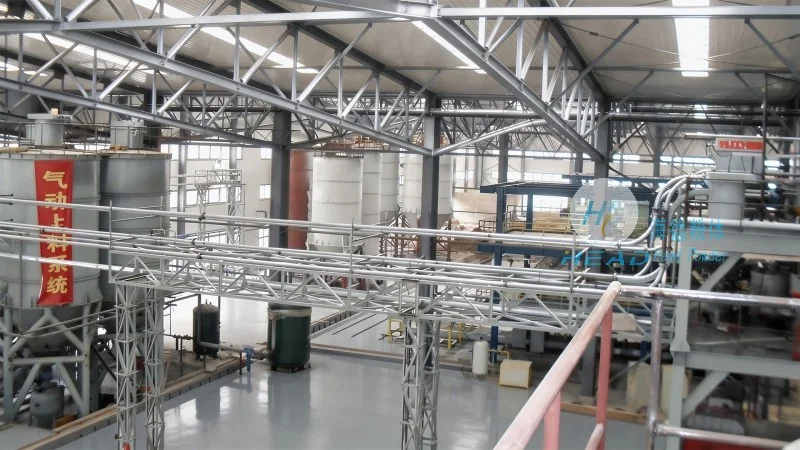
Pulse jet dust collector material handling systems are widely used in industries where dust control is paramount. Common applications include cement plants, power generation facilities, and metalworking operations. The benefits of this system include high filtration efficiency, low operating costs, and minimal maintenance requirements. By effectively capturing dust and particulates, the system not only improves air quality but also reduces the risk of fire hazards and equipment damage caused by accumulated dust. Additionally, the material handling aspect of the system ensures that collected dust is safely transported to a disposal or recycling point, preventing environmental contamination.
At Shandong HeadPowder Engineering Co., Ltd., we specialize in designing and manufacturing pulse jet dust collector material handling systems tailored to the specific needs of our clients. Our team of engineers leverages advanced technology and years of experience to deliver solutions that meet the highest standards of performance and reliability. Whether you are in the process of selecting a new dust collection system or upgrading an existing one, our products are designed to provide long-term value and operational efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top