Understanding the role and design principles of nitrogen-protected material handling systems is crucial for industries dealing with sensitive materials that require protection from atmospheric exposure. These systems are engineered to maintain an inert nitrogen environment throughout the material's transport, storage, and processing stages. By creating a barrier against oxygen, moisture, and contaminants, such systems ensure the integrity and quality of the handled materials, making them indispensable in sectors like pharmaceuticals, food processing, and specialty chemicals.
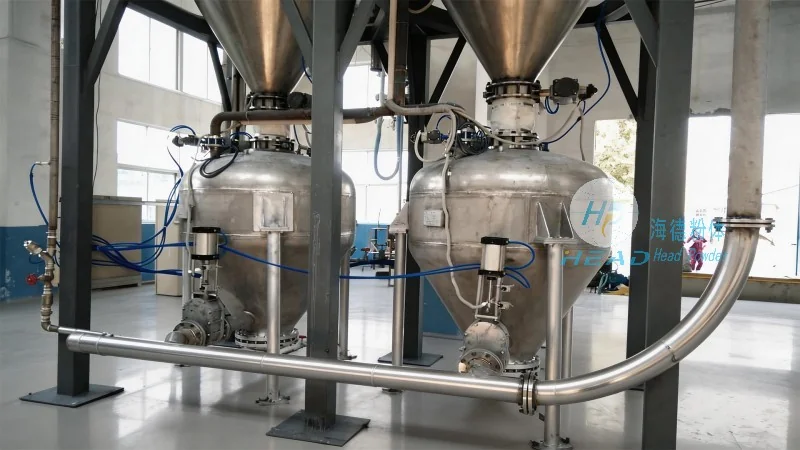
The core components of a nitrogen-protected system include a high-purity nitrogen gas source, a distribution network of pipes and valves, and material handling equipment designed to operate within the inert atmosphere. The nitrogen gas source typically consists of a nitrogen generator or a high-pressure cylinder, ensuring a consistent supply of dry, oxygen-free gas. The distribution system features pressure regulators, flow meters, and check valves to control the flow and pressure of the nitrogen, preventing backflow and maintaining system integrity. Material handling equipment, such as pneumatic conveyors, bulk bags, or silos, is integrated with the nitrogen system to keep the material enclosed in an inert environment from the point of loading to unloading.
The design of a nitrogen-protected system follows several key principles to ensure efficiency and reliability. First, the system must maintain a continuous nitrogen blanket over the material, preventing oxygen ingress and moisture absorption. This is achieved through proper sealing of all connections and equipment, minimizing any potential leaks. Second, the system is designed to handle the specific properties of the material, such as its particle size, flowability, and reactivity. For example, in pharmaceutical applications, the system may include HEPA filters to remove particulate contaminants from the nitrogen stream, ensuring the material remains sterile and free from microbial growth. Third, safety is a critical consideration in the design. The system includes pressure relief valves and gas detectors to monitor for any deviations from the inert atmosphere, providing early warnings and preventing hazardous conditions. Additionally, the design adheres to industry standards like ASME, ISO, and local regulations to ensure compliance and safety.
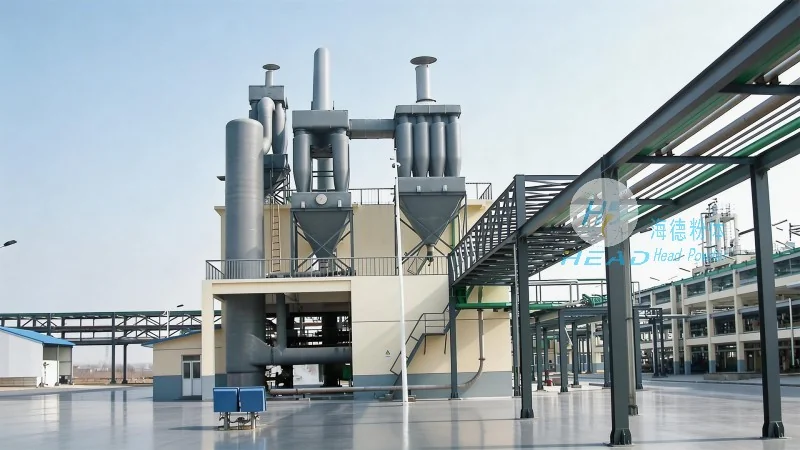
While the fundamental design of nitrogen-protected systems is consistent, the specific implementation varies based on the application. In food processing, for instance, the system may be designed to handle temperature-sensitive materials, with temperature control features integrated into the equipment to maintain the material's quality. In the pharmaceutical industry, the system may incorporate cleanroom-compatible components and aseptic design to prevent contamination during transport. The choice of materials for the equipment, such as stainless steel or food-grade plastics, is also tailored to the application to ensure compatibility with the handled materials and to meet regulatory requirements. For example, in chemical processing, the system may use corrosion-resistant materials to handle aggressive chemicals, while in food processing, food-grade materials are used to prevent any chemical contamination.
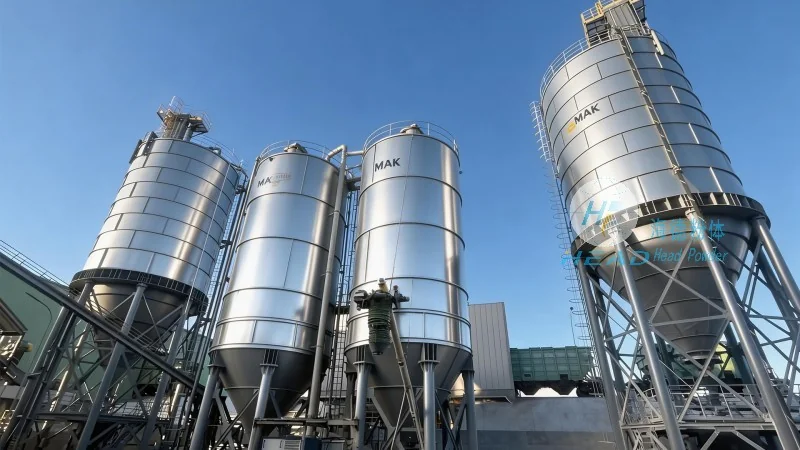
Adopting a nitrogen-protected material handling system offers numerous benefits for industries dealing with sensitive materials. The primary benefit is the preservation of material quality, as the inert nitrogen environment prevents oxidation, degradation, and contamination. This leads to improved product consistency and reduced waste, as the material remains in its original state throughout the handling process. Additionally, the system enhances operational efficiency by eliminating the need for post-processing steps to restore material quality, such as reprocessing or reconditioning. The use of nitrogen also reduces the risk of fire or explosion in environments where flammable materials are handled, as the oxygen content is kept at a safe level. Furthermore, the system improves safety for operators by minimizing exposure to hazardous materials and reducing the risk of accidents caused by material degradation or contamination.
Nitrogen-protected material handling systems are essential for industries that require the safe and efficient transport of sensitive materials. The design principles, components, and application-specific considerations outlined above highlight the importance of a well-engineered system in maintaining material integrity and operational efficiency. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized nitrogen-protected systems tailored to the unique needs of each industry. With a focus on quality, safety, and innovation, HeadPowder ensures that its systems meet the highest standards and deliver reliable performance. Located in Shandong, China, HeadPowder leverages its expertise and advanced technology to provide solutions that enhance the productivity and safety of material handling processes across various sectors. By investing in a nitrogen-protected system, industries can protect their materials, improve their operational efficiency, and ensure compliance with industry regulations, ultimately achieving greater success in their respective markets.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top