Understanding dust collection material conveying systems is crucial for industries that handle powders and fine particulates. These systems are integral to maintaining air quality, ensuring operational efficiency, and complying with environmental regulations. The design principles behind such systems are complex, involving a combination of engineering expertise, material science, and practical application knowledge. In this article, we explore the core components, operational mechanisms, and key design considerations of dust collection material conveying systems, with insights from Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field.
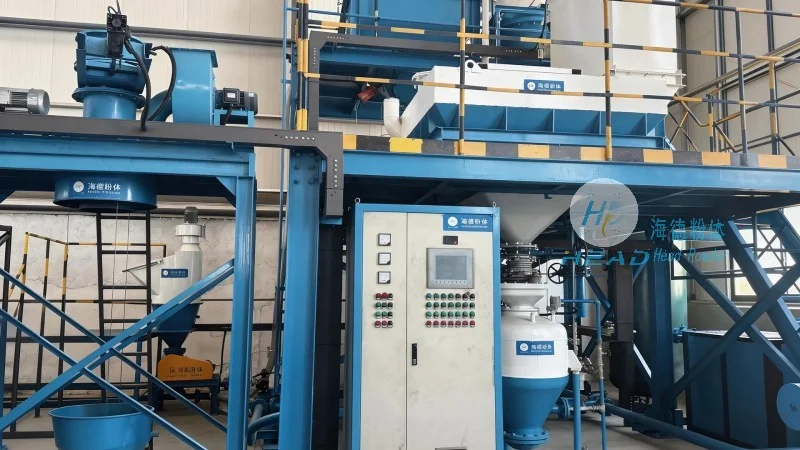
A dust collection material conveying system is a specialized setup designed to collect, transport, and manage dust or fine particles generated during industrial processes. These systems are commonly used in sectors like cement production, mining, chemical manufacturing, and food processing, where airborne particulates pose health risks and environmental concerns. The primary goal of such systems is to capture dust at its source, transport it to a collection point, and then either recycle it or dispose of it safely. This not only improves workplace safety but also enhances overall production efficiency by preventing material loss and equipment damage caused by dust accumulation.
The effectiveness of a dust collection material conveying system depends on its well-designed components, each playing a vital role in the overall operation. The main components typically include:
1. Dust Collectors: These are the central units responsible for capturing dust particles from the air stream. Common types include baghouse filters, cartridge filters, and electrostatic precipitators. The choice of collector depends on the particle size, moisture content, and chemical properties of the dust. For example, baghouse filters are ideal for capturing fine powders, while electrostatic precipitators are effective for larger particles.
2. Conveying Equipment: This includes devices like pneumatic conveyors, screw conveyors, and bucket elevators that transport the collected dust from the collector to a storage or processing area. Pneumatic conveyors use air pressure to move dust through pipelines, making them suitable for long-distance transport and handling of dry powders. Screw conveyors, on the other hand, are used for horizontal or slight incline transport, providing a reliable method for moving bulk materials.
3. Piping and Fittings: The network of pipes and fittings connects all components of the system, ensuring a smooth flow of air and dust. The design of the piping system is critical, as it must minimize pressure drop and prevent dust buildup. Materials such as stainless steel or PVC are commonly used to resist corrosion and wear from the transported particles.
4. Control Systems: Modern dust collection systems incorporate advanced control systems that monitor and regulate the operation of the equipment. These systems include sensors for pressure, temperature, and dust concentration, as well as control panels that adjust the system's performance based on real-time conditions. This automation enhances efficiency and reduces the risk of system failures.
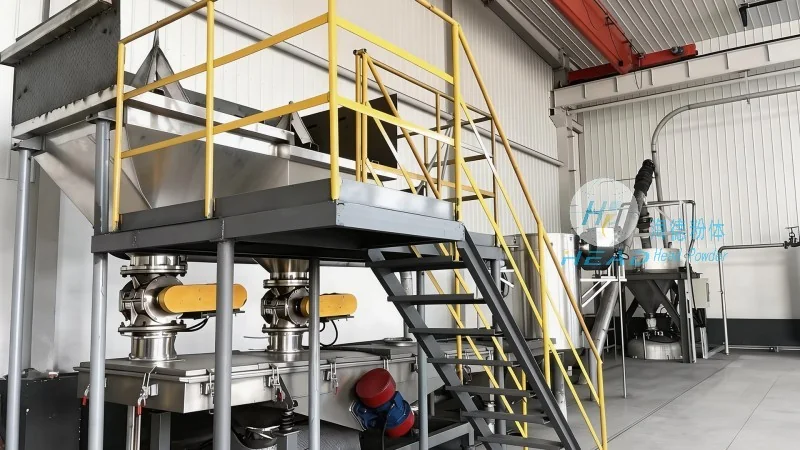
The design of a dust collection material conveying system involves several key principles to ensure optimal performance and longevity. Engineers from Shandong HeadPowder Engineering Co., Ltd. emphasize the importance of considering the following factors:
1. Material Compatibility: The system's components must be compatible with the specific dust being handled. For instance, if the dust is acidic or corrosive, materials like stainless steel or special coatings are required to prevent degradation. This ensures the system's durability and reduces maintenance costs.
2. Flow Rate and Pressure Drop: The design must account for the required flow rate and the pressure drop across the system. High flow rates may require larger ducts or more powerful fans, while excessive pressure drop can lead to energy inefficiency and reduced system performance. Proper sizing of the ductwork and fans is essential to maintain optimal airflow.
3. System Integration: The dust collection system must be integrated seamlessly with the existing industrial processes. This includes coordinating with other equipment, such as hoppers, mixers, and storage silos, to ensure a smooth material flow. A well-integrated system minimizes bottlenecks and maximizes overall productivity.
4. Environmental Regulations: Compliance with local and national environmental regulations is a critical design consideration. Systems must be designed to meet or exceed emission standards, often requiring additional filtration or treatment steps. This not only avoids legal penalties but also contributes to sustainable industrial practices.
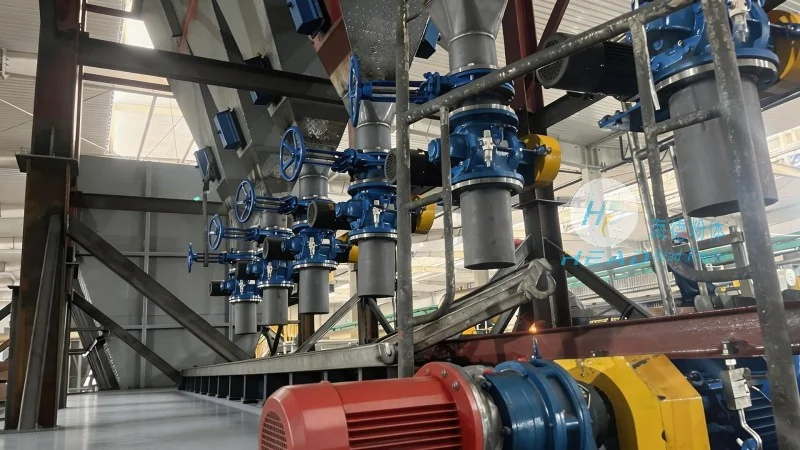
The operational mechanisms of a dust collection material conveying system involve a series of steps that work in tandem to achieve effective dust management. The process typically begins with the generation of dust particles in the production environment. These particles are then drawn into the system by a fan or blower, which creates a negative pressure in the ductwork. The air stream carrying the dust passes through the dust collector, where the particles are separated from the air and collected in a hopper or bin.
The collected dust is then transported to a storage or processing area using the conveying equipment. Pneumatic conveyors, for example, use compressed air to push the dust through the pipelines, ensuring a continuous and efficient transport process. The design of the conveying system must account for the dust's properties, such as its density and moisture content, to prevent blockages and ensure smooth operation.
Efficiency in dust collection is measured by the system's collection efficiency, which indicates the percentage of dust particles captured. High-efficiency systems, such as baghouse filters with multi-stage filtration, can achieve collection efficiencies of over 99%, effectively reducing airborne particulates. Regular maintenance, including filter cleaning and system checks, is essential to maintain this efficiency and prevent system downtime.
Dust collection material conveying systems offer numerous benefits to industrial operations. By effectively capturing and managing dust, these systems improve workplace safety by reducing the risk of respiratory diseases and other health issues. They also protect equipment from dust-related damage, such as clogging and corrosion, which can lead to costly repairs and production downtime. Additionally, these systems help in maintaining a clean and organized work environment, enhancing employee morale and productivity.
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized dust collection material conveying systems tailored to the specific needs of various industries. With years of experience and a team of skilled engineers, the company provides comprehensive solutions that address the unique challenges of each client. Their systems are designed to be energy-efficient, reliable, and compliant with environmental regulations, ensuring long-term performance and customer satisfaction.
In conclusion, dust collection material conveying systems are essential components of modern industrial operations, playing a critical role in maintaining air quality, ensuring operational efficiency, and complying with environmental standards. The design principles behind these systems involve careful consideration of components, material compatibility, flow rates, and regulatory requirements. With the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., industries can implement effective dust management solutions that enhance safety, productivity, and sustainability. As industrial processes continue to evolve, the importance of well-designed dust collection systems will only grow, making them a vital investment for any facility handling powders and fine particulates.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top