Ammonia fertilizer is a critical component in modern agricultural practices, and the efficient handling of its powder form requires specialized equipment. One such device is the ammonia fertilizer powder conveyor, which plays a vital role in transporting these granular or powdered materials from one location to another within industrial or agricultural settings. This article aims to provide a comprehensive overview of what an ammonia fertilizer powder conveyor is and delve into the underlying design principles that make it effective for its intended purpose.
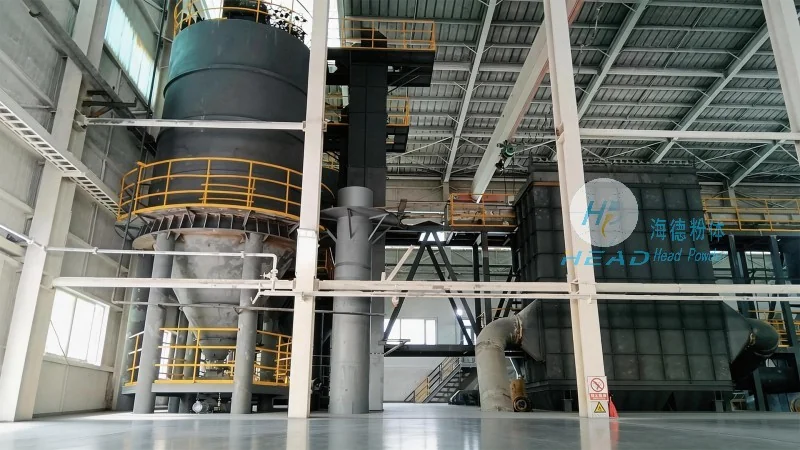
In agricultural and industrial applications, ammonia fertilizers are often produced in bulk quantities and need to be transported to storage facilities, processing plants, or directly to farms. Traditional methods of handling such powders, such as manual shoveling or basic mechanical systems, are often inefficient, time-consuming, and pose health and safety risks. Ammonia fertilizer powder conveyors address these challenges by offering a reliable, automated solution for the movement of these materials. These conveyors are designed to handle the unique properties of ammonia fertilizer, including its potential to be hygroscopic (absorbing moisture from the air) and its sensitivity to temperature and pressure changes. By utilizing advanced engineering and materials, these systems ensure that the fertilizer remains in optimal condition throughout the transportation process.
The design of an ammonia fertilizer powder conveyor is guided by several key principles that ensure its functionality, efficiency, and safety. The first principle is the selection of appropriate materials for the construction of the conveyor components. Since ammonia fertilizer can be corrosive and may come into contact with moisture, the conveyor parts, such as the hopper, chute, and drive mechanisms, are typically made from materials like stainless steel or corrosion-resistant alloys. This choice prevents degradation of the equipment and maintains the quality of the fertilizer during transport. Another critical design principle is the consideration of the flow characteristics of the powder. Ammonia fertilizer powders can exhibit different flow behaviors, including cohesive or non-cohesive properties, depending on moisture content and particle size. The conveyor design must account for these variations to prevent issues like bridging (where the powder forms a solid plug in the hopper) or segregation (where different particle sizes separate during transport). To mitigate these problems, conveyors often incorporate features like agitators, vibrators, or air-assisted systems that help maintain a consistent flow and prevent material buildup.
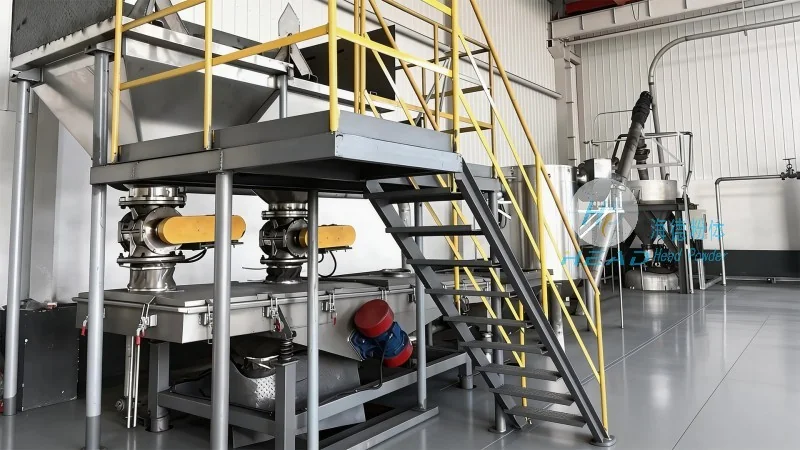
Ammonia fertilizer powder conveyors consist of several interconnected components, each playing a specific role in the overall operation. The primary components include the hopper, which serves as the storage and feeding unit where the fertilizer is loaded. The hopper is designed with a sloped bottom to facilitate the flow of the powder into the conveyor system. The chute or pipe, which is typically made of flexible or rigid material, transports the fertilizer from the hopper to the discharge point. The drive mechanism, which can be powered by electric motors or pneumatic systems, provides the necessary force to move the powder through the chute. In many designs, a control system is integrated to regulate the flow rate and ensure consistent operation. Additionally, safety features such as pressure relief valves and dust suppression systems are often included to protect both the equipment and the environment from potential hazards. The combination of these components, carefully engineered to work in harmony, ensures that the ammonia fertilizer is transported safely and efficiently.
Implementing ammonia fertilizer powder conveyors offers numerous advantages over traditional handling methods. Firstly, these systems significantly improve operational efficiency by automating the transportation process, reducing the need for manual labor and minimizing downtime. This leads to increased productivity and cost savings for agricultural and industrial operations. Secondly, the automated nature of the conveyors enhances safety by minimizing human exposure to the fertilizer, which can be hazardous if mishandled. The enclosed design of the conveyor system also helps in controlling dust emissions, reducing the risk of respiratory issues and environmental contamination. Furthermore, the precise control over the flow rate allows for better inventory management and reduces the risk of overloading or underloading the system. These advantages make ammonia fertilizer powder conveyors an essential investment for any facility dealing with ammonia-based fertilizers.
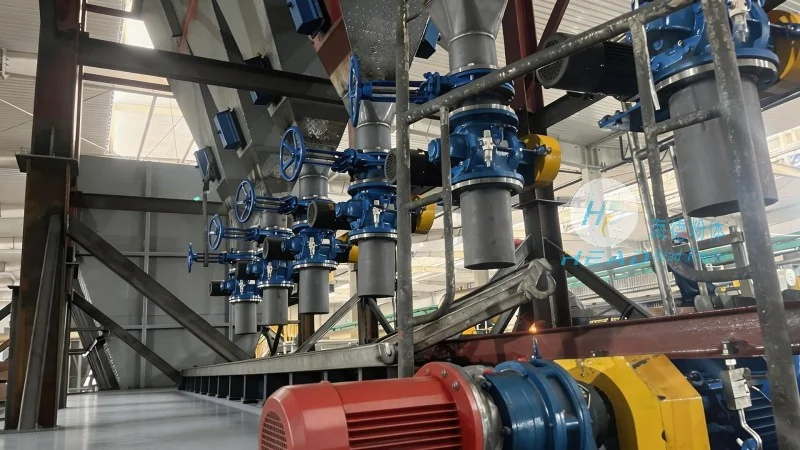
Ammonia fertilizer powder conveyors are widely used in various industries, primarily in the agricultural sector, but also in industrial applications related to fertilizer production and processing. In agriculture, these conveyors are used to transport ammonia fertilizer from storage silos to application equipment on farms, ensuring that the fertilizer is delivered to the fields in a timely and consistent manner. This is particularly important for large-scale farming operations where the efficient distribution of fertilizer is critical for crop yields. In industrial settings, such as fertilizer manufacturing plants, the conveyors are used to move raw materials or intermediate products between different processing stages. The ability to handle bulk quantities of ammonia fertilizer efficiently makes these conveyors indispensable in the production of various types of fertilizers, including urea, ammonium nitrate, and other nitrogen-based compounds. Additionally, the versatility of these systems allows them to be adapted for use in other powder handling applications, such as in the chemical or food processing industries, where similar material properties and handling requirements exist.
Ammonia fertilizer powder conveyors are sophisticated pieces of equipment that play a crucial role in the efficient and safe handling of ammonia-based fertilizers. Their design is based on principles that address the unique properties of the fertilizer, ensuring optimal performance and minimal risk. By automating the transportation process, these conveyors enhance productivity, improve safety, and reduce operational costs for agricultural and industrial operations. The technology behind these systems continues to evolve, with ongoing improvements in materials, control systems, and energy efficiency. For businesses dealing with ammonia fertilizers, investing in a high-quality powder conveyor system is a strategic decision that can significantly impact their overall operational efficiency and success. As a leading manufacturer in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in providing customized ammonia fertilizer powder conveyor solutions tailored to the specific needs of their clients. With a focus on quality, innovation, and customer satisfaction, HeadPowder has established itself as a trusted partner in the agricultural and industrial sectors, helping to meet the growing demand for efficient fertilizer handling solutions. Based in Shandong, China, HeadPowder leverages its expertise and advanced manufacturing capabilities to deliver reliable and durable conveyor systems that meet the highest industry standards. Whether for large-scale farming operations or industrial fertilizer production, HeadPowder's ammonia fertilizer powder conveyors offer a proven solution for efficient material handling.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top