When it comes to handling soap granules in industrial processes, selecting the right material handling solution is crucial for efficiency, safety, and cost-effectiveness. Pneumatic conveying systems have emerged as a preferred method for transporting bulk materials like soap granules due to their ability to handle various particle sizes, maintain product integrity, and operate in a controlled environment. However, with multiple system types available, businesses often face the challenge of determining which system best suits their specific soap granules handling requirements. This article aims to guide you through the key considerations and factors to evaluate when choosing a pneumatic conveying system for your soap granules processing line.
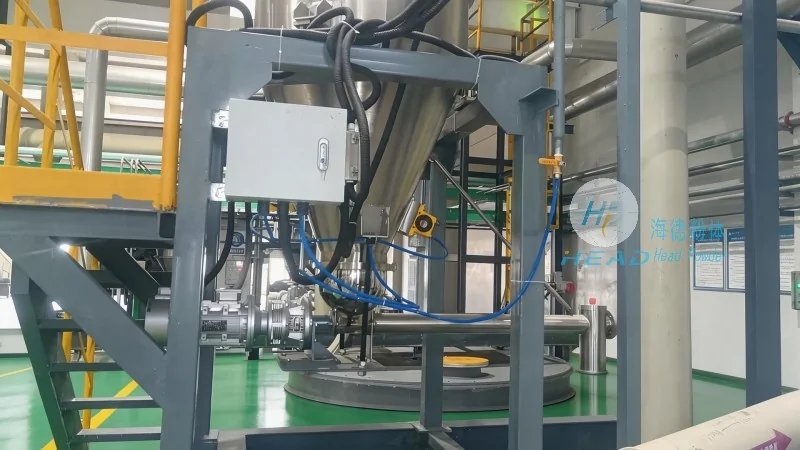
Pneumatic conveying systems utilize air or gas to transport bulk materials through a pipeline network. They are categorized into two main types: positive pressure (or pressure) systems and negative pressure (or vacuum) systems. Positive pressure systems force air and material through the pipeline, while negative pressure systems draw material into the system using a vacuum. Each type has distinct advantages and is suitable for different applications. For soap granules, which may vary in size and density, understanding these differences is essential to ensure optimal performance.
Several critical factors must be evaluated when choosing a pneumatic conveying system for soap granules. The first consideration is the material's physical properties, such as particle size distribution, bulk density, and moisture content. Soap granules can range from fine powders to coarse granules, and the system must be designed to handle these variations without causing blockages or degradation. Additionally, the system's capacity and flow rate requirements are vital, as they directly impact production throughput. For instance, a high-volume soap production line may require a larger conveying capacity compared to a smaller-scale operation.
Another important factor is the distance and layout of the conveying path. The length and number of turns in the pipeline will affect the system's pressure drop and energy consumption. Proper system design, including the selection of appropriate pipeline diameters and air velocities, is crucial to maintain material flow and prevent system inefficiencies. Furthermore, the need for product containment and environmental considerations should be addressed. Pneumatic conveying systems can be designed to minimize dust emissions and ensure compliance with industrial safety standards, which is particularly important for soap granules that may be sensitive to contamination.
For soap granules handling, several pneumatic conveying system options are commonly used. The most suitable system depends on the specific application and operational constraints. One popular choice is the positive pressure system, which uses a blower to push air and material through the pipeline. This system is ideal for short to medium distances and can handle a wide range of particle sizes. It offers better control over material flow and is often preferred for applications requiring precise dosing or handling of sensitive materials like soap granules.
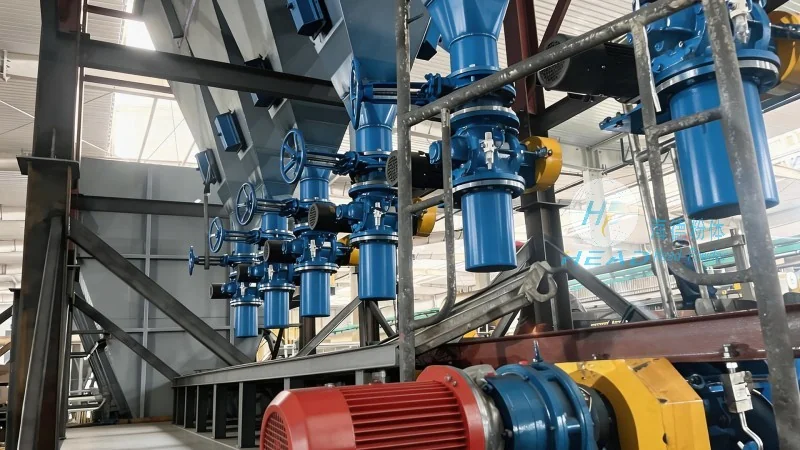
Negative pressure systems, on the other hand, use a vacuum to draw material into the system. These systems are suitable for longer conveying distances and can handle larger volumes of material. However, they may be more complex to install and maintain, as they require a vacuum pump and additional filtration to prevent dust accumulation. The choice between positive and negative pressure systems often depends on factors such as the distance between the source and destination, the material's properties, and the available space for system components.
Handling soap granules presents unique challenges that must be addressed in the design of a pneumatic conveying system. Soap granules are often hygroscopic, meaning they can absorb moisture from the air, which may affect their texture and performance. Therefore, the system must be designed to minimize exposure to ambient air and maintain a controlled environment. This may involve incorporating drying or moisture control measures within the conveying pipeline or storage areas. Additionally, soap granules may be sensitive to temperature changes, which can affect their processing characteristics. Proper temperature regulation during transport is essential to ensure consistent product quality.
Another consideration is the potential for material degradation during transport. Pneumatic conveying systems can generate high velocities and turbulence, which may cause attrition or breakage of soap granules. To mitigate this, system designers may use specialized components such as flexible hoses, low-velocity sections, or airlocks to reduce stress on the material. These measures help preserve the granules' size and shape, ensuring they maintain their intended properties for downstream processing or packaging.
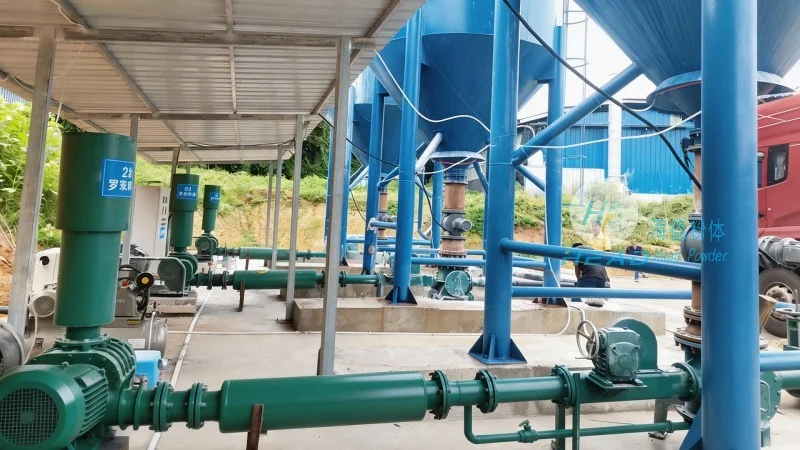
When selecting a pneumatic conveying system for soap granules, partnering with a reputable engineering company is essential to ensure the system meets your specific needs. Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing customized pneumatic conveying systems tailored to the unique requirements of soap granules handling processes. With years of experience in the industry, HeadPowder understands the challenges associated with transporting soap granules and offers comprehensive solutions that address material properties, system efficiency, and operational safety.
HeadPowder's team of engineers works closely with clients to assess their soap granules handling processes, identify potential bottlenecks, and recommend the most suitable pneumatic conveying system. The company provides a range of system types, including positive pressure, negative pressure, and hybrid systems, each designed to optimize performance based on the client's specific parameters. Their expertise extends to system integration, where they ensure seamless operation with existing production lines and equipment. By leveraging advanced design software and rigorous testing protocols, HeadPowder delivers systems that are not only efficient but also reliable and cost-effective.
HeadPowder's commitment to quality and customer satisfaction is reflected in their comprehensive after-sales support. The company offers maintenance services, technical assistance, and system upgrades to ensure long-term performance and adaptability to changing production needs. With a strong presence in China, HeadPowder serves clients across various industries, including soap manufacturing, where their pneumatic conveying systems have proven to enhance productivity and reduce operational costs.
Selecting the right pneumatic conveying system for your soap granules handling process is a critical decision that impacts overall operational efficiency and product quality. By considering factors such as material properties, conveying distance, system capacity, and environmental requirements, businesses can choose a system that meets their specific needs. Partnering with a trusted engineering company like Shandong HeadPowder Engineering Co., Ltd. ensures that the chosen system is tailored to the unique challenges of soap granules handling, providing reliable and efficient material transport. Whether you are operating a small-scale soap production line or a large industrial facility, investing in the right pneumatic conveying system can significantly improve your process performance and contribute to long-term success.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top