Flue gas desulfurization (FGD) is a critical process in industrial facilities that burn fossil fuels, such as coal or natural gas, to generate electricity or heat. The primary goal of FGD is to remove sulfur dioxide (SO₂) from the exhaust gases before they are released into the atmosphere. Among the various FGD technologies available, dry flue gas desulfurization systems have gained significant attention due to their efficiency, low operating costs, and compact design. This article aims to provide a comprehensive overview of what a dry flue gas desulfurization system is and to explain its fundamental design principles.
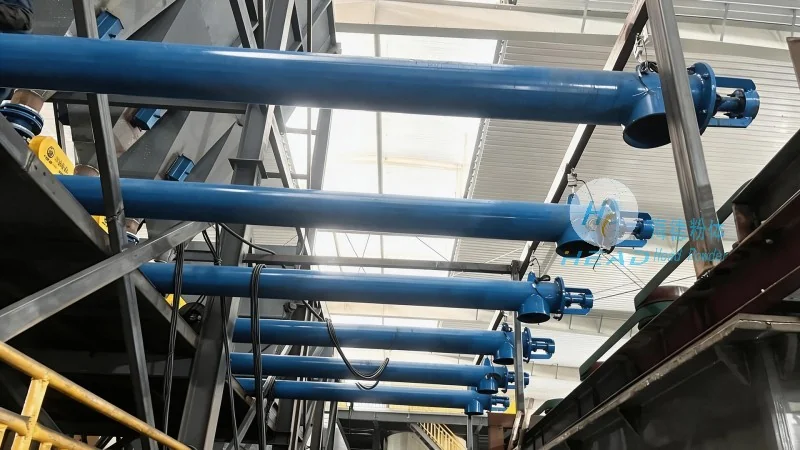
A dry flue gas desulfurization system is a technology used to remove sulfur dioxide from flue gases emitted by industrial processes. Unlike wet FGD systems that use liquid reagents, dry systems employ dry sorbents, typically limestone or calcium carbonate, to capture SO₂. The process involves several key components that work together to achieve efficient sulfur removal. The system typically includes a gas conditioning section, a reaction chamber, and a downstream particulate control device. The gas conditioning section prepares the flue gas by adjusting its temperature and moisture content to optimize the absorption of SO₂ by the sorbent particles. The reaction chamber is where the actual chemical reaction between the flue gas and the sorbent takes place, leading to the formation of solid byproducts. Finally, the downstream device, such as a baghouse or electrostatic precipitator, removes the solid particles from the treated gas before it is released.
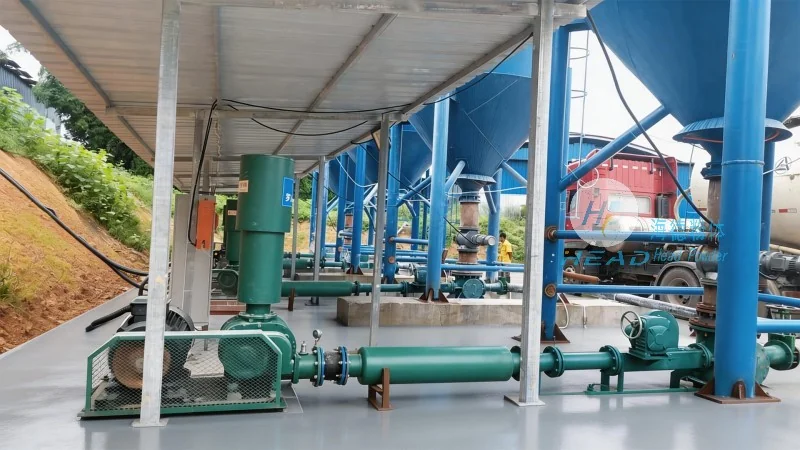
The design of a dry flue gas desulfurization system is based on several critical principles to ensure optimal performance and reliability. The first principle is the selection of an appropriate sorbent material. Limestone (calcium carbonate, CaCO₃) is the most common sorbent due to its availability, low cost, and high reactivity with SO₂. The sorbent is typically ground into a fine powder to increase its surface area, which enhances the absorption efficiency. The second principle is the control of gas temperature and moisture. The flue gas must be cooled to an optimal temperature range (typically between 120-180°C) to facilitate the chemical reaction and prevent the sorbent from becoming too dry or too wet. Moisture content is also crucial, as it affects the sorbent's reactivity and the formation of solid products. The third principle is the design of the reaction chamber. The chamber must provide sufficient contact time between the flue gas and the sorbent particles to ensure complete SO₂ absorption. This is often achieved through the use of a packed bed or a spray dryer absorber, where the gas flows through a bed of sorbent particles or is sprayed with a fine mist of sorbent slurry. The fourth principle is the integration of downstream particulate control. Since the dry system produces solid byproducts, a particulate control device is necessary to remove these particles from the treated gas. This ensures that the final emissions meet regulatory standards and prevents the accumulation of dust in the system.
Dry flue gas desulfurization systems offer several advantages over wet systems, making them suitable for a wide range of industrial applications. One of the main advantages is their lower operating costs, as they do not require large amounts of water or chemicals for operation. Additionally, dry systems are more compact and require less space compared to wet systems, which is beneficial for facilities with limited installation areas. Another advantage is their ability to handle high-temperature flue gases, as the dry process is less sensitive to temperature fluctuations. Dry FGD systems are commonly used in power plants, cement factories, and other industrial facilities that need to comply with stringent environmental regulations regarding SO₂ emissions. They are particularly effective in regions where water resources are scarce or where the cost of water treatment is high.
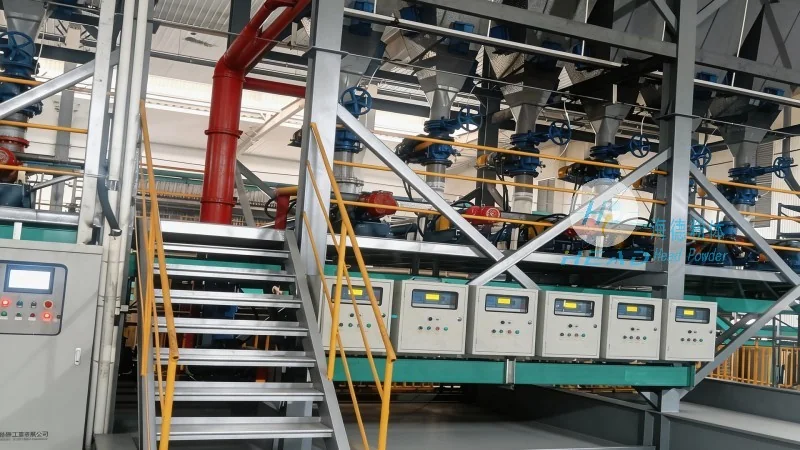
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of advanced industrial solutions, including dry flue gas desulfurization systems. With a strong commitment to innovation and quality, HeadPowder has established itself as a trusted partner for clients seeking reliable and efficient environmental control technologies. The company's expertise lies in the design, manufacturing, and installation of customized dry FGD systems tailored to meet the specific needs of each client. HeadPowder's team of experienced engineers and technicians ensures that each system is optimized for maximum performance and minimal maintenance. The company's facilities are located in Shandong, China, where it leverages its local resources and expertise to deliver high-quality products and services to customers worldwide. HeadPowder is dedicated to helping industrial facilities reduce their environmental impact while maintaining operational efficiency and cost-effectiveness.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top