Calcite, a widely used industrial mineral, often requires efficient and reliable material handling solutions for its processing and transportation. Pneumatic conveying systems are a critical component in the calcite industry, offering advantages such as reduced dust, improved safety, and enhanced process control. Understanding the main pneumatic conveying structures is essential for selecting the optimal system for calcite applications.
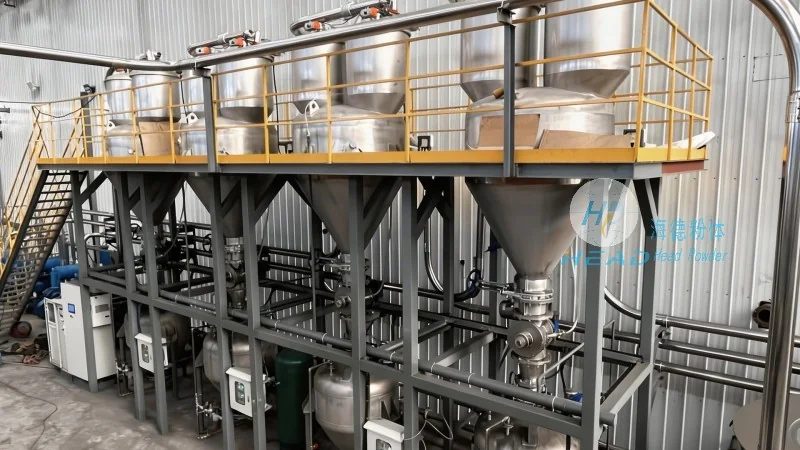
There are several primary pneumatic conveying structures commonly employed in calcite processing facilities. These systems are designed to handle the specific characteristics of calcite, including its particle size, density, and flowability. The main structures include positive pressure systems, negative pressure systems, and hybrid systems, each with distinct operational principles and applications.
Positive pressure systems, also known as pressure conveying systems, operate by generating air pressure within the conveying line. This method is particularly effective for calcite with higher moisture content or cohesive properties, as the positive pressure helps to maintain material flow and prevent blockages. The system typically consists of a blower or positive displacement pump, a hopper for material storage, and a series of pipes and fittings to transport the calcite. Key components include the air compressor, material feeder, and control valves. Positive pressure systems are often used for short to medium distance conveying, with typical distances ranging from 50 to 500 meters. They are well-suited for applications where the calcite needs to be delivered to a specific location, such as a storage silo or processing unit.
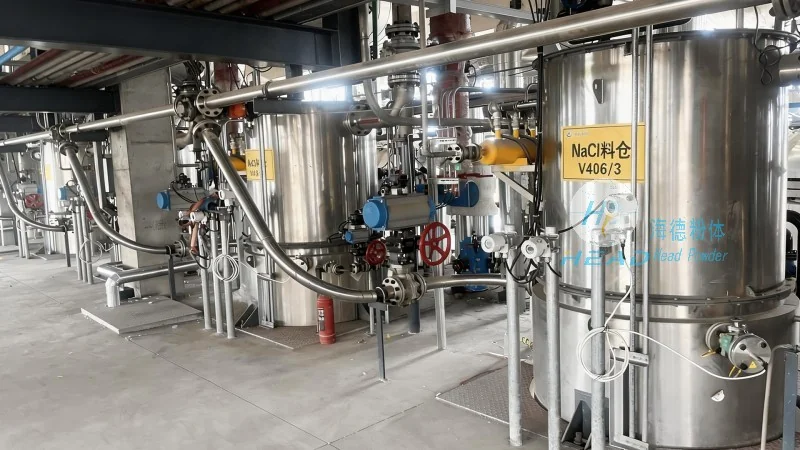
Negative pressure systems, or vacuum conveying systems, operate by creating a vacuum in the conveying line, drawing the calcite material from the source into the system. This method is ideal for calcite that is sensitive to air exposure or requires gentle handling. Negative pressure systems are commonly used for long-distance conveying, often up to several kilometers, and are particularly effective for handling fine or powdery calcite. The system includes a vacuum pump, a material collection hopper, and a filter to remove any dust or particles from the air stream. The vacuum pump creates the necessary suction, while the filter ensures that the air is clean and safe for the environment. Negative pressure systems are often preferred for applications where the calcite needs to be transported from a remote location to a processing facility, as they can handle longer distances with less pressure drop.
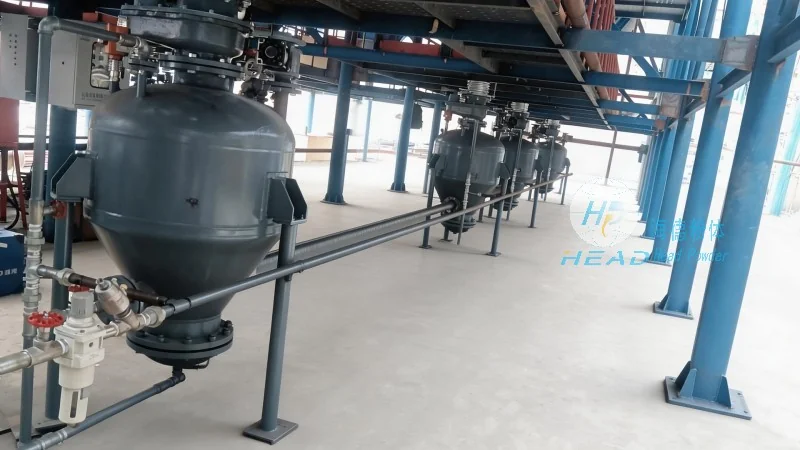
Hybrid systems combine elements of both positive and negative pressure systems, offering flexibility and efficiency for calcite processing. These systems are designed to handle a wide range of calcite characteristics and operational requirements. For example, a hybrid system might use a positive pressure section for the initial material transport and a negative pressure section for the final delivery to a processing unit. This approach allows for optimized energy use and reduced wear on system components. Hybrid systems are often used in complex calcite processing plants where multiple material handling tasks are required, such as conveying calcite from a mine to a processing plant and then to a storage facility. The hybrid design can also accommodate variations in calcite particle size and moisture content, ensuring consistent performance throughout the conveying process.
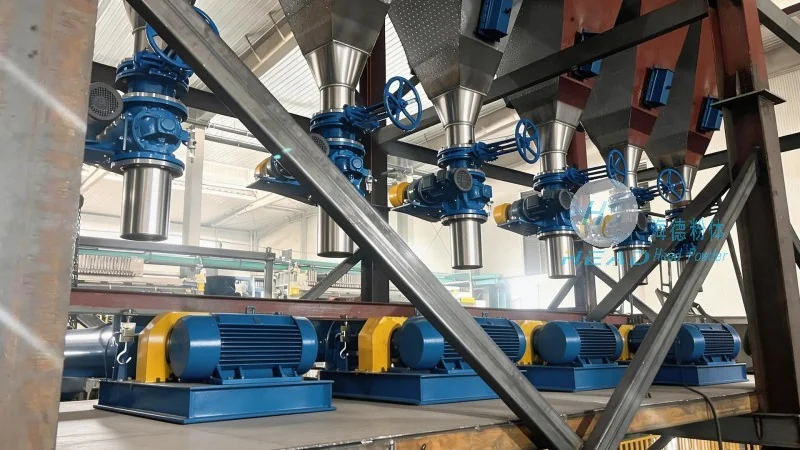
When selecting a pneumatic conveying structure for calcite, several material handling considerations must be taken into account. These include the particle size distribution, moisture content, and flowability of the calcite. Calcite particles can vary in size from fine powders to larger chunks, and the system must be designed to handle these variations effectively. Moisture content is another critical factor, as high moisture levels can lead to material caking or blockages in the conveying line. The system must be equipped with appropriate moisture control measures, such as drying units or heated pipes, to maintain optimal material flow. Flowability is also important, as calcite with poor flowability may require additional equipment, such as vibrators or agitators, to ensure smooth conveying. Additionally, the system must be designed to handle any potential dust or particulate emissions, with proper filtration and ventilation to comply with environmental regulations.
Pneumatic conveying structures for calcite are often integrated with other processing equipment, such as crushers, grinders, and classifiers. This integration allows for a seamless flow of material from the mine or storage facility to the processing unit. The system must be designed to work in harmony with these other components, ensuring that the calcite is conveyed efficiently and without interruption. Process optimization is a key aspect of pneumatic conveying, as it involves fine-tuning the system parameters to achieve the best performance. This includes adjusting the air pressure, flow rate, and material feed rate to minimize energy consumption and maximize conveying efficiency. Regular maintenance and monitoring are also essential to ensure the longevity and reliability of the system. By optimizing the pneumatic conveying process, calcite processing facilities can improve their overall productivity and reduce operational costs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top