Coal powder material handling systems are critical components in various industrial applications, particularly in power generation, cement production, and chemical processing. These systems are designed to efficiently transport coal powder from storage areas to processing units, ensuring a consistent and reliable supply of raw material. The operation process and working principle of such systems involve several key stages, each contributing to the overall efficiency and safety of the material handling operation. Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design and production of these systems, providing customized solutions tailored to the specific needs of industrial clients.
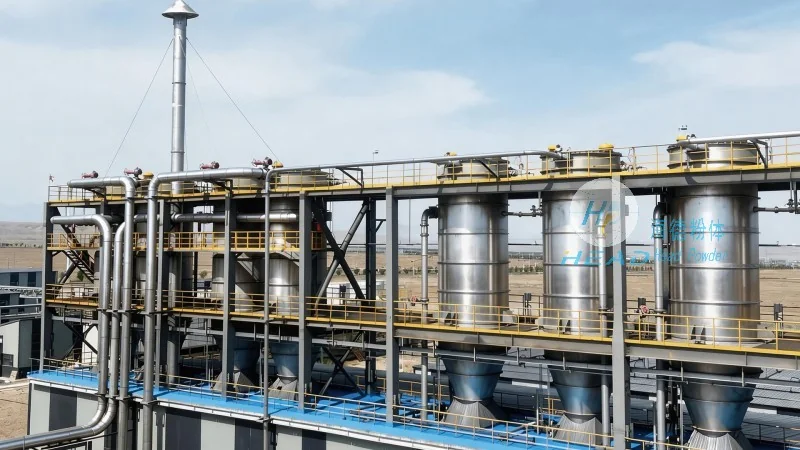
At the core of coal powder material handling systems are several essential components that work in tandem to facilitate the transport of coal powder. These components include coal feeders, conveyor belts or pneumatic conveying pipelines, dust collectors, and control systems. Each component plays a specific role in the system's operation, ensuring that coal powder is moved from its source to the processing point without loss or contamination. The coal feeder, often a rotary valve or screw conveyor, regulates the flow rate from the storage silo, while the conveyor system—whether a belt or pneumatic line—transports the material to the processing unit. Dust collectors are integrated to capture and remove airborne particles, maintaining a safe and clean environment.
The operation process of coal powder material handling systems typically begins with the storage of coal in bulk storage silos or bunkers. From there, the coal is fed into a feeder, which regulates the flow rate to the conveyor system. The feeder may be a rotary valve or a screw conveyor, depending on the system design, ensuring a steady and controlled discharge of coal powder. The conveyor system, which can be a belt conveyor or a pneumatic conveying line, then transports the coal powder to the processing unit. Pneumatic conveying systems use compressed air to move coal powder through pipelines, while belt conveyors use mechanical rollers and pulleys to move the material along a fixed path. The control system monitors flow rates, pressure, and other parameters to maintain optimal operation.
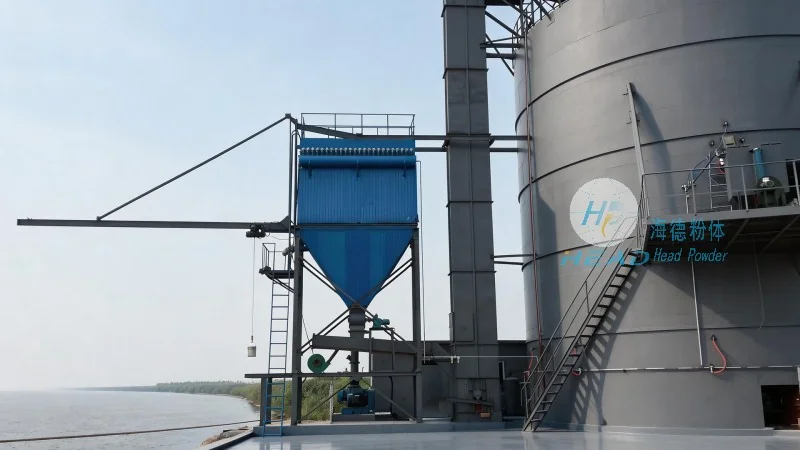
The working principle of coal powder material handling systems is based on the principles of fluid dynamics and mechanical transport. In pneumatic conveying systems, compressed air is used to create a flow that carries the coal powder through the pipeline. The air pressure is maintained at a level sufficient to overcome the resistance of the coal particles and pipeline friction. The velocity of the air and the size of the particles determine the efficiency of the conveying process. In belt conveyor systems, the principle is based on mechanical friction, where the belt moves over rollers, and the coal powder is placed on the belt and transported to the destination. The control system monitors the flow rate, pressure, and other parameters to ensure optimal operation and prevent system failures.
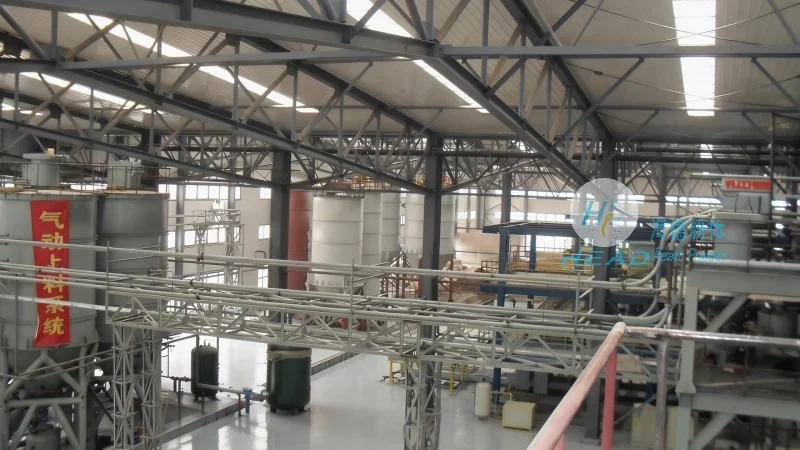
Efficiency and safety are paramount in coal powder material handling systems. The system design must consider factors such as the particle size distribution, moisture content, and bulk density of the coal to ensure effective transport. Dust control is a critical aspect, as coal dust can be hazardous and cause environmental issues. Dust collectors are integrated into the system to capture and remove dust particles from the air, ensuring a safe working environment. Additionally, the system must be equipped with safety features such as emergency stop buttons, overload protection, and temperature sensors to prevent accidents and equipment damage. Shandong HeadPowder Engineering Co., Ltd. incorporates these safety measures into their systems, adhering to industry standards and ensuring compliance with environmental regulations.
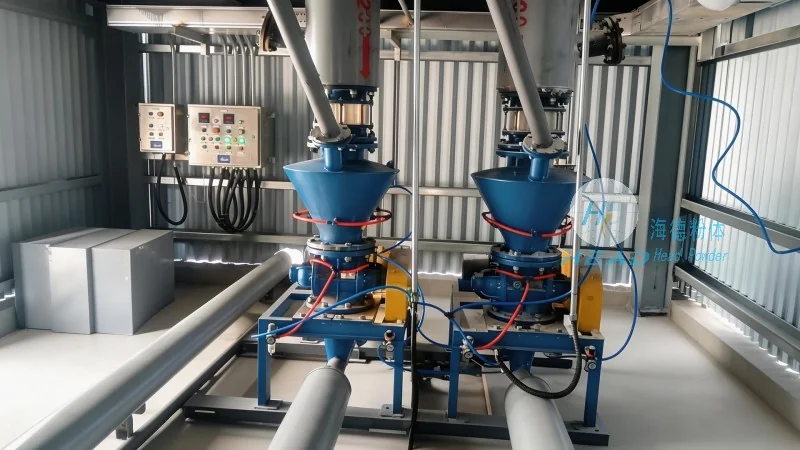
Coal powder material handling systems are widely used in various industries, including power plants, where coal is used as a fuel source. The systems provide a reliable and efficient way to transport coal from storage to the boiler, ensuring consistent fuel supply and optimal combustion. In cement production, coal is used as a fuel in the kiln, and the material handling system ensures that the coal is delivered to the kiln at the right time and in the right quantity. The benefits of these systems include improved operational efficiency, reduced labor costs, and enhanced safety. By automating the coal handling process, companies can achieve higher productivity and lower operational costs. Shandong HeadPowder Engineering Co., Ltd. has successfully implemented these systems for numerous clients, contributing to their operational excellence and cost-effectiveness.
Coal powder material handling systems are essential for the efficient and safe operation of industrial processes that rely on coal as a raw material. The operation process and working principle of these systems involve a combination of mechanical and pneumatic components, carefully designed to transport coal powder from storage to processing units. With advanced control systems and safety features, these systems ensure consistent performance and minimal downtime. As a leading manufacturer based in China, Shandong HeadPowder Engineering Co., Ltd. continues to provide high-quality coal powder handling solutions, meeting the diverse needs of industrial clients and contributing to the advancement of industrial efficiency and safety.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top