For industrial operations dealing with sintered fly ash, efficient material handling is crucial. Pneumatic conveying systems offer a reliable solution, and understanding the types, features, and application scope of these systems is essential for optimizing processes and ensuring operational efficiency. This article explores the key aspects of sintered fly ash pneumatic conveying, providing insights into the technology's capabilities and practical applications.
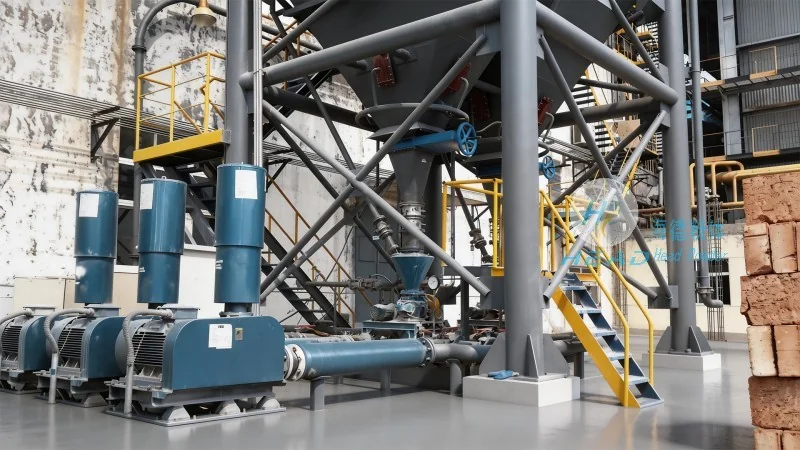
HeadPowder, a leading provider in the field of material handling solutions, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems. With a strong focus on innovation and customer-centric approaches, the company has established itself as a trusted partner for industries requiring high-performance material transport solutions. HeadPowder's expertise lies in tailoring systems to meet specific operational needs, ensuring durability, efficiency, and compliance with industry standards. The company's commitment to quality and technological advancement has enabled it to serve a diverse range of clients across various sectors.
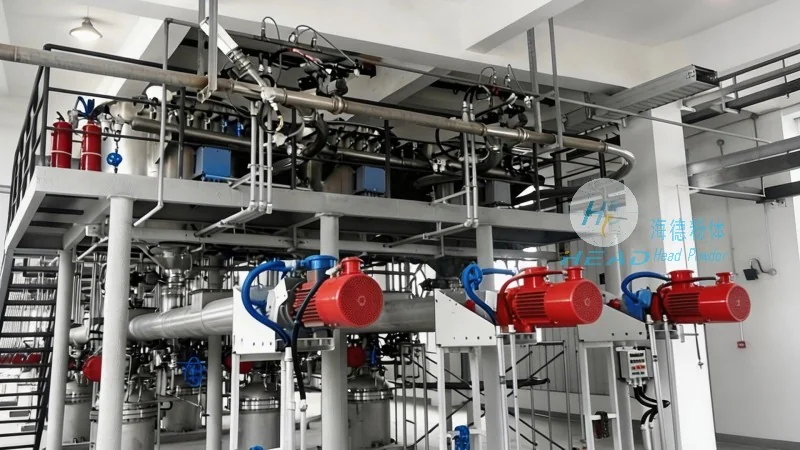
There are several types of pneumatic conveying systems used for handling sintered fly ash, each with distinct characteristics and suitability for different operational conditions. The primary categories include dense-phase and dilute-phase systems, as well as pressure and vacuum systems. Dense-phase conveying, often referred to as low-velocity conveying, involves transporting material in a semi-solid state, which minimizes particle degradation and reduces wear on system components. This method is particularly effective for handling abrasive or delicate materials like sintered fly ash, ensuring minimal product damage during transport. Dilute-phase systems, on the other hand, operate at higher velocities, using air to suspend and transport particles, making them suitable for shorter distances and less abrasive materials. Pressure systems utilize compressed air to push material through the pipeline, while vacuum systems employ suction to draw material from the source. The choice of system type depends on factors such as material properties, distance to be covered, and required throughput.
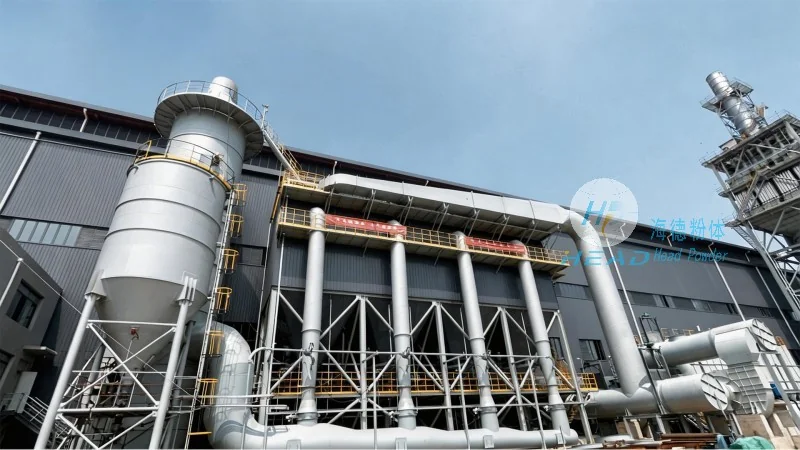
Effective sintered fly ash pneumatic conveying systems are characterized by several key features that enhance performance and reliability. One of the most significant features is the ability to handle abrasive and fine materials without excessive wear or clogging. The design of the conveying line, including the use of specialized valves and filters, ensures that particles are transported smoothly and efficiently. Another important feature is the system's adaptability to varying material flow rates and particle sizes. This flexibility allows for seamless integration into existing production lines and the ability to adjust to changing operational demands. Additionally, modern systems incorporate advanced control technologies, such as variable frequency drives and real-time monitoring, which enable precise control over conveying parameters and enhance overall operational efficiency. The use of corrosion-resistant materials in the construction of the conveying components further contributes to the longevity and reliability of the system, reducing maintenance requirements and operational downtime.
Sintered fly ash pneumatic conveying systems find extensive applications across various industries, primarily in the power generation sector where fly ash is a byproduct of coal combustion. The systems are used for transporting sintered fly ash from storage silos to disposal sites or for reusing the material in cement production. In the cement industry, sintered fly ash is often used as a supplementary cementitious material, and pneumatic conveying systems facilitate the efficient transport of this material from storage to production lines. Other applications include the handling of fly ash in industrial plants for waste management and recycling purposes. The systems are also utilized in research and development facilities where precise control over material transport is required for experimental processes. The versatility of pneumatic conveying systems makes them suitable for a wide range of applications, from large-scale industrial operations to smaller-scale laboratory settings.
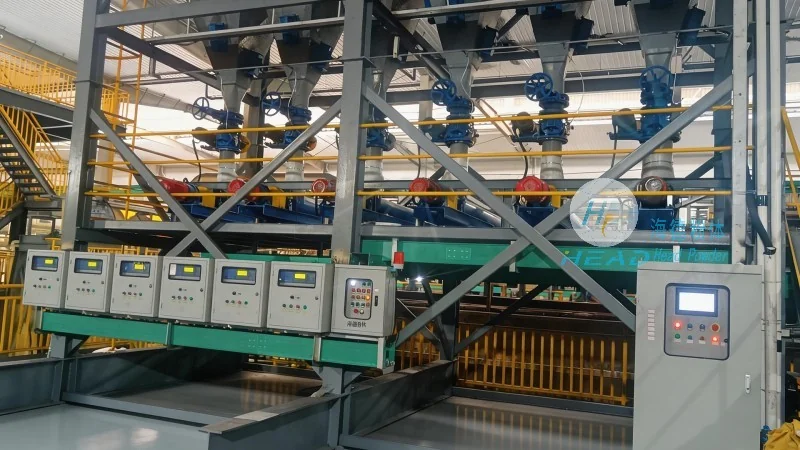
In conclusion, sintered fly ash pneumatic conveying systems offer a highly effective solution for the efficient and reliable transport of sintered fly ash. The various types of systems available, along with their distinct features and application scopes, provide industries with the flexibility to choose the most suitable solution for their specific needs. Companies like Shandong HeadPowder Engineering Co., Ltd. play a crucial role in providing these advanced systems, ensuring that industries can optimize their material handling processes and improve overall operational efficiency. By understanding the characteristics and applications of these systems, businesses can make informed decisions to enhance productivity and reduce operational costs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top