When dealing with sodium chlorate, a highly reactive chemical, the method of material handling is critical to ensure efficiency, safety, and environmental compliance. Pneumatic conveying systems have emerged as a preferred solution for transporting sodium chlorate powder due to their ability to handle fine powders with minimal dust generation and high operational efficiency. This article provides an in-depth analysis of the classification of these systems and their practical applications in various industrial settings.
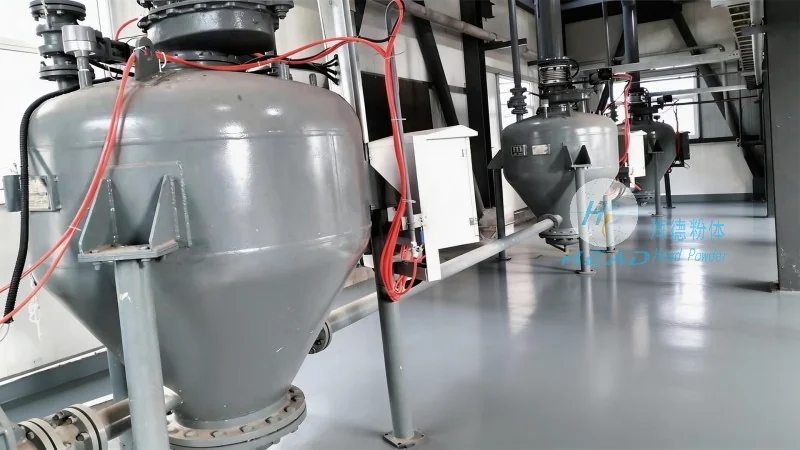
Pneumatic conveying systems for sodium chlorate are categorized based on the air velocity and pressure used during the conveying process. The two primary classifications are dilute-phase and dense-phase systems. Dilute-phase systems operate at low to moderate pressure and high air velocity, typically used for short to medium distances and low to medium material flow rates. These systems are suitable for applications where the material is relatively dry and free-flowing. Dense-phase systems, conversely, utilize higher pressure and lower air velocity to transport material in a more concentrated form, making them ideal for longer distances and higher material loads. The choice between these systems depends on factors such as the distance between the source and destination, the required material throughput, and the physical properties of the sodium chlorate powder.
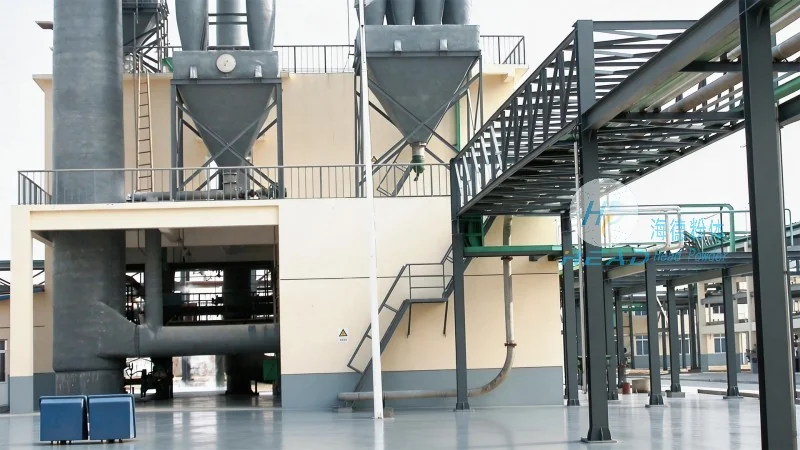
The effective operation of a sodium chlorate pneumatic conveying system relies on several essential components. The material feeder is the first component, responsible for controlling the flow rate of sodium chlorate into the system, ensuring a consistent and controlled feed. The conveying line, often made of stainless steel or other corrosion-resistant materials, transports the material and air mixture. A separator, typically a cyclone or bag filter, is used to separate the sodium chlorate powder from the air, allowing the material to be collected in a hopper or storage bin. The dust collector then captures any fine particles that may have escaped the separator, preventing air pollution and ensuring compliance with environmental regulations. Finally, a blower or compressor provides the necessary air pressure to move the material through the system, with the pressure and air volume adjusted based on the system's requirements.
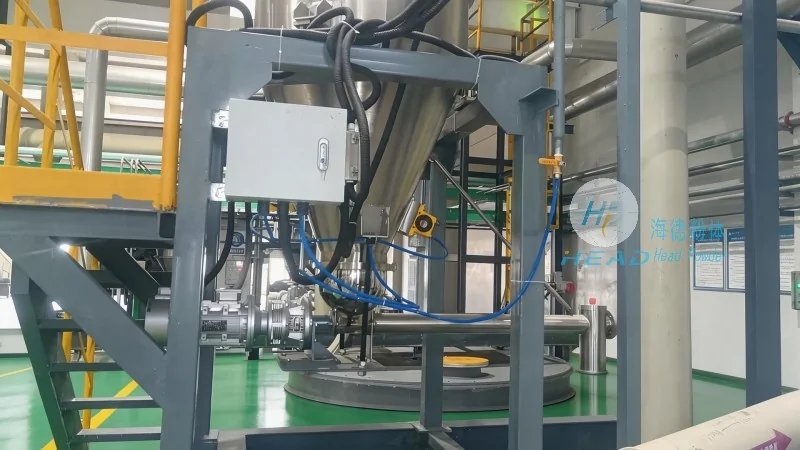
Sodium chlorate is widely utilized in multiple industries, including the chemical manufacturing sector, where it is used as an intermediate in the production of chlorine and other chemicals. In the paper and pulp industry, it serves as a bleaching agent, enhancing the whiteness and quality of paper products. The food industry also uses sodium chlorate as a disinfectant and preservative. The pneumatic conveying system is particularly advantageous in these applications as it minimizes the risk of dust exposure and contamination. For instance, in chemical plants, the system efficiently transports sodium chlorate from storage silos to reactors, ensuring a continuous supply without the need for manual handling. In paper mills, the system delivers sodium chlorate to bleaching towers, maintaining the quality of the bleaching process and reducing downtime. The ability to handle fine powders without causing dust explosions makes the pneumatic conveying system a safer and more reliable option compared to traditional methods like bucket elevators or belt conveyors.
Employing a pneumatic conveying system for sodium chlorate offers several significant advantages. Firstly, it significantly reduces material loss and contamination, as the material is contained within the pipeline throughout the conveying process. This is crucial for sodium chlorate, which is a valuable and potentially hazardous chemical. Secondly, the system minimizes the risk of dust explosions by maintaining the material in a controlled environment, preventing the accumulation of fine particles that could ignite. Thirdly, it enhances operational efficiency by allowing for continuous and automated material transport, reducing labor costs and increasing production throughput. Additionally, the system is highly flexible and can be easily integrated with existing plant layouts, adapting to changes in production requirements without major modifications. Finally, the use of corrosion-resistant materials in the system ensures long-term durability and low maintenance costs, making it a cost-effective solution for long-term operations.
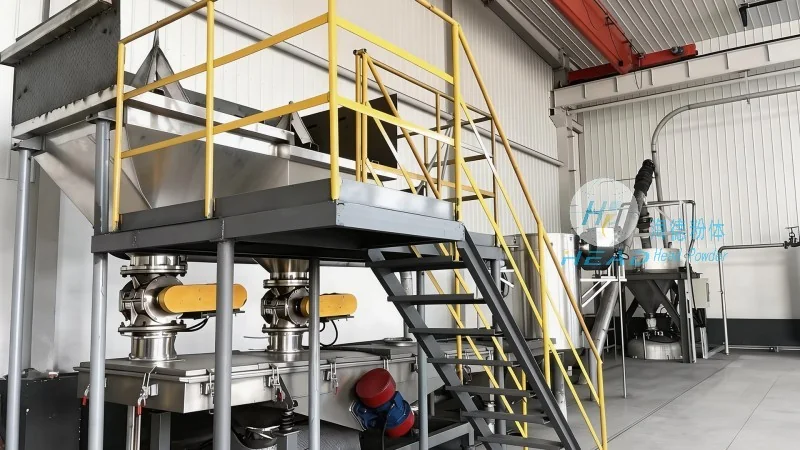
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a reputable company specializing in the design, manufacturing, and supply of pneumatic conveying systems and related equipment. HeadPowder has built a strong reputation in the industry by focusing on innovation, quality, and customer satisfaction. The company's headquarters is located in Shandong, China, and they have a team of experienced engineers and technicians who are dedicated to developing customized solutions for their clients. HeadPowder's expertise lies in understanding the unique challenges of handling sodium chlorate and other fine powders, and they provide tailored systems that meet the specific needs of each application. The company adheres to international standards and uses advanced manufacturing techniques to ensure that their products are reliable, efficient, and safe. With a commitment to continuous improvement, HeadPowder aims to be a leading provider of pneumatic conveying solutions in the global market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top