Understanding PFA Pneumatic Conveying Systems and Their Applications, presented by Shandong HeadPowder Engineering Co., Ltd. (headpowder), a leading provider of industrial material handling solutions. PFA is a fluoropolymer widely used in industrial applications due to its excellent chemical resistance, thermal stability, and non-stick properties. When integrated into pneumatic conveying systems, PFA components enhance the performance and durability of these systems, especially for handling materials that are abrasive, corrosive, or sensitive to moisture. Pneumatic conveying, in general, is a method of transporting bulk materials through a pipeline using air or other gases as the conveying medium. It offers advantages such as flexibility in layout, ability to transport materials over long distances, and reduced exposure to contaminants compared to mechanical conveying methods.
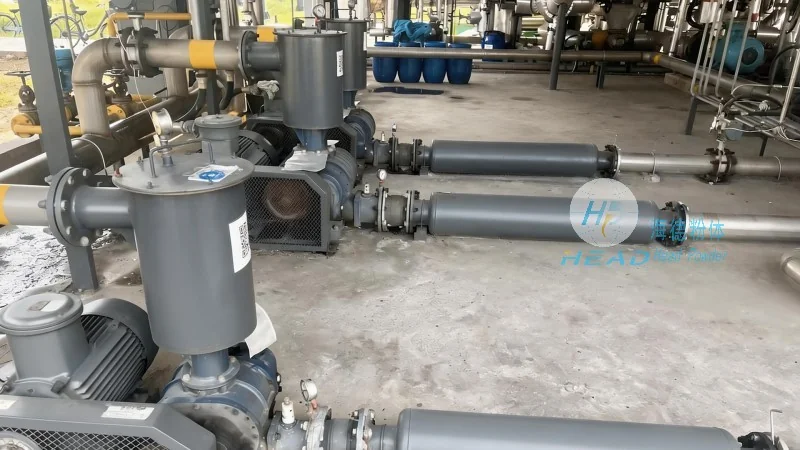
Polytetrafluoroethylene (PFA) is a fluoropolymer widely used in industrial applications due to its excellent chemical resistance, thermal stability, and non-stick properties. When integrated into pneumatic conveying systems, PFA components enhance the performance and durability of these systems, especially for handling materials that are abrasive, corrosive, or sensitive to moisture. Pneumatic conveying, in general, is a method of transporting bulk materials through a pipeline using air or other gases as the conveying medium. It offers advantages such as flexibility in layout, ability to transport materials over long distances, and reduced exposure to contaminants compared to mechanical conveying methods.
The core components of a PFA pneumatic conveying system typically include a material hopper, a feeder (often a rotary valve or screw feeder), a conveying line (usually made of PFA or compatible materials), a venturi or airlock for material discharge, and a dust collector or filter system. The PFA material, often in the form of tubing or fittings, is chosen for its resistance to high temperatures and aggressive chemicals, making it suitable for handling a wide range of powders and granules. The system operates by creating a pressure differential, either by suction (in suction-type systems) or by pressure (in pressure-type systems), to move the material through the pipeline.
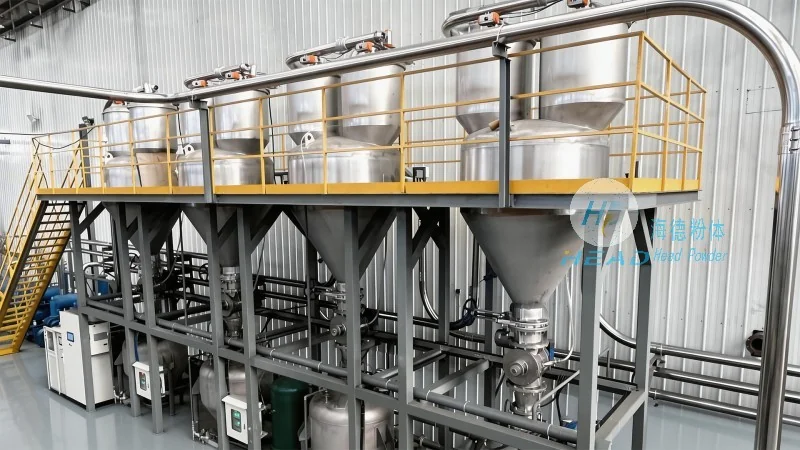
Pneumatic conveying systems are generally classified into two main categories: suction (or negative pressure) systems and pressure (or positive pressure) systems. Suction systems operate by creating a vacuum at the material discharge point, drawing material from the source into the conveying line. These systems are ideal for applications where the material source is at a higher elevation than the discharge point, as they can pull material up and over obstacles. Pressure systems, on the other hand, use compressed air to push material through the pipeline from the source to the discharge point. They are suitable for applications where the material source is at a lower elevation or when the material needs to be transported over long distances under pressure.
PFA pneumatic conveying systems are widely used in various industries, including chemical, pharmaceutical, food processing, and aerospace. In the chemical industry, they are used to transport corrosive powders and granules, such as acids and bases, where PFA's chemical resistance is crucial. In the pharmaceutical industry, PFA systems are preferred for handling sensitive materials like active pharmaceutical ingredients (APIs) and excipients, as they prevent contamination and ensure product purity. The food processing industry utilizes PFA systems for conveying food powders and granules, such as sugar, flour, and spices, due to PFA's non-stick and hygienic properties. In the aerospace industry, PFA systems are used for transporting high-purity powders and granules used in the manufacturing of aerospace components, where cleanliness and material integrity are paramount.
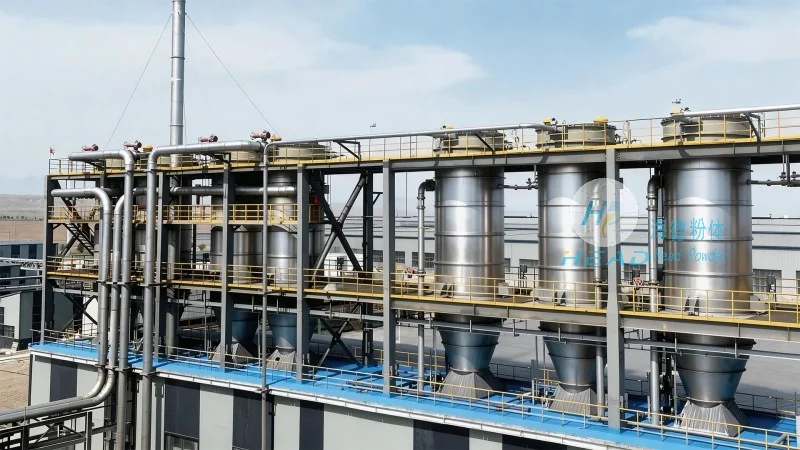
Compared to traditional mechanical conveying methods, PFA pneumatic conveying systems offer several advantages. First, they provide a more hygienic and clean environment, as the material is contained within a sealed pipeline, reducing the risk of contamination. Second, they are more flexible in terms of layout, allowing for easy integration into existing facilities or new plant designs. Third, PFA materials are resistant to high temperatures and aggressive chemicals, extending the lifespan of the system and reducing maintenance costs. Fourth, PFA systems can handle a wide range of materials, from fine powders to large granules, without the need for additional equipment like crushers or screens.
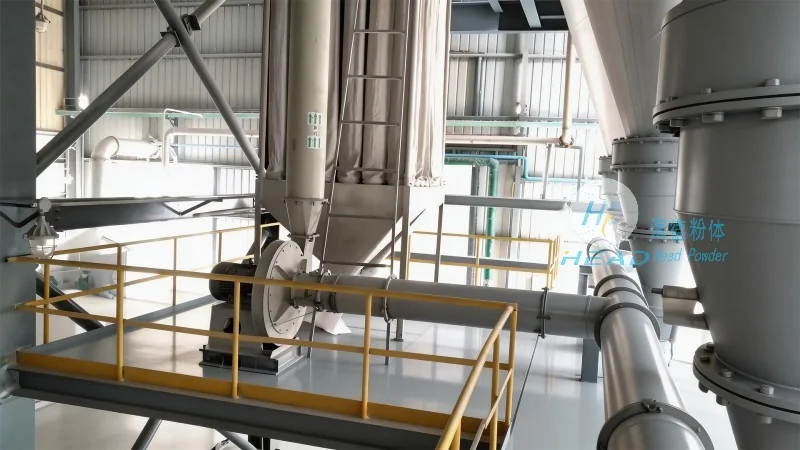
When implementing a PFA pneumatic conveying system, several factors need to be considered to ensure optimal performance and longevity. First, the material being conveyed must be compatible with PFA components, as some materials may cause degradation over time. Second, the system design must account for the material's flow properties, such as bulk density and particle size, to ensure efficient conveying. Third, the system must be properly sized to handle the required material flow rate and pressure differential. Fourth, regular maintenance, including cleaning and inspection of PFA components, is essential to prevent clogging and ensure consistent performance. By addressing these considerations, industries can maximize the benefits of PFA pneumatic conveying systems and achieve operational efficiency.
PFA pneumatic conveying systems represent a reliable and efficient solution for transporting bulk materials in various industrial applications. With their excellent chemical resistance, thermal stability, and non-stick properties, PFA components enhance the performance and durability of these systems. The classification of pneumatic conveying systems, including suction and pressure types, allows for flexibility in design to suit different material handling requirements. The applications of PFA systems span multiple industries, from chemical and pharmaceutical to food processing and aerospace, where material purity and integrity are critical. By understanding the key components, advantages, and considerations of PFA pneumatic conveying systems, industries can make informed decisions to improve their material handling processes and achieve operational efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top