For the efficient transportation of river sand, specialized material handling systems are essential. These systems are designed to ensure the smooth and safe movement of sand from extraction sites to processing or storage facilities. This article provides a detailed overview of the operation process and working principle of a typical river sand material handling system, highlighting the key components, operational steps, and technical advantages that contribute to its effectiveness.
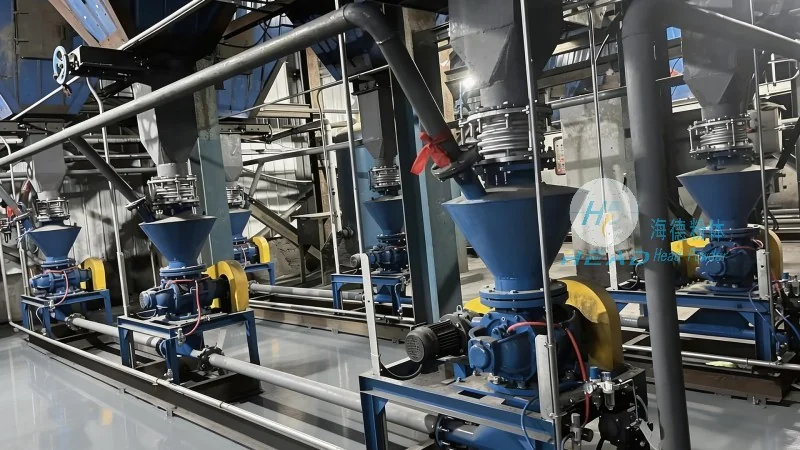
The river sand material handling system is a critical infrastructure in the sand and gravel industry, facilitating the efficient transfer of sand from natural sources to industrial applications. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and implementation of such systems. With a strong presence in China, particularly in Shandong, the company leverages advanced engineering solutions to meet the diverse needs of clients in the construction and mining sectors. The system's design incorporates robust materials and intelligent control mechanisms to ensure high efficiency, reliability, and safety during operation.
The river sand material handling system typically consists of several interconnected components, each playing a vital role in the overall operation. The primary components include conveyors, feeders, storage bins, and control systems. Conveyors, such as belt conveyors or screw conveyors, are responsible for transporting the sand over long distances. Feeders regulate the flow of sand from the source to the conveyor, ensuring a consistent and controlled feed rate. Storage bins are used to temporarily hold the sand, allowing for buffer storage and smooth operation during peak demand periods. The control system integrates all components, monitoring and adjusting operations based on real-time data to optimize performance and prevent issues like overloading or blockages.
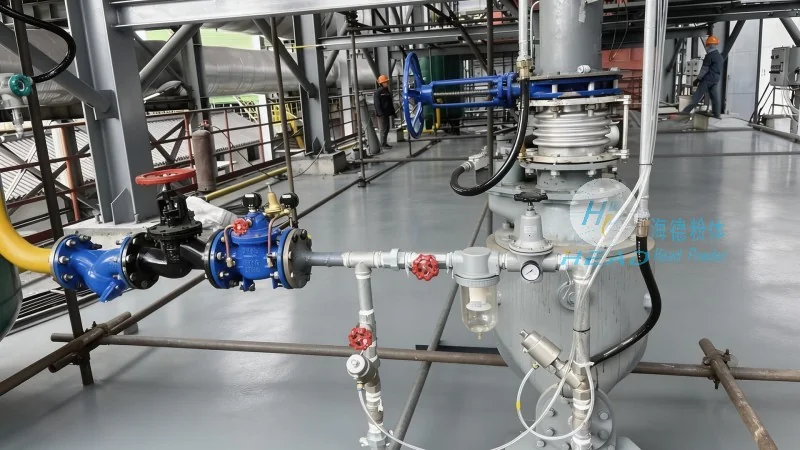
The operation process of the river sand material handling system begins with the extraction of sand from the riverbed or quarry. The sand is then fed into a hopper or feeder, where it is evenly distributed and directed towards the conveyor system. The conveyor transports the sand to the processing or storage area, where it may undergo further treatment or be stored for later use. Throughout the process, the control system continuously monitors the flow rate, pressure, and other parameters to ensure that the system operates within safe and efficient limits. In case of any anomalies, such as a blockage or overload, the system automatically triggers alerts or corrective actions to maintain smooth operation. The entire process is designed to be automated, reducing the need for manual intervention and minimizing the risk of accidents or inefficiencies.
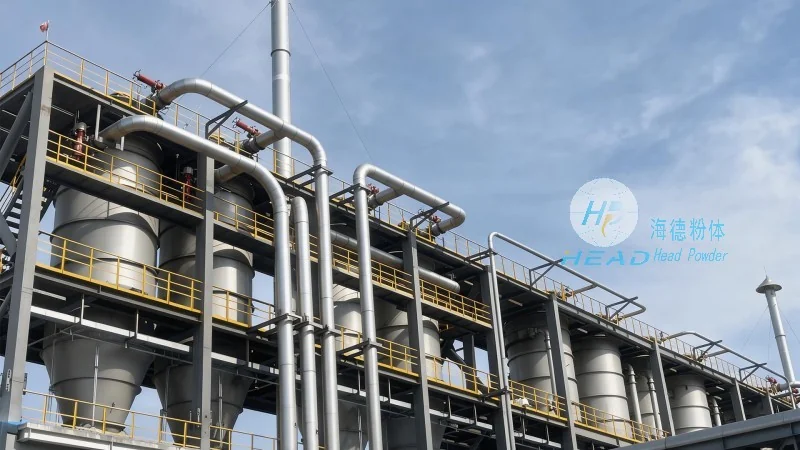
The working principle of the river sand material handling system is based on the principles of mechanical transport and material flow control. The system utilizes gravity and mechanical force to move the sand from the source to the destination. The conveyor belt, for example, uses friction and tension to move the sand along its path. The feeder regulates the flow by adjusting the opening size or speed, ensuring a consistent feed rate. The storage bin acts as a buffer, maintaining a steady supply of sand even when the conveyor is temporarily stopped or during maintenance. The control system employs sensors and feedback mechanisms to adjust the speed of the conveyor and feeder, optimizing the flow rate based on the demand and the condition of the system. This closed-loop control system ensures that the system operates at its peak efficiency, minimizing energy consumption and maximizing throughput.
The river sand material handling system developed by Shandong HeadPowder Engineering Co., Ltd. offers several technical advantages that make it suitable for various applications. The system's robust design ensures durability and long service life, even under harsh operating conditions. The use of high-quality materials and advanced manufacturing techniques enhances the system's resistance to wear and corrosion, reducing maintenance costs and downtime. The intelligent control system provides real-time monitoring and data analysis, enabling operators to make informed decisions and optimize performance. The system is also highly adaptable, capable of handling different types of sand and accommodating varying production demands. These advantages make the system suitable for a wide range of applications, including sand processing plants, construction sites, and mining operations. Whether for large-scale industrial use or smaller-scale projects, the system provides reliable and efficient sand transportation solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top