Stabilizer powders are critical components in various industrial processes, and their efficient bulk handling is essential for maintaining production efficiency and product quality. Pneumatic conveying has emerged as a highly effective method for transporting these powders, offering advantages such as low maintenance, minimal product contamination, and the ability to handle a wide range of materials. This article explores the application of pneumatic conveying in the bulk transport of stabilizer powders, highlighting the technical solutions provided by Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field.
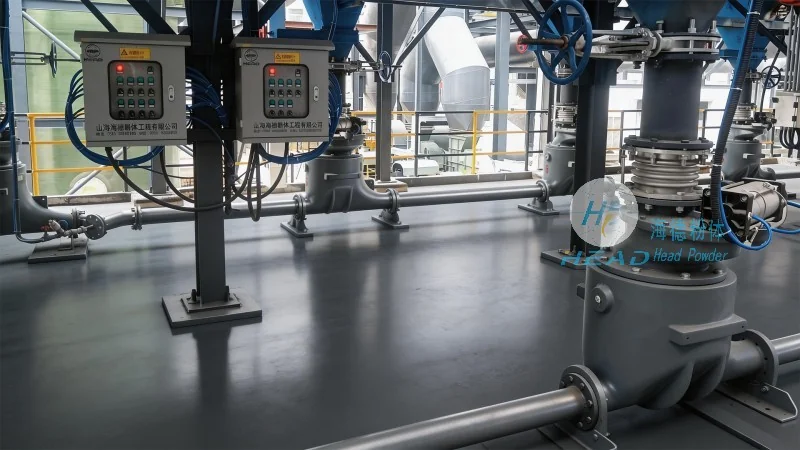
Pneumatic conveying systems utilize air or gas to transport bulk materials through a pipeline network. For stabilizer powders, which often require precise control and minimal degradation, the choice of conveying system is crucial. Traditional methods like belt conveyors or bucket elevators may introduce contamination or cause particle degradation due to friction and impact. In contrast, pneumatic conveying offers a closed system that protects the material from external factors, ensuring that the stabilizer's properties remain intact throughout the transport process. The system typically consists of a material feed hopper, a conveyor line, and a discharge unit, with the air flow controlled to maintain the desired velocity and pressure. This technology allows for flexible and scalable solutions, adapting to different production volumes and plant layouts.
When applied to stabilizer powders, pneumatic conveying provides several key benefits that enhance operational performance. First, it minimizes product contamination by isolating the material from the environment and other process streams. This is particularly important for stabilizers used in pharmaceuticals, food, or cosmetics, where purity is non-negotiable. Second, the system reduces the risk of material degradation, as the enclosed pipeline prevents exposure to moisture, dust, or other contaminants that could alter the powder's properties. Third, pneumatic conveying offers energy efficiency compared to some mechanical systems, as the air flow can be optimized to minimize power consumption while maintaining effective transport. Additionally, the technology allows for easy integration with other process equipment, such as mixing or packaging systems, enabling seamless flow from storage to end-use. These advantages make pneumatic conveying an ideal choice for industries that demand high standards of product integrity and operational reliability.
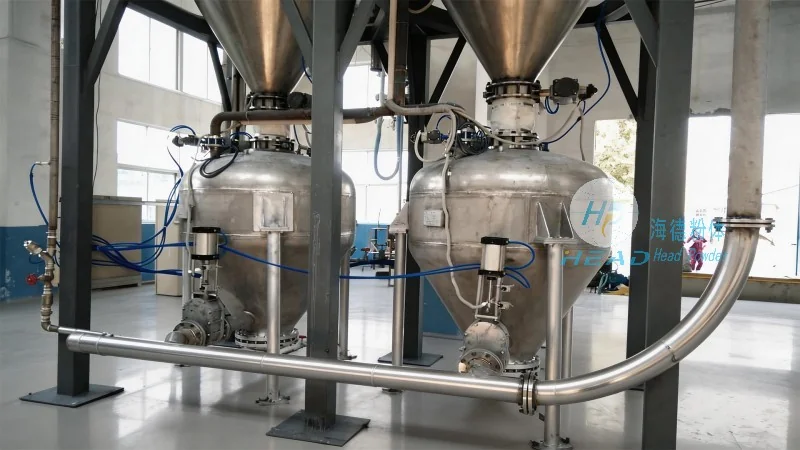
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and implementing customized pneumatic conveying solutions tailored to the unique needs of stabilizer powder applications. The company's expertise lies in understanding the specific characteristics of different stabilizer powders, such as particle size, density, and flowability, and selecting the appropriate conveying technology accordingly. For example, for fine, cohesive powders that are prone to caking, HeadPowder may recommend a pressure system with positive displacement blowers, which provides consistent air pressure to prevent blockages. For bulkier, free-flowing powders, a vacuum system with a rotary valve feeder might be more suitable, offering flexibility in material handling. The company's engineers work closely with clients to assess their existing infrastructure, production requirements, and budget constraints, ensuring that the final solution is both effective and cost-efficient. HeadPowder also provides ongoing support and maintenance services to ensure the longevity and optimal performance of the conveying systems, addressing any issues that may arise during operation.
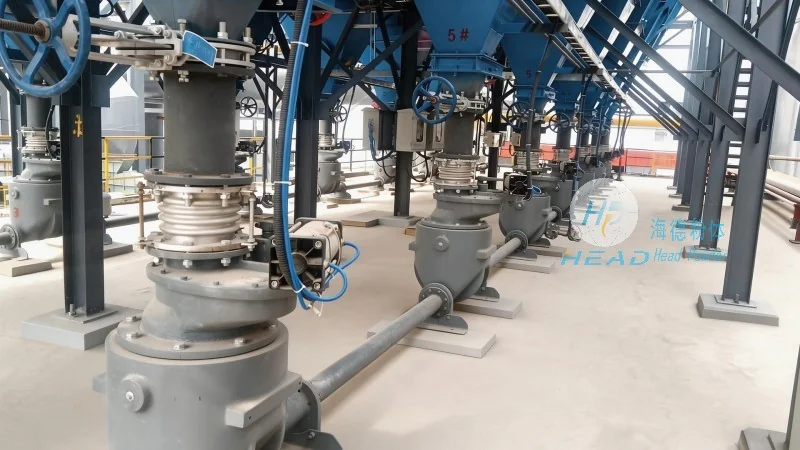
HeadPowder has successfully implemented pneumatic conveying systems for numerous clients in the stabilizer industry, demonstrating the technology's effectiveness in real-world scenarios. One notable case involved a pharmaceutical manufacturer that required the transport of a sensitive stabilizer powder from storage silos to a mixing line. The existing system was prone to blockages and contamination, leading to production downtime and quality issues. HeadPowder designed a new pressure pneumatic conveying system with a closed-loop air filtration system, which eliminated the risk of contamination and reduced downtime by 60%. The system was integrated with the client's existing control system, allowing for automated operation and real-time monitoring of material flow. Another case involved a food processing company that needed to transport a stabilizer powder used in beverage production. The company required a system that could handle varying production volumes and maintain product freshness. HeadPowder's solution included a combination of pressure and vacuum conveying sections, with a variable speed drive to adjust air flow based on demand. This flexibility allowed the client to scale production without compromising product quality or efficiency.
Pneumatic conveying is a proven and reliable technology for the bulk handling of stabilizer powders, offering significant advantages in terms of product protection, operational efficiency, and flexibility. Shandong HeadPowder Engineering Co., Ltd. stands as a trusted partner in providing customized solutions that meet the specific needs of clients in the stabilizer industry. With a focus on technical expertise, customer satisfaction, and long-term partnerships, HeadPowder continues to deliver high-quality pneumatic conveying systems that enhance the performance and reliability of industrial processes. For more information about their services or to discuss a specific project, please contact Shandong HeadPowder Engineering Co., Ltd., located in Shandong, China.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top