For industries dealing with bentonite, selecting the right material handling solution is crucial for efficiency and cost-effectiveness. Pneumatic conveying systems have emerged as a versatile and efficient method for transporting bentonite, offering advantages such as reduced labor costs, minimized product contamination, and enhanced safety in handling. This article explores the various types of pneumatic conveying systems used in bentonite transport and their practical applications, highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd. in providing tailored solutions for this industry.
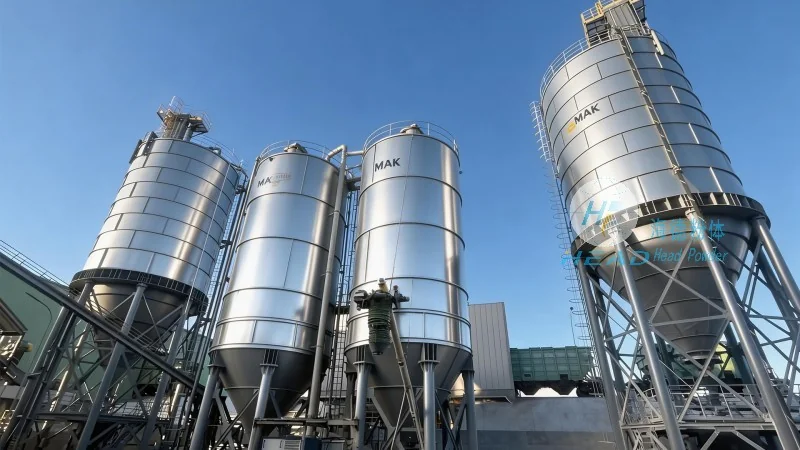
Pneumatic conveying systems utilize air or gas to transport bulk materials like bentonite through a pipeline. These systems are categorized based on the direction of air flow and the method of material transport. The primary types include pressure, vacuum, and mixed flow systems, each with distinct characteristics suited to different operational needs.
1. Pressure Pneumatic Conveying: This system operates by forcing air and material through the pipeline under pressure. It is ideal for long-distance transport and can handle abrasive materials like bentonite without causing excessive wear. The system typically includes a positive displacement blower or compressor, a hopper for material storage, and a discharge point at the destination. Pressure systems are known for their high efficiency and ability to transport materials over significant distances, making them suitable for large-scale bentonite operations.
2. Vacuum Pneumatic Conveying: In contrast, vacuum systems draw material into the pipeline using a vacuum created by a fan or ejector. This method is often preferred for short-distance transport or when material needs to be collected from multiple points. Vacuum systems are gentle on the material, reducing the risk of degradation or particle breakage, which is particularly important for bentonite, a fine powder that can be sensitive to handling. They are commonly used in applications where the material is sourced from various locations and needs to be consolidated into a central processing unit.
3. Mixed Flow Pneumatic Conveying: A hybrid approach combining both pressure and vacuum principles, mixed flow systems offer flexibility in handling different material characteristics and operational requirements. They can be configured to operate under pressure or vacuum as needed, providing adaptability for varied bentonite transport scenarios. This versatility makes mixed flow systems a popular choice for industries that require both long-distance and short-distance transport capabilities, or when the material flow rate needs to be adjusted dynamically.
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and implementing pneumatic conveying systems tailored to the specific needs of bentonite processing facilities. The company's expertise ensures that the chosen system maximizes efficiency while minimizing operational costs. Practical applications of these systems include:
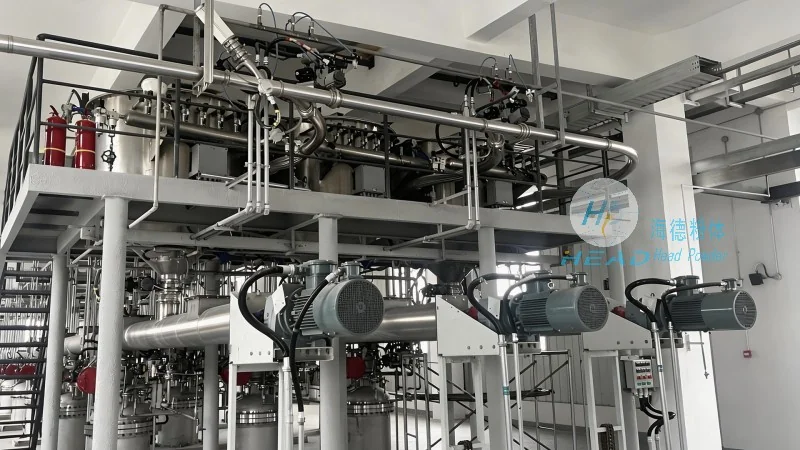
1. Raw Material Handling: In bentonite mining and processing plants, pneumatic conveying systems are used to transport raw bentonite from storage silos or stockpiles to processing equipment. This method eliminates the need for manual handling or heavy machinery, reducing the risk of dust exposure and improving workplace safety. The systems can handle large volumes of material, ensuring a steady supply of raw bentonite for production.
2. Process Integration: During the manufacturing of bentonite-based products, such as drilling muds or cat litter, pneumatic conveying is used to transfer processed materials between different stages of production. For example, after the bentonite has been mixed with other additives, the mixture is conveyed to a drying or packaging unit. This seamless integration of processes enhances productivity and maintains consistent product quality.
3. Storage and Distribution: Pneumatic conveying systems are also employed in the storage and distribution of finished bentonite products. They can transport the material from production facilities to storage silos or directly to customers, ensuring that the product remains intact and free from contamination. The systems are particularly useful for transporting fine powders, as they prevent the material from settling or caking in the pipeline, which could affect the quality of the final product.
Implementing pneumatic conveying systems for bentonite transport offers several key benefits that contribute to operational excellence. These include:
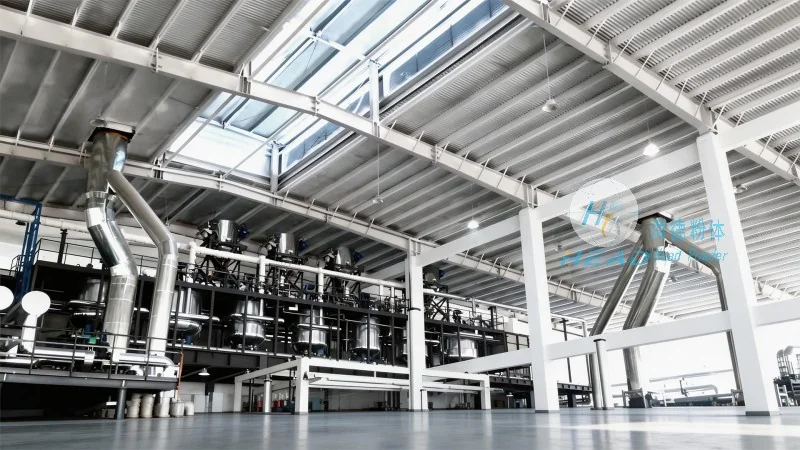
1. Enhanced Safety: By eliminating the need for manual handling and reducing exposure to dust, pneumatic systems create a safer working environment. This is especially important for bentonite, which can cause respiratory issues if inhaled in large quantities. The enclosed system also prevents dust from spreading into the surrounding environment, minimizing the risk of environmental contamination.
2. Cost Efficiency: Pneumatic conveying reduces labor costs associated with manual material handling and minimizes equipment wear compared to traditional methods like truck or conveyor belt transport. The systems are energy-efficient, with modern designs utilizing less power while maintaining high transport rates. This leads to long-term cost savings for bentonite processing facilities.
3. Product Quality Preservation: The enclosed nature of pneumatic systems prevents the bentonite from coming into contact with external contaminants, such as moisture or other materials. This ensures that the product remains in its original state, maintaining its quality and performance characteristics. For applications like drilling muds, where the properties of bentonite are critical, this preservation of quality is essential.
4. Flexibility and Scalability: Pneumatic conveying systems can be easily scaled to accommodate changes in production volume or operational requirements. Whether a facility needs to increase its transport capacity or expand its processing capabilities, the system can be modified or upgraded without significant disruption. This flexibility allows bentonite producers to adapt to market demands and grow their operations efficiently.
Pneumatic conveying systems represent a sophisticated and effective solution for the transport of bentonite, offering a range of benefits from enhanced safety and cost efficiency to product quality preservation. Shandong HeadPowder Engineering Co., Ltd. leverages its expertise in designing and implementing these systems to meet the unique needs of bentonite processing industries. By selecting the appropriate type of pneumatic conveying system and optimizing its operation, companies can achieve improved operational performance and competitive advantages in the market. As the demand for bentonite continues to grow, the role of efficient material handling systems like pneumatic conveyors becomes increasingly vital in ensuring the smooth and sustainable operation of bentonite processing facilities.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top