HeadPowder, a leading provider of material handling solutions, specializes in the efficient transportation of various bulk materials, including manganese silicate. In the realm of pneumatic conveying, two primary methods dominate: positive pressure and negative pressure systems. This article delves into the nuances of these two approaches, examining their applications, advantages, and limitations when applied to the transport of manganese silicate. By understanding the differences between positive and negative pressure conveying, industries can make informed decisions to optimize their material handling processes.
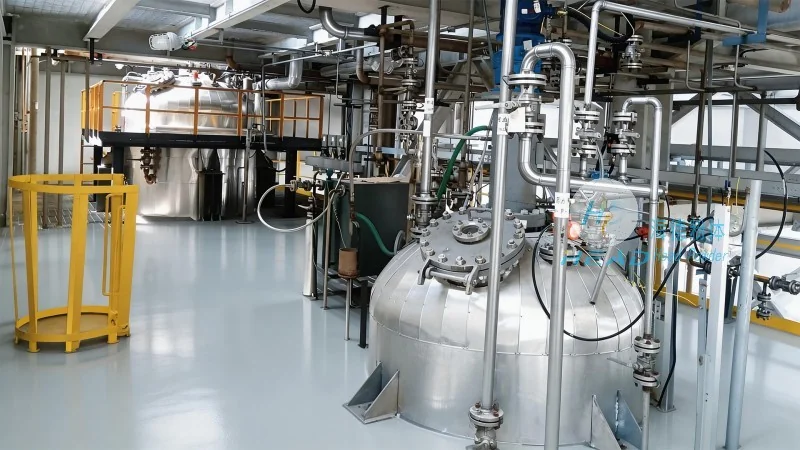
Manganese silicate is a versatile industrial material used in applications ranging from chemical manufacturing to construction. Its handling requires specialized equipment to ensure safety, efficiency, and product integrity. Pneumatic conveying, which uses air or gas to move bulk materials, offers a non-contact method of transport that minimizes contamination and damage to the material. For manganese silicate, the choice between positive and negative pressure systems is critical, as each method presents distinct characteristics that influence system design, operational costs, and overall performance.
Positive pressure pneumatic conveying systems operate by blowing air or gas into the conveying line, creating a pressure higher than the ambient air pressure. This method forces the material to move through the system, typically using a blower or positive displacement pump as the primary power source. The system is often closed, with the conveying line connected to the material source and discharge point, ensuring that the air and material are contained within the system.
For manganese silicate, positive pressure conveying is particularly effective when dealing with fine powders or granules that are prone to dusting or caking. The high-pressure air helps to maintain the material's flowability and prevents blockages in the conveying line. Additionally, positive pressure systems are well-suited for long-distance transport, as the pressure can be maintained throughout the entire length of the line, ensuring consistent material movement. However, these systems require robust seals and filtration to prevent air leakage and dust emissions, which can be a challenge in industrial settings.
One of the key advantages of positive pressure conveying is its ability to handle high-volume material transport with minimal pressure loss. The system can efficiently move large quantities of manganese silicate over considerable distances, making it ideal for large-scale production facilities. Another benefit is the reduced risk of material degradation, as the enclosed system prevents exposure to external contaminants and moisture. Furthermore, positive pressure systems are generally more forgiving when it comes to variations in material properties, such as changes in particle size or moisture content, as the high pressure helps to maintain consistent flow rates.
Despite its advantages, positive pressure conveying has several limitations. The most significant challenge is the need for high-pressure air or gas, which increases energy consumption and operational costs. The system also requires regular maintenance of the blower and seals to prevent air leakage and ensure efficient operation. Additionally, positive pressure systems may be less effective for transporting materials with high moisture content or those that are prone to agglomeration, as the high pressure can sometimes exacerbate these issues. Finally, the system's design is more complex, requiring precise engineering to ensure proper air distribution and material flow.
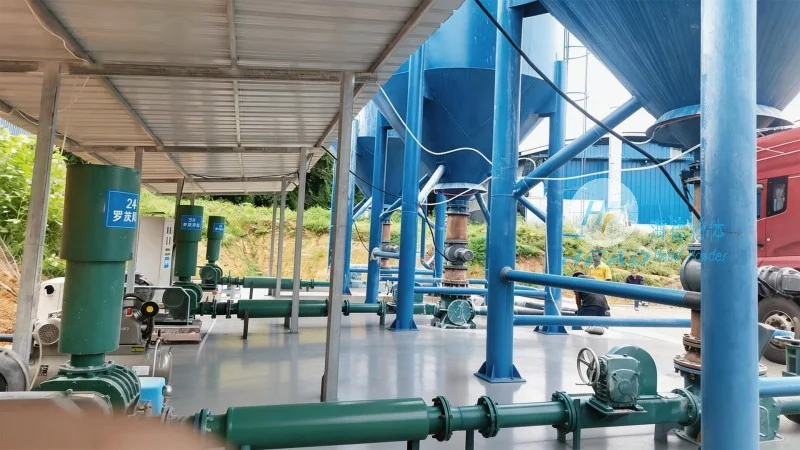
Negative pressure pneumatic conveying, also known as suction or vacuum conveying, operates by creating a vacuum in the conveying line, which draws the material from the source into the system. The material is then transported to the discharge point using the vacuum created by a vacuum pump or fan. Unlike positive pressure systems, negative pressure systems do not force the material through the line but rather pull it in, making them more suitable for short to medium-distance transport.
For manganese silicate, negative pressure conveying is often preferred when dealing with materials that are less abrasive or when the material source is located at a higher elevation than the discharge point. The vacuum system is also effective for handling materials that are prone to dusting, as the enclosed line prevents dust from escaping into the environment. However, negative pressure systems are generally less efficient for long-distance transport, as the vacuum can be lost over longer distances, leading to reduced material flow rates.
One of the primary advantages of negative pressure conveying is its lower energy consumption compared to positive pressure systems. The vacuum pump requires less power to operate, resulting in reduced operational costs. Another benefit is the system's simplicity, as it typically consists of fewer components and requires less maintenance. Negative pressure systems are also well-suited for handling materials that are sensitive to pressure, as the low pressure environment minimizes the risk of material degradation. Additionally, the system is easier to install and modify, making it a flexible option for changing production needs.
Despite its advantages, negative pressure conveying has its own set of challenges. The most significant limitation is its inefficiency for long-distance transport, as the vacuum can be lost over longer distances, reducing material flow rates. The system is also more susceptible to blockages, as the material is drawn into the line and may accumulate if the flow is interrupted. Additionally, negative pressure systems require careful design to prevent air leakage, as even small leaks can significantly reduce the vacuum level and impact material transport. Finally, the system may not be suitable for handling high-volume material, as the vacuum pump may not be able to maintain sufficient suction for large quantities.
When comparing positive and negative pressure pneumatic conveying for manganese silicate, several factors must be considered to determine the most suitable system. The primary decision points include the distance of transport, the volume of material to be moved, the material properties (such as particle size, moisture content, and abrasiveness), and the operational budget. Positive pressure systems are generally preferred for long-distance, high-volume transport, while negative pressure systems are better suited for short to medium distances and lower material volumes.
From an energy perspective, negative pressure systems are more efficient for shorter distances, but positive pressure systems offer better performance for longer distances. The choice also depends on the material's sensitivity to pressure and the risk of contamination. Manganese silicate, being a fine powder, is more likely to benefit from the enclosed environment of positive pressure systems, which minimizes dust exposure. However, if the material source is at a higher elevation, negative pressure conveying may be more practical due to the vacuum's ability to draw material upward.
Industrial applications of manganese silicate often require customized pneumatic conveying solutions. For example, in a chemical manufacturing plant, positive pressure conveying may be used to transport manganese silicate from a storage silo to a processing unit over a distance of several hundred meters. The high-pressure system ensures consistent material flow and prevents blockages, while the enclosed design maintains product integrity. In contrast, a construction materials plant may use negative pressure conveying to transport manganese silicate from a hopper to a mixing area over a shorter distance, leveraging the system's lower energy consumption and simplicity.
Another example is in the food processing industry, where manganese silicate is used as a food additive. Here, both positive and negative pressure systems are used, depending on the specific application. Positive pressure systems are employed for transporting the material from storage to processing equipment, ensuring that the material remains sterile and free from contamination. Negative pressure systems are used for short-distance transport within the processing facility, such as moving the material from a mixer to a packaging line. The choice is based on the need for hygiene, energy efficiency, and material handling efficiency.
Ultimately, the choice between positive and negative pressure pneumatic conveying for manganese silicate depends on a careful evaluation of the specific requirements of the application. Positive pressure systems offer superior performance for long-distance, high-volume transport, while negative pressure systems provide a more energy-efficient and flexible solution for shorter distances. By understanding the advantages and limitations of each method, industries can select the most appropriate system to optimize their material handling processes, ensuring efficiency, cost-effectiveness, and product quality.
HeadPowder, with its expertise in material handling solutions, provides tailored pneumatic conveying systems that meet the unique needs of manganese silicate applications. Our team of engineers works closely with clients to design and implement systems that balance performance, cost, and operational requirements. Whether you require a positive or negative pressure system, HeadPowder offers reliable solutions that enhance your material handling capabilities and support your production goals.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top